Every thermoformed part starts as a flat sheet clamped around a tool, and the shape of that tool decides far more than the outline. In heavy-gauge vacuum forming, the choice between a male and a female mold determines which surface ends up cosmetic, which dimensions the tool actually controls, where the wall thins, and what the tooling costs. Buyers who settle this question late tend to redesign parts after first articles; buyers who settle it early quote faster and accept parts with fewer surprises.
This guide explains how each mold style works, where each one thins the sheet, what the trade-offs mean for housings, trays, and covers, and how engineers and buyers can decide between the two before committing to aluminum.
- A male mold is a raised plug the sheet drapes over; a female mold is a recessed cavity the sheet is drawn into.
- The mold-contact surface stays close to the original sheet thickness; free, unsupported surfaces stretch and thin.
- Male tooling controls inside dimensions and suits deep draws; female tooling controls outside dimensions and delivers crisp cosmetic detail.
- Thinning concentrates at the base corners of deep draws on either style; plug assist redistributes material in female cavities.
- Tooling cost follows geometry, texture, and finish requirements, not just the male-versus-female label.
- Judge both options with thickness maps at fixed points rather than a single nominal thickness callout.
What Is a Male Mold in Vacuum Forming?
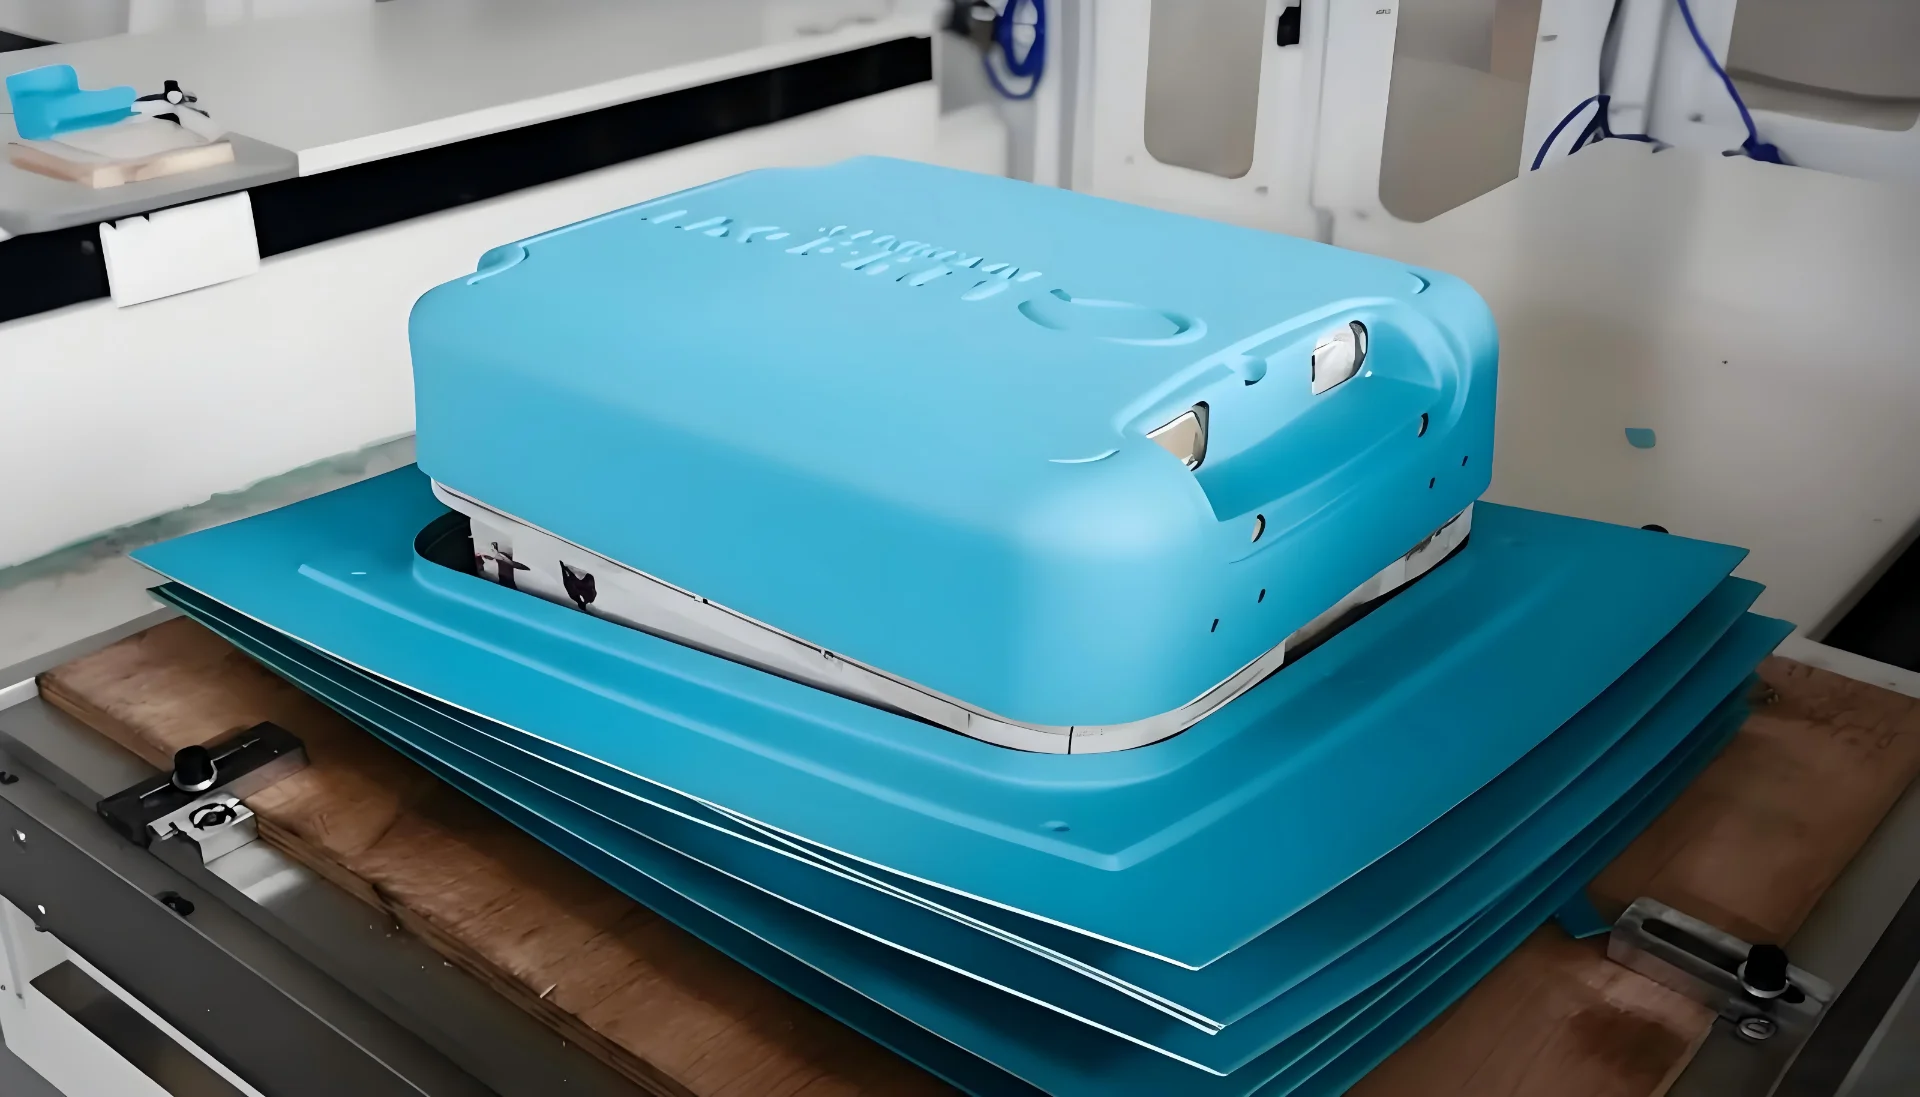
A male mold is a convex, plug-shaped tool that the heated sheet is draped over from above. The tool surface becomes the inside face of the part, and the tool itself defines the part’s inside dimensions.
The forming sequence is simple, but the physics matter. The sheet is heated until it sags, then the tool rises into it or the sheet is lowered over the tool. Because the crown of the plug touches the hot sheet first, that area cools early and keeps close to its original thickness. As vacuum pulls the sheet down the sides, the remaining hot material stretches, so the sidewalls and base corners end up thinner than the crown. On deep draws, that corner thinning is the number to watch, and webbing between tall features is the defect to look for in first articles1.
Draft on a male tool must open outward from the crown toward the rim, or the part will grip the tool on withdrawal. Inside radii should be generous, because sharp corners on the tool become stress concentrations and thin spots on the part. Texture on a male mold appears on the interior face, which is useful when the inside of a cover faces the operator.
Typical male-mold parts include seedling trays where cell geometry is defined from the inside, equipment covers sized to slip over a machine frame, and industrial liners where the cavity they must fit is the critical dimension.
"Male molds always produce more uniform wall thickness than female molds."False
A male crown does hold near-full thickness, but the sidewalls and base corners of a deep draw can thin severely while the crown stays thick. Uniformity depends on pre-stretch, sheet temperature, and draw depth, not on the mold label alone.
"Mold-contact surfaces stay close to the original sheet thickness."True
Wherever the hot sheet touches the tool early, it cools almost immediately and keeps most of its thickness. Free surfaces stretch under vacuum and thin out. That is why designers put cosmetic or dimensionally critical faces against the tool instead of leaving them free.
These thickness rules also shape quoting. A buyer who specifies a single minimum wall across the whole part forces the process to start from thicker sheet, which raises material cost and cycle time. A buyer who specifies minimums per zone — crown, wall, corner — gets a lighter part at a fairer price.
ZetarVac processes thermoforming sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm. Within that envelope, shallow cosmetic covers and deep industrial housings can be compared in the same tooling review, so the male-versus-female decision is made against the real part size rather than a catalog assumption.
What Is a Female Mold in Vacuum Forming?
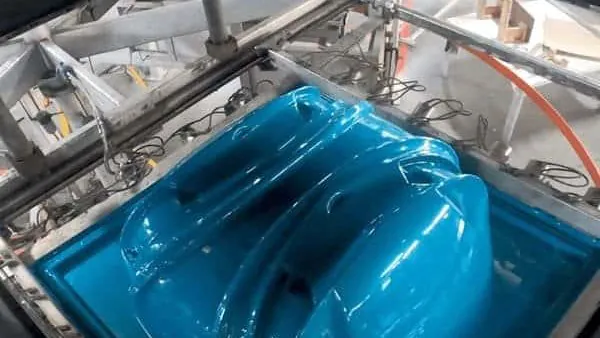
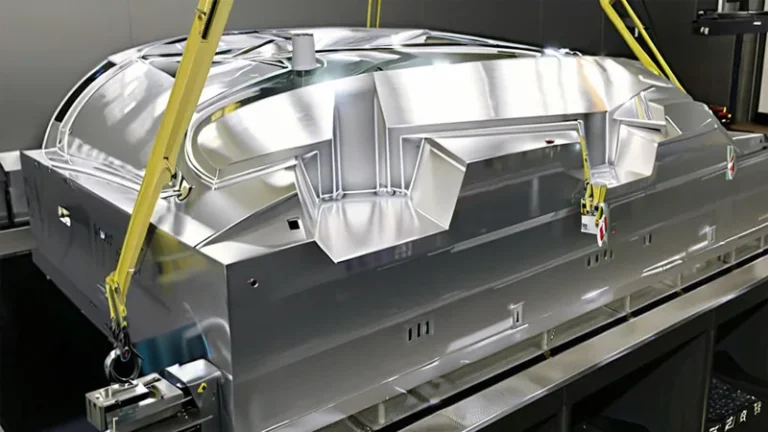
A female mold is a recessed cavity. The heated sheet is clamped over its rim and drawn down inside it, so the tool defines the part’s outside dimensions and the surface touching the tool becomes the finished outer face.
Because the rim contacts the sheet first, the upper walls stay near full thickness while the material that must travel to the cavity floor stretches the most. On anything beyond a shallow part, the floor and lower corners thin noticeably. For deep or highly detailed cavities, a plug assist is added: a helper plug pushes the sheet partway into the cavity before vacuum is applied, carrying extra material toward the bottom before it freezes2. Pressure forming extends the same idea by adding compressed air on the free side of the sheet, forcing it into fine texture and sharp detail on the tool face.
The practical payoff of female tooling is cosmetics. Texture, lettering, and crisp parting lines form on the tool-contact face, which is why exterior surfaces — equipment housings, machine guards, display covers — are usually specified as female-formed. The trade-off is that outside dimensions are now the controlled ones, so any feature that must mate internally needs clearance built into the cavity.
"Female molds are always the more expensive option."False
A cavity removes more material than a plug of the same part, and engraved texture adds cost. But shallow parts need only a small cavity, and avoiding a later coating or laminating operation can flip the total-cost comparison in favor of female tooling.
"Tooling cost follows geometry and finish, not the male or female label."True
Deep, textured, or tight-radiused cavities cost more; simple open plugs cost less. The reliable comparison quotes both styles on the actual 3D model, including trim fixtures and expected cycle time, before any commitment is made.
How Does Each Mold Shape Wall Thickness?
Thickness follows contact timing. Wherever the hot sheet touches the tool early, it freezes near its original gauge3; wherever it stretches unsupported, it thins. Male tools protect their crowns while their base corners thin, and female tools protect their rims while their floors thin.
For planning purposes, deep-draw thermoformed parts commonly show 30–60 percent thinning at the highest-stretch corners, driven by material, sheet temperature, draw ratio, and pre-stretch method. Shallow parts may thin by well under 20 percent. These are engineering ranges rather than guarantees; the honest number for a specific part comes from a trial shot and a thickness map. Pre-stretch practice is documented in depth by the SPE Thermoforming Division, whose technical resources cover material distribution for both mold styles.
The standard method is to mark fixed measurement points on the first article — crown, sidewall mid-height, base corner, flange — and record the thickness at each. Those points then become the acceptance criteria for production. Mechanical properties are validated separately: ASTM D638 is the standard tensile test run on thermoformed sheet and formed parts, and it confirms that the formed material still meets the strength values on the material data sheet.
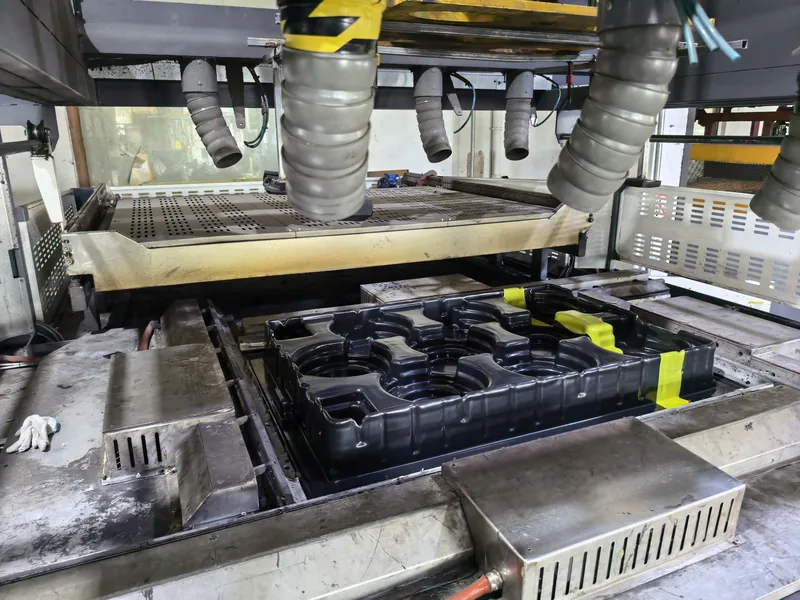
Webbing deserves its own warning. When a tool has two tall, closely spaced features, the sheet bridges between them, collapses, and folds into webs that are both cosmetic and structural defects. Male molds with multiple raised bosses and female molds with deep, narrow pockets are both exposed. The fixes are similar on either style: open up the spacing, increase radii, slow the vacuum, or add pre-stretch.
Male vs. Female Tooling: Side-by-Side Comparison
The table below condenses the decision factors into one view. Use it as a checklist during design reviews, not as a scoring system.
| Aspect | Male mold (plug) | Female mold (cavity) |
|---|---|---|
| Tool geometry | Convex raised form | Recessed cavity |
| Controlled dimensions | Inside of the part | Outside of the part |
| Cosmetic face | Free outer surface | Tool-contact outer surface |
| Near-full-thickness zone | Tool crown (part top) | Rim and upper walls |
| Highest-thinning zone | Base corners on deep draws | Floor and lower corners |
| Draft direction | Opens from crown to rim | Opens from floor to rim |
| Deep draws | Often preferred; crown keeps gauge | Needs plug assist for depth |
| Fine exterior detail | Limited | Strong, especially with pressure forming |
| Typical tooling cost | Often lower for simple plugs | Often higher with texture and detail |
One caution on the last row: cost comparisons that ignore the trimming fixture, texture depth, and expected scrap rate mislead more often than they inform. A cheaper mold that drives a double-digit reject rate is not cheaper.
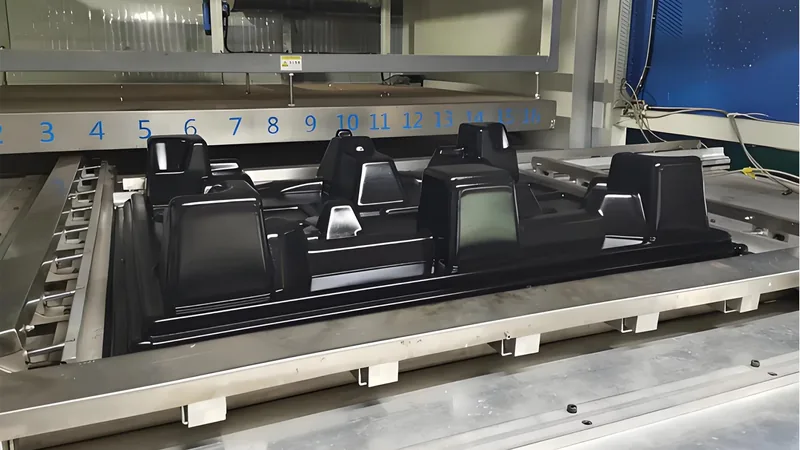
ZetarVac runs more than 20 vacuum forming machines and supports prototyping, small batch, and large batch production on the same plant floor. That matters here because the male-versus-female decision does not have to be final at quotation — both styles can be trialed at prototype scale before volume tooling is committed.
How Should You Choose Between a Male and a Female Mold?
Start from three questions: which face must look finished, which dimensions are critical, and how deep is the draw. A cosmetic exterior with controlled outside dimensions points to a female mold; a deep draw with critical inside dimensions points to a male mold.
Then work through the material and application requirements, because they constrain both styles. ISO 75-2 specifies how the heat deflection temperature4 of a plastic is measured under flexural load, and it is the usual reference for judging whether a formed housing will hold its shape near motors or heaters. UL 94 classifies the flammability of plastic materials, and many formed equipment enclosures must meet a specified rating before they are accepted into electrical assemblies. For transparent covers, ISO 13468 defines the total luminous transmittance of transparent plastics — the property to verify when a PC or PMMA cover must stay optically clear.
The working examples show how the logic plays out. An ABS vacuum-formed seedling tray is defined by its cell geometry from the inside, which favors male tooling. A PC vacuum-formed medical equipment housing with large curved surfaces, cut-outs, and mounting holes usually wants its exterior cosmetic, which favors female tooling with a plug assist for depth. A PMMA display cover lives or dies on exterior clarity and curve quality — again female tooling, with texture kept off optical faces. Material selection interacts with all of this, and the ABS versus HIPS comparison covers the most common housing materials in detail.
Draft angle5, corner radii, and shrinkage allowance belong in this decision as well, because the two mold styles apply them on opposite faces of the same part. Deciding them before the tool is cut costs nothing; deciding them after first articles costs a tool revision.
Formed parts at ZetarVac are trimmed on a 5-axis CNC trimming centre, and the trimmed outline follows the forming tool. The datum chosen on the mold therefore carries straight through trimming, which is one more reason to decide whether inside or outside dimensions are critical before the tool is cut.
Whichever style wins, document the reasoning. When the mold choice is recorded alongside the critical dimensions and cosmetic faces, every later decision — trim datum, inspection points, requote — inherits a clear rationale instead of tribal knowledge.
"First-article approval proves wall thickness will hold across the production run."False
A first article is usually formed from sheet at ideal temperature in the middle of its lot. Heater drift, new sheet lots, and ambient changes move the thickness map over a run. Without periodic checks, thin spots appear long after the first article was signed off.
"Production thickness stability needs checks at fixed points on a schedule."True
Agree the measurement points during first-article review, then re-check them at a defined frequency or whenever the sheet lot changes. This turns thickness from a one-time promise into a controlled characteristic, and it costs minutes per shift rather than a redesign.
FAQ
Does mold choice affect part tolerances?
Yes. Tool-contact dimensions follow the aluminum and hold the tightest values; free-formed surfaces move with sheet thickness variation and cooling, so they need wider tolerances. Agreeing which dimensions are tool-contact during quotation prevents most tolerance disputes later.
Can male and female features be combined on one part?
Yes, and it is common. Deep-draw female parts routinely use a plug assist, and pressure forming pairs a female cavity with a pressure plate or helper plug. Hybrid tooling is specified feature by feature, not picked as a single style for the whole part.
Which mold style is cheaper to maintain?
Neither style is inherently cheaper to maintain. Textured female cavities need more careful cleaning, while male plugs are easier to inspect and repair. Maintenance cost tracks texture depth, material abrasiveness, and handling discipline far more than the male-versus-female choice.
Should the cosmetic face always be formed against the tool?
In most heavy-gauge work, yes. Tool-contact surfaces copy the mold finish and stay closer to the original sheet thickness, while free surfaces show more sag marks and thinning. Exceptions exist where inside dimensions and interior appearance dominate the design.
Can we switch from male to female tooling later?
Technically possible, but it is a new mold rather than a modification. Changing styles redefines which dimensions are controlled and moves the cosmetic face to the other side, so finish, tolerances, and mating features all need re-verification. Trialing both styles at prototype scale is usually the cheaper path.
To keep digging into these decisions, explore our vacuum forming process and capabilities, or see how heavy-gauge tooling choices are handled in practice at the supplier level.
-
Webbing: Wrinkles or folds that form when the hot sheet bridges between mold features and collapses under vacuum. ↩
-
Plug assist: A mechanically driven helper plug that pre-stretches the sheet into a female cavity before vacuum is applied. ↩
-
Gauge: The original thickness of the flat plastic sheet before forming. ↩
-
HDT: Heat deflection temperature, the temperature at which a plastic specimen deflects a defined amount under flexural load. ↩
-
Draft angle: The taper built into mold walls so the formed part releases from the tool without scraping or hanging up. ↩