
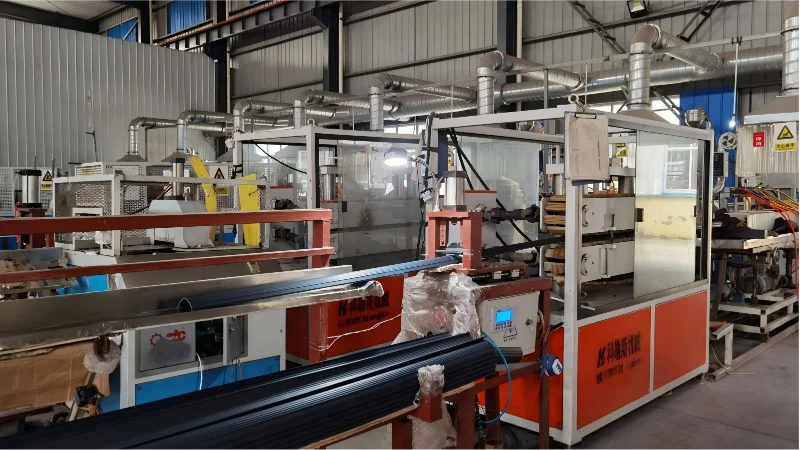
Most buyers meet heavy gauge thermoforming for the first time when a flat plastic sheet becomes a machine cover, a logistics tray, or a medical housing. The process looks simple — heat the sheet, pull it over a mold with vacuum, trim the result — yet the details behind that simplicity decide whether a part is repeatable and affordable or a recurring quality problem. Below are ten facts that engineers and purchasing teams most often learn the hard way, from sheet selection through tooling to field failures. For background on the process itself, the thermoforming overview is a good starting point.
- Heavy gauge thermoforming covers sheet from 0.5 to 15 mm and forming lengths up to about 2,500 mm, which spans most industrial enclosures, trays, and panels in one piece.
- Draw ratio, not machine bed size, is usually the first limit on how deep a part can be formed.
- Standards such as UL 94 and ISO 75-2 decide the material list before formability or price enters the discussion.
- The trimmed edge, produced on a 5-axis CNC trimming centre, defines final fit more than the forming step itself.
- First-article approval does not prove lot-to-lot stability; sheet lots and oven settings still need re-qualification.
- Prototyping, small batches, and monthly volumes of 100,000–200,000 pieces are all realistic in vacuum forming.
What Is Thermoforming, Really?
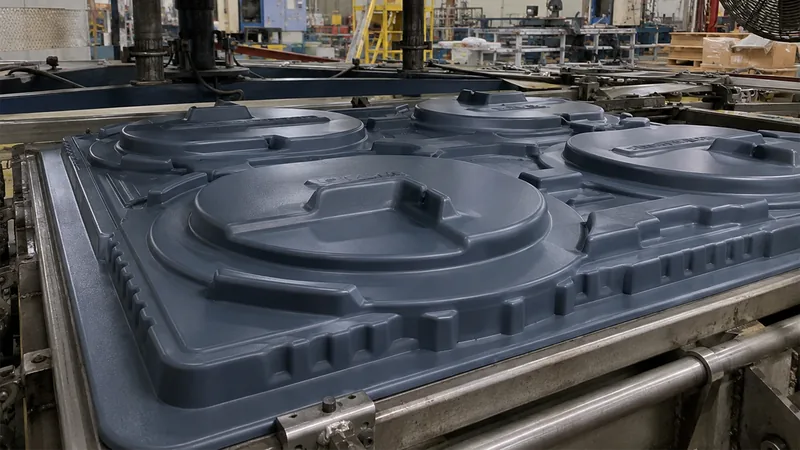
Thermoforming is a process that heats a thermoplastic sheet until it is pliable, stretches it against a mold using vacuum or pressure, and cools it into a stable shape. In vacuum forming the driving force is atmospheric pressure acting on the evacuated gap between sheet and mold — gentle and uniform compared with the packing pressures used in molding processes.
1. Heavy gauge and thin gauge are different businesses. Thin-gauge work runs rolled film on fast rotary lines for high-volume thermoformed packaging. Heavy gauge thermoforming, sometimes called thick-gauge forming, starts from cut sheet 0.5–15 mm thick and produces structural or cosmetic parts such as enclosures, machine covers, trays, and panels. Machines, cycle times, and quality expectations differ enough that a buyer should treat them as separate supplier categories. If your part must carry loads, shield equipment, or survive outdoors, you are in heavy gauge territory — see how a thick gauge thermoforming workflow is structured before you compare quotes.
2. Pressure forming is vacuum forming with a helper. A pressure box above the sheet adds air pressure of roughly 0.3–0.6 MPa on top of the vacuum, pressing the sheet into fine mold texture and sharp detail. It is the standard route when a cosmetic exterior needs texture or crisp edges without secondary finishing.
3. The process window lives in the sheet temperature. Every part is made inside a narrow band between the sheet’s forming temperature and its sag point. Too cold, and the sheet webs and misses detail; too hot, and it sags, marks, or tears. The band shifts with every resin — PVC forms far below PC, and hygroscopic materials must be dried first — so sheet surface temperatures commonly sit somewhere in the 120–190 °C range depending on material and gauge. A molder who cannot describe their heating zones is asking you to trust luck.

Which Sheet and Size Limits Shape Your Design?
Three numbers matter before any geometry discussion: the sheet thickness a molder can process, the maximum forming length of the machines, and the depth your part demands relative to its footprint. A working window of 0.5–15 mm sheet and forming lengths up to about 2,500 mm covers most single-piece enclosures, trays, and cladding panels without joining or welding.
4. Draw ratio decides depth before machine size does. The draw ratio1 is the forming depth divided by the narrowest mold dimension at that depth. As shop practice, ratios near 1:1 form comfortably; above roughly 1.5:1 the process usually needs plug assistance, hotter sheet, and staged vacuum; and near 2:1 corners thin unpredictably. Exact limits depend on resin, gauge, and mold temperature, so treat published values as starting points rather than guarantees.
5. Wall thinning is physics, not a defect. As the sheet stretches into a cavity, the area that touches the mold first stops moving while the rest keeps drawing material past it. On deep draws, corner walls can end up 30–50% thinner than the starting sheet; on shallow trays the loss is often under 15%. Specify a minimum wall at the thinnest section — not the nominal gauge — and ask the molder to section a sample part and map the distribution before the design is frozen.
ZetarVac processes sheet from 0.5 to 15 mm and forms parts up to about 2,500 mm long on more than 20 vacuum forming machines, which means large equipment housings and long panels can usually be formed as one piece instead of being split and joined.
How Do Standards Decide Whether a Formed Part Passes?
Standards turn datasheet claims into acceptance criteria a buyer can enforce. For an enclosure, the first two questions are usually whether the plastic will burn and how long it carries load at temperature, which is why flammability and heat-deflection data appear in nearly every housing specification.
6. Standards decide the material list before formability does. Formability tells you whether a resin can be shaped; standards tell you whether the shaped part can ship. Three test families matter most for formed parts.
Flammability. UL 94 classifies the flammability of plastic materials, and many equipment enclosures and covers are specified to a UL 94 rating such as V-0 or V-2 before tooling starts.2 One warning: the rating applies at a specific thickness, and a formed corner is thinner than the nominal sheet, so certification must be confirmed at the thinnest product wall.
Heat deflection. ISO 75-2 specifies the method for determining the temperature at which a plastic deflects a set distance under flexural load, and that value — the heat deflection temperature3 — is what predicts whether a housing near a motor or control cabinet will sag over months of service. The melting point on a datasheet will not tell you that.
Mechanical validation. ASTM D638 defines the tensile test used to validate both incoming sheet and formed parts, because stretching during forming changes orientation and, with it, strength and elongation relative to the flat sheet the resin vendor certified.4 For load-bearing parts, tensile coupons cut from actual formed areas are worth the small extra cost.
"Any engineering plastic can be swapped into an enclosure design if it forms cleanly."False
Formability and compliance are separate gates. A resin can drape beautifully over the mold and still miss the flammability, heat-deflection, or impact requirement the enclosure demands, which is why material substitution needs a compliance check before a quote, not after a failed audit.
"Material selection starts from the enclosure requirement, not the forming behavior."True
Experienced teams filter resins by UL 94 rating, heat deflection temperature, and impact class first, then choose among the survivors for formability and cost. That order prevents a late discovery that the chosen sheet cannot be certified at the finished wall thickness.
The table below maps common formed materials to the property a reviewer will check first:
| Material | Typical formed use | Property to verify first |
|---|---|---|
| ABS | Equipment housings, cases, guards | UL 94 rating and impact at part thickness |
| PC | Clear guards, protection covers, medical housings | Impact strength and heat deflection temperature |
| PC/ABS | Automotive interiors, equipment housings | Balanced impact, flammability, and low-temperature behavior |
| ASA | Outdoor equipment housings, automotive exterior parts | UV and weathering stability |
| HDPE | Industrial trays, equipment liners, storage boxes | Stiffness at temperature and stress-crack resistance |
| PP/GF | Automotive and industrial structural parts | Flexural stiffness and warpage control |
| PMMA | Clear covers, luminaires, display parts | Light transmittance and surface hardness |
| TPE | Soft liners and seals | Hardness and compression set |
What Happens Between the Sheet and the Shipped Part?
Forming is the visible half of the process. Tooling and trimming quietly decide cost, tolerance, and lead time, and they are where most disputes between buyers and suppliers start.
7. Tooling is cheaper than you expect — and more sensitive. A thermoform mold works at far lower pressures than a molding die, so it can be cast, machined, or additively built at a fraction of the cost, which is why prototyping stays affordable. The trade-off is sensitivity: mold temperature, vent layout, and vacuum path all shape the sheet, and a mold that runs hot on one side will pull the part out of flat. Ask how mold temperature is controlled and logged; that answer predicts your dimensional consistency better than machine size does.
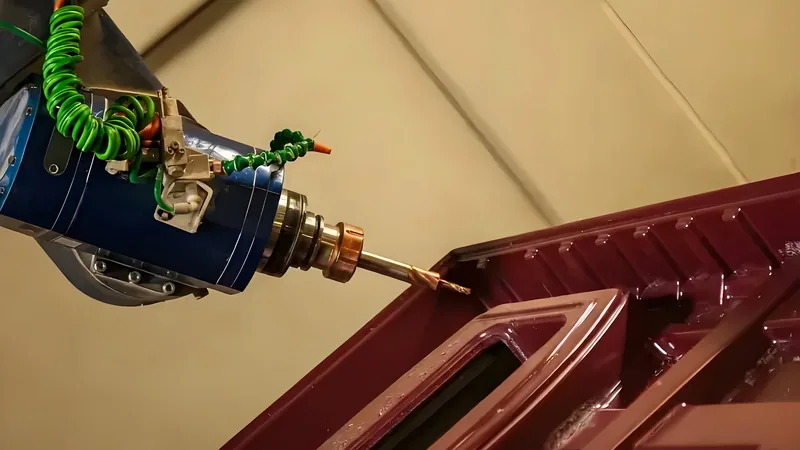
8. The trimmed edge is where quality is judged. After forming, the part carries flange material that must be removed along a three-dimensional contour. A 5-axis CNC trimming centre follows the forming tool geometry, so the cut line lands exactly where the formed surface expects it; hand trimming cannot hold that relationship on deep or curved parts.5 Mounting holes, cut-outs, and snap features are also produced at trimming, so trim programming is part of dimensional quality, not a finishing afterthought.
ZetarVac trims formed parts on a 5-axis CNC trimming centre where the trimmed outline follows the forming tool, so mounting holes and cut-outs land consistently on curved surfaces across a production run.
9. Tolerances scale with part size. As common heavy-gauge practice, small formed features hold roughly ±0.5 mm, overall formed dimensions on large parts open up into a wider envelope that scales with part size and geometry, and trimmed hole patterns hold tighter because they are cut in a fixture. Write tight tolerance only on the dimensions that drive assembly and leave free surfaces looser; blanket tolerances raise trimming cost without improving fit.
Which Defects Only Appear After the Part Is Formed?
10. Some failure modes are invisible until the sheet meets the mold. Webbing, blisters, and warpage rarely show up in a datasheet review — they emerge from the interaction of geometry, moisture, and cooling, and each has a specific inspection method.
Webbing and bridging appear between tall bosses or across wide spans when the sheet contacts high points first and the surplus material folds instead of stretching. The fix is usually geometric — increase spacing, add radii, or re-sequence the vacuum — rather than a better operator.
Blisters and bubbles come from residual moisture in the sheet. Hygroscopic materials such as ABS, PC, and PA6 need drying before forming, so a blister on a cosmetic surface is a drying-log problem before it is a forming problem.
Warpage grows with asymmetric wall distribution and uneven mold cooling. Parts that leave the machine flat and warp days later were cooled under residual stress; section the part, measure the wall map, and rebalance cooling rather than fighting the symptom during assembly.
"A first article that passes inspection proves the whole order will match it."False
A first article is formed from one sheet lot, one oven state, and one mold temperature. Sheet lots change, heaters drift, and mold temperature creeps across shifts, so a batch can move out of tolerance days after approval — usually at corners first, where the wall is thinnest.
"Production stability is confirmed across sheet lots and shifts, not on a single part."True
Reliable suppliers re-qualify after every material lot change and track oven zones and mold temperature through the run. Ask how incoming sheet is certified and what triggers re-approval; the answer separates stable heavy gauge thermoforming shops from lucky ones.
For deeper guidance on sheet drying and heating practice, the SPE Thermoforming Division publishes technical papers that go well beyond what any single molder can share in a quote.
ZetarVac runs 45+ production lines with a reference monthly capacity of about 100,000–200,000 pieces and supports prototyping, small batch, and large batch production, so a design validated on one equipment class can scale without changing process route.
FAQ
How thick can thermoformed sheet be?
Heavy gauge vacuum forming typically processes sheet from about 0.5 to 15 mm. Below roughly 1.5 mm you are in thin-gauge packaging territory; above 15 mm, controlling wall distribution on deep draws becomes difficult and other forming routes deserve consideration.
Is vacuum forming suitable for very large parts?
Yes. With forming lengths up to about 2,500 mm, machine enclosures, vehicle and bus panels, and large tray systems can be formed in one piece. The practical limit is usually draw ratio and corner thinning, not machine bed size.
What tolerances can a formed part hold?
Small formed features commonly hold around ±0.5 mm, overall formed dimensions on large parts open into a wider envelope that scales with part size, and trimmed hole patterns hold tighter because they are cut in a fixture. Specify tolerances on assembly-critical dimensions only.
Which materials are used for thermoformed enclosures?
ABS, PC, PC/ABS, and ASA dominate equipment housings: ABS for cost and formability, PC for impact and clarity, PC/ABS for balanced performance, and ASA for outdoor UV stability. HDPE and PP serve industrial trays and liners where chemical resistance matters more than stiffness.
Does thermoforming make sense for low volumes?
Yes. Tooling cost is a fraction of a molding die, so prototypes and small batches stay economical, and the same part can scale to monthly volumes in the 100,000–200,000 piece range without changing process route.
To keep digging into the process, explore the ZetarVac vacuum forming overview for material options, tooling practice, and worked examples, or see how a China-based heavy gauge thermoforming partner walks a project from prototype to volume production.
-
Draw ratio: Draw ratio is the forming depth divided by the narrowest mold dimension at that depth, used to estimate how severely the sheet will thin during forming. ↩
-
UL 94: UL 94 is the standard classification for the flammability of plastic materials, graded at defined specimen thicknesses. ↩
-
HDT: HDT, heat deflection temperature, is the temperature at which a plastic specimen deflects a specified amount under a standard flexural load. ↩
-
ASTM D638: ASTM D638 is the standard tensile test method for plastics, measuring strength, modulus, and elongation of sheet and formed parts. ↩
-
5-axis CNC trimming: 5-axis CNC trimming machines formed parts with a cutting head moving along five axes to follow three-dimensional trim contours. ↩


