Thermoformed packaging shows up everywhere once you start looking: machine-side trays that carry parts between work cells, protective covers that ship with expensive equipment, reusable material-handling trays that survive years of automation, and retail displays that must look sharp after a rough freight trip. Most buyers meet this process when a part is too large, too thick-walled, or too long-lived for ordinary packaging routes. This guide explains how the process works, how materials are selected, which defects actually matter, and what to check before you commit to a tool.
- Thermoforming packaging spans thin-gauge clamshells and heavy gauge trays and covers formed from sheet up to 15 mm thick.
- The wall thickness a part ends up with after forming, not the sheet gauge you ordered, decides its stiffness and impact behavior.
- HDPE, ABS, PVC, PP, and PC cover most packaging duties; the right pick balances impact strength, temperature exposure, clarity, and cost.
- Trimmed outline accuracy comes from 5-axis CNC trimming of the formed part, not from hand finishing at a bench.
- Food-contact formed trays must comply with EU 10/2011, while structural packaging is validated with standard tensile and flexural tests.
- The process supports prototyping, small batch, and large batch production, which is why reusable industrial packaging is so often thermoformed.
What Is Thermoforming Packaging?
Thermoforming packaging is packaging made by heating a plastic sheet until it softens, then drawing it against a mold with vacuum so the sheet takes the tool’s shape. In thin gauge, the same process produces clamshells and blister packs; in heavy gauge, it produces reusable trays, protective covers, and structural packaging parts.
The two groups are quoted and validated differently, so it pays to know which one you are buying. Thin-gauge work is a high-speed, high-volume business measured in single-use units. Heavy gauge thermoforming runs slower on larger machines, uses sheet from 0.5 to 15 mm, and produces parts that stay in service for years — dunnage trays, machine covers, shipping protection for large equipment, and multi-cavity trays for agriculture and logistics. This guide concentrates on the heavy gauge side, because that is where most engineering decisions get made.
How the Heavy-Gauge Process Shapes a Packaging Part
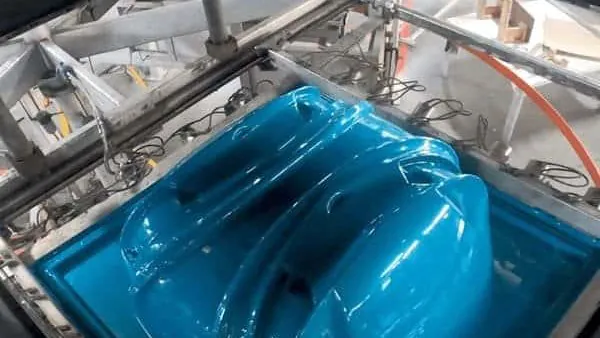
The sequence is simple to describe and easy to get wrong. A clamped plastic sheet is heated until it sags into a controlled bubble, then pulled down over a single-sided mold by vacuum, cooled until it holds its shape, and finally trimmed. The basic mechanics are well documented in CustomPartNet’s thermoforming overview, but production quality depends on details that overview does not cover: heater zoning, sheet temperature uniformity, vacuum hole layout, and mold temperature.
Most packaging polymers form inside a sheet-temperature window of roughly 120–180 °C, with the exact window set by the material data sheet, the sheet gauge, and the machine’s heater zones. Forming too cold gives you poor detail and high residual stress; forming too hot gives you sheet sag, marks off the mold, and unpredictable thinning at the part’s deepest features. In heavy gauge vacuum forming, the process is tuned so the sheet reaches the mold with enough heat to take detail but not so much that it thins out of control.
Two numbers define the usable envelope for formed packaging. Sheet thickness processed runs from 0.5 to 15 mm, and the maximum forming length is about 2,500 mm, which is why long trays and full-length covers can be formed in one piece. Beyond geometry, the practical limit is draw ratio — the relationship between the deepest draw and the opening the sheet must pass through — which a molder will estimate before quoting the tool.1
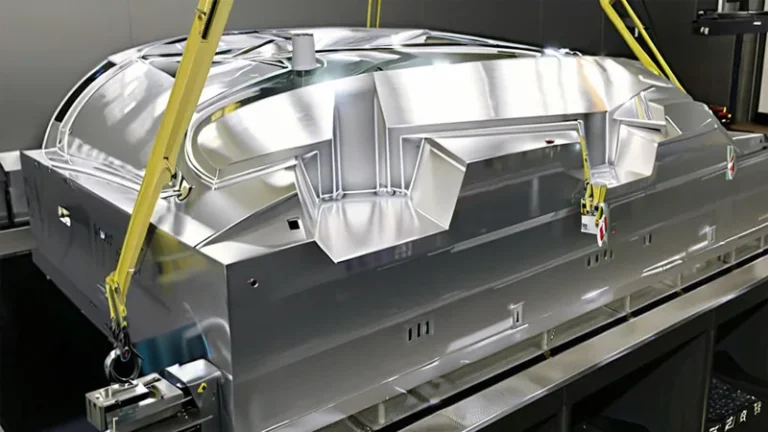
ZetarVac runs more than 20 vacuum forming and thermoforming machines, processing sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm. For a packaging buyer, that means large trays and long covers can be formed in one piece instead of being split into several sections and joined.
Machine capacity is only half the story, though. What separates a stable process from a lucky one is how the molder proves the parts, and the most common misunderstanding starts right after the first sample is approved.
"First-article approval guarantees the whole production run will match the sample."False
First articles are usually formed slowly, with generous heating time and full operator attention. Production cycles run faster and hotter on a schedule, so wall thinning at deep draws can drift even when the tool has not changed.
"Stability is proven by parts sampled after the process reaches production conditions."True
Once the machine is running at rate, sample parts and measure wall thickness at the same deep-draw locations checked on the first article. Repeat that at two or three checkpoints during the run, and you will know whether the process holds instead of hoping it does.
Which Material Fits Your Packaging Duty?
Most heavy gauge packaging parts are formed from HDPE, ABS, PVC, PP, or PC. HDPE suits industrial trays, equipment liners, and storage boxes; ABS and PC/ABS suit protective covers, cases, and guards; PVC works for trays and general packaging where cost leads; PP handles chemical exposure; PC is the choice when clarity and impact strength are both required.
Each material also brings its own forming personality. ABS is forgiving and holds detail well, which is why it dominates protective covers and equipment-style cases. HDPE shrinks and warps more, so flatness on large trays takes real process control. PC forms cleanly but demands careful heating practice, and PMMA is chosen for display work where optical clarity matters more than impact. Temperature exposure is a separate axis entirely: deflection temperature under load sets how much heat a filled tray or a sun-exposed cover can tolerate in service.2
| Material | Typical formed packaging use | Property to verify before release |
|---|---|---|
| HDPE | Industrial trays, equipment liners, storage boxes | Drop resistance and flatness after forming |
| ABS | Equipment housings, cases, guards | Impact strength and surface finish |
| PVC | Trays, packaging, industrial liners | Forming window and detail reproduction |
| PP | Trays, boxes, packaging, equipment liners | Chemical resistance and fatigue behavior |
| PC | Clear guards, equipment protection covers | Transparency and puncture impact |
| PMMA | Clear covers, display and retail parts | Total luminous transmittance |
Material compliance is part of the specification, not an afterthought. For any tray or packaging article that will touch food, EU 10/2011 regulates which plastic compositions may be used and how much material may migrate into foodstuffs, so the compliance file has to be requested at the sourcing stage rather than assembled after tooling.3
Material choice is also where one of the most persistent packaging myths lives.
"A thicker starting sheet always makes the finished tray stronger."False
Forming stretches the sheet unevenly, so corners and deep draws can end up thinner than on a lighter sheet formed with a better draw ratio. Extra gauge also slows heating and cooling, adding cost without buying performance where the part actually needs it.
"Measured wall thickness at critical features is the number to specify."True
Ask the molder to report wall thickness at corners, flanges, and load points on formed parts, not the incoming sheet gauge. Those measurements decide whether the tray survives the drops and stacking loads you actually care about.
Thin Gauge or Heavy Gauge: Which Does Your Part Need?
Choose thin gauge when the packaging is disposable and consumed with the product; choose heavy gauge when the tray or cover is reused, carries load, or protects equipment. The practical crossover sits where sheet exceeds roughly 1.5 mm and parts are measured in years of service rather than single trips.
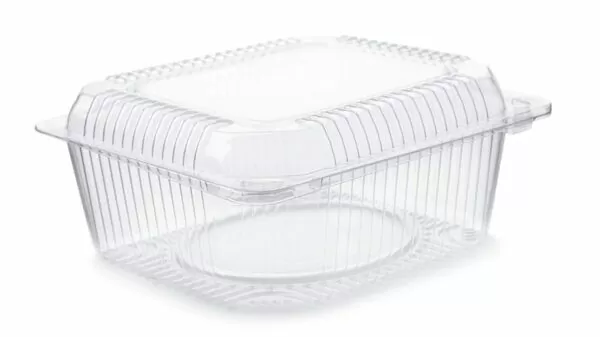
Thin-gauge thermoforming is built around roll-fed sheet, fast cycles, and millions of units, which is the right economics for retail blister and clamshell packaging. Heavy gauge thermoforming works from cut sheet on larger machines, trades cycle time for part depth and stiffness, and justifies itself whenever a tray will make hundreds of trips through a factory or a cover must protect equipment for the life of a product line.
Tooling reflects the same split: thin-gauge tools are built for speed and volume, while heavy gauge tools are optimized for geometry and easy revision. If your part sits on the heavy side of that line, it is worth reading a dedicated thick-gauge thermoforming breakdown before you set tolerances.
What Defects and Checks Decide Packaging Part Quality?
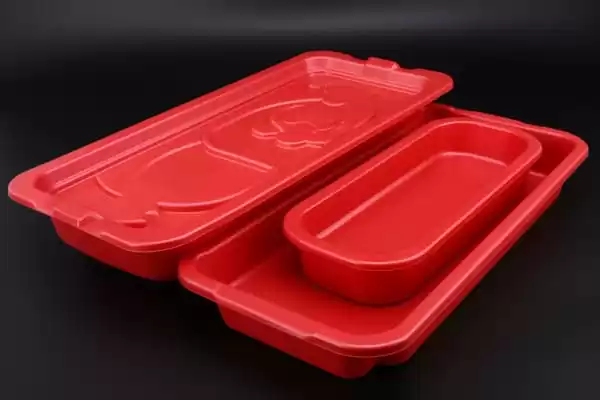
The failures that matter are uneven wall thinning, webbing between deep features, warpage after trimming, and stress whitening at corners. All four are visible in sampled production parts, which makes systematic sampling a stronger acceptance tool than any inspection of the first piece alone.
Wall thickness distribution is the first check. Ultrasonic gauges measure the formed part at corners, sidewalls, and flanges in minutes, and a thickness map tells you more about process health than any visual inspection. Webbing — material folding between tall or closely spaced features — appears when the hot sheet bridges and then collapses, and it is fixed by changing plug geometry, vacuum hole layout, or sheet temperature rather than by reworking parts.4
Warpage is the second battle. Large flat trays and covers relax toward their preformed shape as they cool, so flatness has to be controlled through cooling practice, mold temperature, and fixturing during trimming. Mechanical performance is then validated against standard methods: ISO 527-2 defines the tensile test used on thermoformed sheet, which lets you compare sheet and formed-part tensile data from different suppliers on the same basis, while ASTM D790 governs flexural property measurement for formed panels and enclosures where stiffness under load is the acceptance criterion.
Trimming is the step buyers most often underestimate, and one claim about it causes real damage.
"Formed packaging parts come off the mold ready to ship."False
As-formed parts carry the full sheet perimeter, sag edges, and clamp margins, so the final outline does not exist until it is cut. Without controlled machining, cut-outs and mounting holes drift from tray to tray and stacking features stop lining up.
"Trimmed outline accuracy is set by CNC cutting of the formed part."True
A capable molder trims on a 5-axis CNC trimming centre, where the trimmed outline follows the forming tool geometry. That is how cut-outs, mounting holes, and stacking rims stay consistent across a production run, and it is a fair question to ask any supplier early.
Tooling and volume planning deserve the same scrutiny as the forming itself. Mold material, texture depth, and draft angles decide both part cost and how often the tool needs attention, and the practical tips of thermoforming cover many of these choices in detail. On the volume side, thermoforming sits in a useful band: tooling stays affordable for mid-volume programs, and the process supports prototyping, small batch, and large batch production from the same design intent.
ZetarVac’s reference monthly capacity is about 100,000 to 200,000 pieces across more than 45 production lines in total at the plant. For a packaging program, that means a design can move from prototyping to small batch to large batch without changing suppliers or restarting tooling conversations.
FAQ
Is vacuum forming the same as thermoforming?
Vacuum forming is the most widely used variant of thermoforming: the heated sheet is drawn against the mold by vacuum alone. Thermoforming is the broader family, which also includes pressure forming, where air pressure pushes the sheet into the tool for sharper detail.
How thick and how large can formed packaging parts be?
In heavy gauge work, sheet from 0.5 to 15 mm can be processed with a maximum forming length of about 2,500 mm. That envelope covers most industrial trays, long equipment covers, and multi-cavity agricultural trays in one formed piece.
Does thermoforming only work for simple, shallow shapes?
No. Deep draws, custom cavity counts, curved geometries, and integrated cut-outs are routine once the tool is designed for them. An ABS vacuum-formed seedling tray, for example, carries multiple cavities with custom cell geometry sized to the crop, and PC medical equipment housings are formed as large curved shells with custom cut-outs and mounting holes.
What documentation should I ask a thermoforming supplier for?
Ask for three things: measured wall thickness at critical features, material compliance files matched to the duty — EU 10/2011 documentation when trays touch food, transmittance data for clear PMMA parts — and sampling records taken at production conditions. Those documents predict production behavior far better than a polished showroom sample.
How do I keep researching before I compare suppliers?
Walk through ZetarVac’s vacuum forming guide to see how forming capability, tooling, and trimming fit together, then hold what you read against your own part drawings and duty cycle. When you are ready to look at suppliers, the China vacuum forming manufacturer page gives you a structured view of what a heavy gauge molder should be able to show you.
-
Draw ratio: The ratio between the depth or area a sheet is stretched over and its starting dimensions; higher draw ratios thin the sheet more at deep features. ↩
-
HDT: Heat deflection temperature, the temperature at which a plastic test bar deflects a set amount under a defined flexural load, used to judge short-term heat resistance. ↩
-
EU 10/2011: The EU regulation on plastic materials and articles intended to come into contact with food, defining authorized compositions and migration limits. ↩
-
Webbing: A thermoforming defect where the hot sheet folds or wrinkles between tall or closely spaced mold features instead of stretching cleanly. ↩