
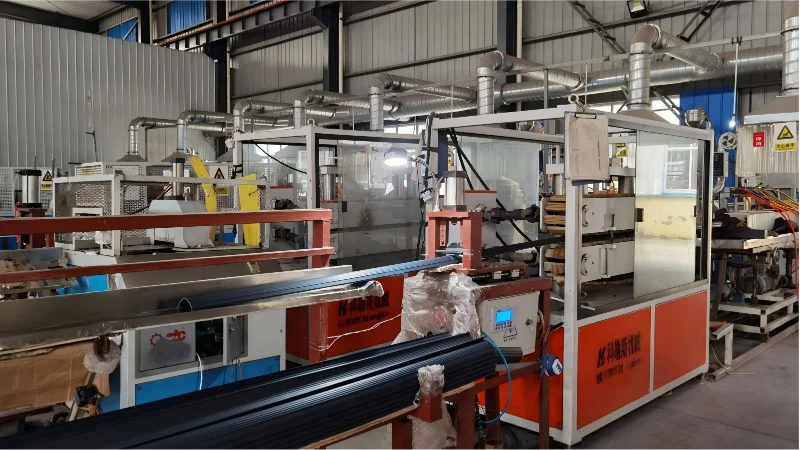
When a program engineer needs a plastic enclosure, cover, tray or guard, two routes usually sit on the table: injection molding and heavy-gauge thermoforming. The honest engineering answer is that thermoforming can replace molding for a broad class of parts, but only when part size, wall section, annual volume and standards requirements line up in its favor. This article sets out where the substitution works, where it breaks, and how to validate it before you commit tooling budget.
- Heavy-gauge thermoforming is a practical substitute for injection molding on large, thin-walled parts such as equipment enclosures, machine covers, trays and guards.
- The substitution works best from prototypes through mid volumes; above roughly 25,000–50,000 annual pieces, molded amortization can flip the cost math.
- Formed walls thin wherever the sheet stretches hardest — budget 20–50% thinning on deep draws instead of expecting uniform cross-sections.
- Formed enclosures can satisfy UL 94, IEC 60529 and NEMA 250 requirements when resin grade and sealing design are engineered in from the start.
- Validate the part the same way as any plastics program: tensile per ASTM D638, flexure per ASTM D790, heat deflection per ASTM D648.
When Can Thermoforming Replace Injection Molding?
Yes for large, thin-walled parts — equipment enclosures, machine covers, industrial trays and protective guards — where moderate annual volumes make molded tooling uneconomic. No when the design demands thick uniform cross-sections, complex internal cores, or volumes high enough for molded amortization to drop below forming’s per-part cost.
Heavy-gauge thermoforming works from cut sheet rather than resin pellets. The sheet is clamped, heated into its forming window, then drawn down over a single-sided tool by vacuum forming or, on tighter-detail parts, by pressure forming with plug assist. The formed shell is trimmed on a 5-axis router and moves to secondary operations such as drilling, bonding and hardware insertion.
The substitution is strongest at the two ends of the size spectrum that molded tooling dislikes: very large parts, where a two-sided steel tool gets expensive and machine tonnage climbs, and low-to-mid volume programs, where the molded tool never repays itself. A formed enclosure two meters long is routine work for heavy-gauge shops; a molded one is a capital project.
Material selection follows the same logic as any plastics program. ABS covers general housings and guards, PC serves clear guards and equipment covers, ASA handles outdoor exposure, and PP or HDPE suit industrial trays and liners. A fuller side-by-side of the two processes is set out in our thermoforming and injection molding overview, and the compatible resin families are mapped in this guide to plastic vacuum forming materials.

What Happens to Wall Thickness and Geometry?
Injection molding fills a closed cavity, so wall thickness is fixed by the mold and stays nearly uniform. Vacuum forming stretches a heated sheet over a single-sided tool, so the finished wall thins wherever the sheet has to stretch hardest — deep corners, tall flanks and tight radii.
Engineers describe this behavior with the draw ratio, the ratio of formed surface area to the original clamped sheet area.1 As the ratio climbs, corner thinning compounds; on aggressive deep draws a corner can carry only half to three-quarters of the nominal sheet gauge. Sound practice budgets for this deliberately: specify the minimum acceptable wall in the corner, not the nominal gauge on the flat.
Geometry rules follow from the physics. Generous corner radii keep the sheet from bridging, a few degrees of draft on male tools eases release, and ribs or bosses are formed as flange features rather than internal cores because the tool only contacts one face. Cosmetic detail lives on the tool side, while the free side carries the fine texture of the heated sheet.
ZetarVac processes sheet from 0.5 to 15 mm on more than 20 vacuum forming and thermoforming machines, with a maximum forming length of about 2,500 mm and 5-axis CNC trimming that follows the forming tool. That envelope covers everything from thin equipment covers to full machine enclosures in one formed shell.

Because the trimmed outline follows the forming tool, the 5-axis trimming centre keeps flange datums consistent from part to part. That matters when the enclosure bolts to a machined frame: mounting holes and cut-outs land where the mating structure expects them, without a secondary fixturing operation.
How Do Tooling Cost and Volume Break Even?
Forming tooling typically costs a fraction of a molded tool because it is single-sided and is often machined from aluminum or composite board. The trade is a higher per-part cost, so break-even usually lands somewhere between ten thousand and fifty thousand annual pieces, depending strongly on part size and material.
The crossover point is not a published constant. A small electronics tray and a two-meter machine cover have completely different tooling, cycle and finishing economics, so their break-even volumes differ by an order of magnitude. The defensible method is to model the whole program — tool cost, cycle time, sheet yield, trimming, finishing and freight — and compare annualized totals at your actual volume.

"Thermoforming tooling is always the cheaper choice because the molds are simple."False
A single-sided tool does cost a fraction of a molded tool, but cycle time and material yield run less favorably. At sustained high volume the molded amortization curve crosses below, so total program cost — not tool price alone — decides the winner.
"Break-even volume depends on part size, not a universal rule of thumb."True
A pocket-sized tray and a two-meter enclosure differ by orders of magnitude in tooling and cycle economics, so their crossover points do too. Model the full program at your real volumes before committing to either route.
Which Properties and Standards Should You Validate?
Run the same validation you would demand of any structural plastics part: tensile properties on the sheet and the formed part, flexural stiffness on panels, heat deflection under load, and — for electrical equipment — flammability and ingress protection on the finished enclosure.
ASTM D638 and ISO 527-2 define the tensile test used to qualify both incoming sheet and finished formed parts, so material certificates and part tests can be compared on the same basis. ASTM D790 governs flexural properties, the stiffness metric that decides whether a formed panel stands up as an enclosure wall or sags between its mounting points. For thermal exposure, ASTM D648 and ISO 75-2 measure the deflection temperature of the material under flexural load.2
For electrical equipment, UL 94 classifies the flammability of plastic materials and is required for many equipment enclosures, while IEC 60529 defines the ingress protection code that a formed cover can only claim once gaskets, lapped joints and drainage are engineered in.34 NEMA 250 adds the Type 4 and 4X enclosure constructions often specified on industrial control panels. Each of these applies to the finished assembly, not just the resin grade.
Process-level context on sheet behavior and forming defects is documented in depth by the SPE Thermoforming Division, whose technical resources are a useful reference when reviewing a supplier’s test plans.
One recurring mistake in substitution projects is assuming the certification path resets because the process changed. It does not.
"A formed plastic enclosure cannot meet real electrical enclosure standards."False
A formed housing is judged against the same UL 94 and IEC 60529 requirements as a molded one; the process does not exempt the part. Assuming otherwise is how formed covers fail customer audits.
"Standards compliance is engineered through resin grade and sealing design."True
Selecting a flame-rated ABS or PC grade, adding gasket grooves and lapped flanges, and testing the finished housing are what earn a rating. Heavy-gauge forming is fully compatible with these requirements when they are specified before tooling.
Where the resin family matters most is outdoor and transparent service, because UV stability and clarity are resin properties rather than process properties.
ZetarVac’s forming material library spans ABS for housings and guards, PC for clear covers, ASA for outdoor equipment, PP and HDPE for industrial trays and liners, PMMA for display parts, and PC/ABS for automotive interiors. A substitution project can usually keep the resin inside the family the molded design already used.
Where Does Forming Fail in Service?
Heat is the first limit. A formed enclosure is a single-wall shell, and its working temperature ceiling is set by the resin’s softening behavior rather than by structural margin. The Vicat softening temperature per ISO 306 indicates where a formed part starts to sag under load, so it is the practical screening number for any cover sitting near a heat source.5
Thinning hot spots are the second failure mode. Corners that were under-gauged at forming become crack initiation sites under vibration or impact; a housing that survives shipment but cracks after two years on a vibrating frame almost always fails at the thinnest formed radius. Ultrasonic thickness mapping, or sectioning a first-off part, finds these hot spots before release.
Warping is the third. Asymmetric cooling or uneven sheet heating locks residual stress into the shell, and the part moves after trimming. Symmetric tool temperature control and adequate cooling on the tool keep it in check, and flattening fixtures buy back tolerance on borderline designs.
A Selection Framework for Program Engineers
When the decision has to be documented for a design review, a factor-by-factor comparison keeps the discussion out of opinion territory:
| Decision factor | Favors heavy-gauge thermoforming | Favors injection molding |
|---|---|---|
| Part footprint | Large shells up to about 2,500 mm forming length | Small to medium parts per shot |
| Annual volume | Prototypes through mid volumes | High continuous volumes |
| Wall section | Single-wall shell, 0.5–15 mm sheet | Uniform multi-millimeter sections |
| Tooling budget | Single-sided, low-cost tool | Two-sided steel tool |
| Surface detail | Tool side defined; pressure forming adds detail | Detail on both faces |
| Typical parts | Enclosures, covers, trays, guards | Complex small structural parts |
ZetarVac runs more than 45 production lines across the plant, with reference monthly capacity around 100,000–200,000 pieces across prototyping, small batch and large batch programs. Documented heavy-gauge forming cases include an ABS multi-cavity seedling tray, a PC medical equipment housing with custom cut-outs and reinforcement, and a high-clarity PMMA display cover.
One judgment trap deserves its own call-out: how much a single good part actually proves.
"A good first article proves the process is stable for production."False
First-article approval validates tool fit and setup on one sample. Sheet batch variation and oven drift appear across runs, not within a single part, so a clean first article says nothing about part two hundred.
"Process stability has to be demonstrated before release."True
A short capability run measuring critical dimensions and minimum wall across consecutive parts catches thinning hot spots and drift early. Treat first-article sign-off as the gate into that run, not as the finish line.
FAQ
How large can a formed part actually be?
ZetarVac processes sheet from 0.5 to 15 mm and forms parts up to about 2,500 mm in length, trimming them on a 5-axis centre. That covers most industrial equipment enclosures, machine covers and large logistics trays as a single formed shell rather than a welded assembly. The heavy-gauge vacuum forming manufacturer page puts the forming envelope in context.
Can a thermoformed part match the strength of a molded one?
Per resin grade, the material itself is identical; what differs is wall distribution and residual stress. For large panels, a continuous single-wall shell with formed flanges is often stiffer in practice than a comparably thin molded shell of the same resin. Confirm with ASTM D638 tensile and ASTM D790 flexural testing on actual formed parts rather than resin data sheets alone.
What annual volume makes the switch worthwhile?
As a planning range, forming tends to win from prototypes through roughly 25,000–50,000 annual pieces for mid-sized parts, with the crossover moving lower as part size grows. Treat the range as a screen and run the program-level cost model at your actual volumes before committing.
Can formed enclosures carry IP or flame ratings?
Yes. Choose a UL 94 rated resin grade, design gasket grooves and lapped flanges into the part, and test the finished housing against IEC 60529 or NEMA 250 as the specification requires. Industrial formed enclosures are regularly specified this way.
Where can I go deeper on heavy-gauge thermoforming?
Explore the process guide on the vacuum forming hub to see how heavy-gauge forming handles part geometry, materials, trimming and finishing — and to review how formed enclosures behave across your own part family before you lock the process decision.
-
Draw ratio: the ratio of the formed part’s surface area to the original clamped sheet area; higher ratios mean more stretching and greater corner thinning. ↩
-
HDT: Heat Deflection Temperature, measured per ASTM D648 or ISO 75-2 as the temperature at which a specimen deflects a specified amount under flexural load. ↩
-
UL 94: the classification standard for the flammability of plastic materials, grading resins from HB up to V-0 and 5VA by burning and extinguishing behavior. ↩
-
IP code: the ingress protection rating defined by IEC 60529, expressing an enclosure’s protection against solid objects and water. ↩
-
Vicat softening temperature: the temperature at which a flat-ended needle penetrates a plastic specimen 1 mm under a specified load, per ISO 306. ↩



