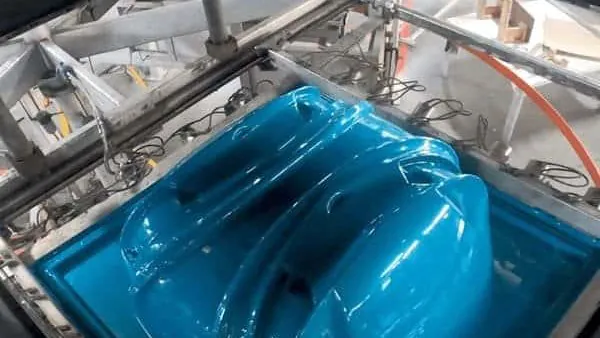
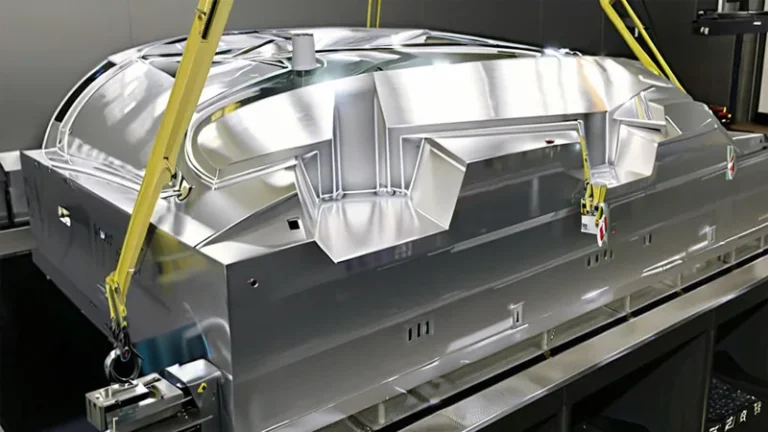
Pick the wrong sheet for a thermoforming project and the consequences show up late: a cover that hazes after its first heat cycle, a tray that cracks at the trim line in winter, an enclosure that fails a flammability review months in. PETG and PVC are two of the most common amorphous sheets specified for heavy gauge vacuum forming, and on a summary datasheet they look interchangeable. Both form at moderate temperatures, both can be made clear, and both cost well below engineering resins. In practice they are not interchangeable, and the differences sit exactly where process engineers get burned.
This comparison walks through the differences that matter — forming window, heat and flame behavior, clarity, chemical resistance, tooling effects and cost drivers — so the material can be shortlisted correctly before tooling is cut. For the wider process picture, start with the vacuum forming overview.
- PETG forms in a wider, more forgiving window; PVC forms at lower sheet temperatures but degrades quickly when overheated.
- PVC is inherently flame retardant, so it often reaches enclosure requirements without additives; PETG needs a certified flame-retardant grade for comparable ratings.
- PETG generally holds better impact strength, especially at low temperatures; PVC resists many acids and alkalis better.
- Both materials make clear formed parts, but optical acceptance should rest on measured transmittance and haze for the actual sheet lot.
- Food-contact and hygiene-critical trays depend on grade certification, not on the base material name.
- Total cost is decided by forming yield, scrap and trim time far more often than by resin price per kilogram.
Why PETG and PVC Both End Up on the Same Shortlist
Both materials are amorphous, which is the core reason they dominate clear and cosmetic forming work. Amorphous sheets pass through a broad, rubbery softening range instead of a sharp melting point, so they sag predictably under radiant heaters and stretch deep into a mold without crystallizing. Both also take mold texture well, trim cleanly on CNC equipment and are stocked in opaque, translucent and clear variants by most sheet suppliers.
PETG, the glycol-modified copolyester of PET, is favored where cosmetic clarity and impact toughness overlap: covers, display glazing, machine guards and thin-wall trays. PVC is favored where cost, chemical resistance and inherent flame behavior matter: industrial trays, packaging, enclosures and liners. That split explains why the two names keep appearing on the same request for quotation — they compete for the same parts from opposite directions.
ZetarVac runs more than 20 thermoforming machines on sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm, so both materials can be evaluated on the same equipment at production scale. The material choice changes the oven profile and tool temperature, not the machine envelope.
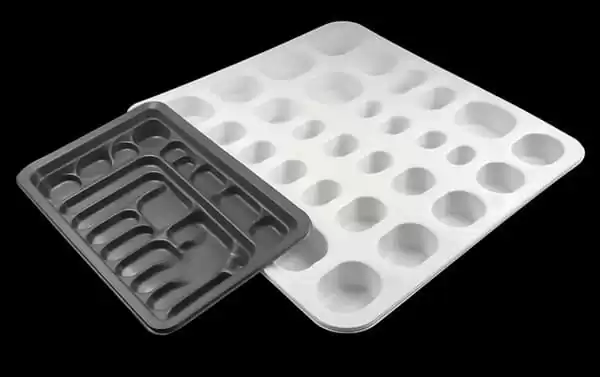
How Do PETG and PVC Behave at Forming Temperature?
PETG offers a wider forming window and slower, more predictable sag, which makes it forgiving on deep draws and complex geometry. PVC forms at a lower sheet temperature with a narrower margin: heat it modestly too far and it starts to degrade, discoloring the sheet and releasing corrosive fumes. That single difference drives most of the setup decisions between the two materials.
Typical radiant-heat practice puts PETG sheet surface temperatures somewhere around 120–160 °C and PVC around 100–140 °C, though exact targets shift with sheet thickness, color, heater type and machine draft. Treat these as starting ranges to confirm on your own equipment, not fixed recipes. PVC asks for tight control because its window sits close to degradation onset: once decomposition starts, the released fumes discolor the part, attack tooling surfaces and demand effective extraction. PETG tolerates a slower ramp and holds heat longer, which suits deep cavities and sharp detail transfer.
Sag behavior differs too. PETG sags gradually and evenly, so operators can time it reliably cycle after cycle. PVC sags quickly and then loses melt strength fast, and an overheated sheet can thin at the center or tear under its own weight before the frame indexes. On cosmetic work, where pressure forming is used for sharper texture and definition, PETG stability under the platen is often the deciding factor; the comparison of vacuum forming and pressure forming covers that variant in detail.
The SPE Thermoforming Division publishes heating and forming practice guidance that applies to both materials and is a useful cross-check whenever a sheet supplier’s forming data looks optimistic.
"PETG and PVC form at the same temperature, so one oven recipe covers both."False
PVC forms at a lower sheet temperature with a much narrower margin above degradation. Running PVC on a PETG profile discolors the part and releases corrosive fumes, while running PETG too cold sacrifices surface detail and leaves molded-in stress.
"Each material needs its own oven profile and sag check before the first production cycle."True
Set the profile from the sheet supplier’s forming data, then confirm it by watching sag time and center-of-sheet temperature. Re-check the recipe whenever thickness, color or lot changes, because all three shift heat absorption.
What About Clarity, Chemical Resistance and Surface Finish?
For clear covers and display parts, PETG usually holds an edge on post-forming impact and resistance to cleaning agents, while PVC counters with lower price and stronger resistance to many acids and alkalis. Both produce optically clear formed parts. The deciding factor is the measured transmittance and haze of the actual sheet lot, not the generic datasheet.
Optical claims should be made measurable. ISO 13468 specifies the determination of the total luminous transmittance of transparent plastics1, and it is a sensible basis for accepting clear covers: set numeric transmittance and haze targets, then verify them on first articles. Both materials can haze if the sheet carries moisture or the oven overheats the surface, so optical checks belong in the inspection plan, not the brochure.
Chemically the two are complementary. PVC stands up well to many acids, alkalis and aqueous salts, one reason it persists in industrial trays and liners. PETG resists lipids, detergents and common disinfectants well — a practical point for equipment covers wiped down daily — but it is attacked by strong alkalis and ketone solvents. Where trays touch food, the grade matters more than the family name: EU Regulation 10/2011 specifies which plastic materials and articles may come into contact with food2, and compliance must be documented on the specific sheet grade, not assumed from the acronym.
"A clear PVC part and a clear PETG part will always look identical after forming."False
Transmittance and haze are lot-specific, and both materials pick up moisture marks or surface bloom when heated incorrectly. Two parts can fail the same optical spec while using nominally identical material.
"Optical quality is accepted against measured transmittance and haze on formed parts."True
Write numeric targets into the drawing and verify them on first articles instead of judging clarity by eye. That makes acceptance reproducible across sheet lots, colors and suppliers.
None of this makes selection difficult; it makes it measurable. Clear-part disputes almost always trace back to acceptance criteria written as adjectives rather than numbers.
PVC sits in the plant’s material library for trays, packaging, industrial enclosures and liners, while PC and PMMA cover clear guards and display covers. A clear-part project therefore usually settles between PVC, PC and PMMA — and PETG belongs in the same conversation whenever impact toughness and cleaning resistance outweigh cost.
Which Material Handles Heat, Flame and Impact Better?
PVC wins on flame behavior because it is inherently flame retardant; PETG needs a certified FR grade to reach comparable classifications. PETG wins on impact toughness, particularly at low temperature. For heat, both are limited, and neither suits parts that sit near continuous service temperatures above roughly 60–70 °C.
Heat deflection tells that story. HDT is the temperature at which a standard bar deflects a fixed amount under flexural load3, and for unfilled PETG and rigid PVC it generally falls in the 60–75 °C region depending on grade and load. That makes both suitable for housings, trays and covers, and unsuitable for anything mounting near heat sources without shielding. When more margin is needed, the conversation moves to PC or PC/ABS grades rather than to additives.
Flame ratings are where the comparison turns asymmetric. UL 94 specifies the flammability classification of plastic materials4, the rating most equipment enclosures and covers must satisfy before an electrical application accepts them. Rigid PVC inherently reaches V-0 behavior in many formulations without additives, while PETG normally requires a flame-retardant grade, which shifts cost, clarity and sometimes formability. For structural validation, sheet and formed parts are routinely tensile-tested to ISO 527-2, which specifies how the tensile properties of plastics are measured5, so properties follow the part rather than the resin family.
| Selection factor | PETG | PVC |
|---|---|---|
| Forming window | Wide, slow and predictable sag | Narrower, fast sag, tight heat control |
| Typical sheet surface range | ~120–160 °C | ~100–140 °C |
| Flame performance | Needs certified FR grade | Inherently flame retardant |
| Low-temperature impact | Strong | Moderate, more notch-sensitive |
| Chemical resistance | Detergents and lipids; weak vs. alkalis and ketones | Strong vs. many acids, alkalis and salts |
| Clear-part optics | High clarity, good haze control | High clarity, high gloss |
| Drying before forming | Recommended | Less sensitive |
| Relative sheet cost | Moderate | Lower |
These ranges are typical for common commercial sheet grades and shift with thickness, color and equipment, so confirm targets with the sheet supplier and on the machine.
How Do the Two Materials Affect Tooling, Trimming and Cost?
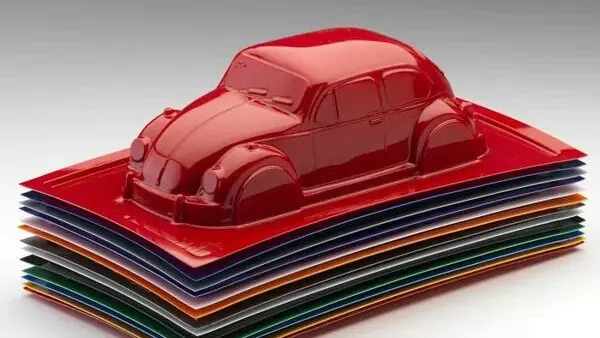
The tool itself changes little between the two materials; the process around it changes a lot. PVC’s degradation fumes push toward stronger extraction and more durable mold surfaces, while PETG’s moisture sensitivity adds a drying step and its toughness changes trimming behavior.
On the tool side, both run on the same cast or machined molds, plug assists and vacuum hole layouts. Two practical differences follow. First, PVC that runs hot will slowly attack aluminum tool surfaces and plug materials, so shops that run it regularly plan for surface maintenance and robust extraction. Second, PETG wants dry sheet: absorbed moisture flashes into bubbles and silver streaks at forming temperature, so PETG jobs often include a drying step that PVC avoids.
Trimming and finishing differ in feel rather than feasibility. PETG, being tougher, resists chipping and cuts cleanly even in cool shops, which favors tight trim lines and thin webs. PVC trims well but can chip at low shop temperatures or in very thin sections, and its lower melt strength punishes aggressive deep draws more visibly. The supplier profile on the China vacuum forming manufacturer page shows how finishing capability maps onto these material behaviors in practice.

ZetarVac finishes formed parts on a 5-axis CNC trimming centre, and the trimmed outline follows the forming tool. Because PETG and PVC shrink slightly differently on cooling, locking the material choice before final tool cuts protects both the formed geometry and the trim program.
Cost questions close the comparison, and they rarely land where buyers expect:
"Resin price per kilogram decides which material is cheaper for a formed part."False
Price per kilogram ignores forming yield, scrap, drying, trim time and compliance testing. A slightly costlier sheet that runs with fewer rejects and less rework often lands cheaper per accepted part.
"Total cost compares forming yield, scrap, trim time and certification, not resin price alone."True
Build the comparison around first-pass acceptance on your actual geometry. Deep draws, textures and tight trim lines amplify material differences that never appear on a datasheet.
FAQ
Which material is better for food-contact trays?
Neither name answers the question — the specific grade does. Both PETG and PVC exist in food-contact certified formulations, and the applicable regulation for the destination market must be documented against the exact sheet grade. Ask the sheet supplier for the compliance declaration for the lot and keep it with the part file.
Does PETG really need drying before vacuum forming?
In most production settings, yes. PETG absorbs enough ambient moisture that heating drives bubbles, streaks and surface blemishes into the formed part. PVC is far less sensitive, which is one reason some shops prefer it for quick-turn industrial work. Drying time depends on sheet thickness and storage history.
Which material should I pick for an outdoor housing?
Neither is ideal without help. Unmodified PETG and PVC both degrade under long-term UV exposure, so an outdoor housing usually shifts to ASA or another UV-stabilized grade. If the housing must stay clear or translucent, discuss UV-stabilized PC with the sheet supplier instead.
How do the two materials compare on post-forming shrinkage?
Both are amorphous, so both shrink far less than semi-crystalline resins — commonly a few tenths of a percent — with PETG typically slightly higher than PVC. Exact values depend on sheet thickness, forming temperature and tool temperature, so tolerance plans should use the supplier’s data for the actual grade.
Where can I review these materials against real thermoformed parts?
The most useful next step is a capability review rather than a quotation: explore the vacuum forming overview to see how heavy gauge sheet is formed, trimmed and finished across the full thickness range, then bring that baseline into your material decision.
-
ISO 13468: ISO 13468 specifies the determination of the total luminous transmittance of transparent plastics, the core metric for accepting clear formed parts. ↩
-
EU 10/2011: EU Regulation 10/2011 governs plastic materials and articles intended to come into contact with food, including thermoformed trays and packaging. ↩
-
HDT: Heat deflection temperature — the temperature at which a standard plastic bar deflects a specified amount under a defined flexural load, used to compare short-term heat resistance. ↩
-
UL 94: UL 94 is the flammability standard for plastic materials, classifying how specimens ignite, burn and extinguish, e.g. V-0, V-1 and HB ratings. ↩
-
ISO 527-2: ISO 527-2 specifies the test conditions for determining the tensile properties of plastics, the standard tensile measurement used to validate sheet and formed parts. ↩