

Thermoforming has a reputation as the low-cost route to plastic parts, and for once the reputation is mostly deserved. A heated sheet is pulled against a single mold surface by vacuum, the tool only defines one face, and the machines are mechanically modest. But cheap hides trade-offs. Buyers who take the label at face value get surprised by trimming bills, material minimums, and tolerance limits that never appeared in the first quotation. This article breaks down where the savings in heavy-gauge thermoforming actually come from, where they disappear, and how to judge whether the process is the economical choice for your part — not just the one that sounds cheapest.
- Thermoforming is cheap because forming pressure, tooling complexity, and machine demands are all low — not because the raw material is cheaper.
- Only one side of the part is molded; the second surface and the trimmed outline depend on sheet quality and post-forming machining.
- Sheet from 0.5 to 15 mm can be formed to lengths of about 2,500 mm, so large housings and trays ship as one part instead of an assembly.
- Secondary operations — trimming, cut-outs, bonding, finishing — are where unit cost quietly grows.
- The process is cheapest when geometry is simple, volumes are low to medium, and one formed surface carries the functional requirements.
Why Is Thermoforming Cheap?
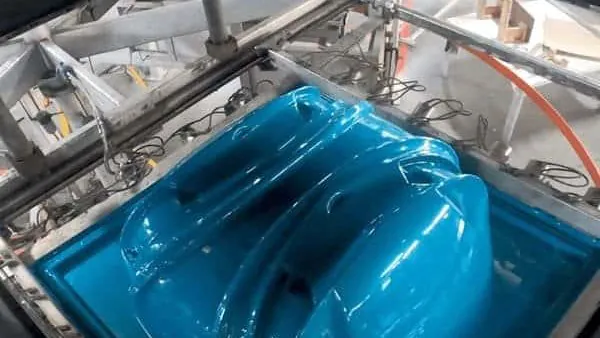
Thermoforming is cheap because it needs far less force than any other way of shaping a plastic part. A softened sheet is drawn onto the mold by vacuum at roughly atmospheric pressure, so tooling can be cut from inexpensive materials, the machines stay simple, and first articles can be formed within days of freezing a design.
Tooling is the headline saving. A vacuum forming tool only has to define one surface, survive clamping loads, and evacuate air, which cast or machined aluminum does without containing any cavity pressure. For a comparable part size, forming tools frequently land an order of magnitude below the tools required by high-pressure processes, and a geometry revision is a CNC edit rather than a rebuild. Nothing about the tool has to fight pressure, so nothing about the tool has to be expensive.
Machine cost follows from the same physics. Because vacuum forming pulls the sheet at about one atmosphere, frames, platens, and clamp systems are sized for modest loads. Pressure forming, which adds compressed air behind the sheet for sharper detail and texture, raises pressures into the several-bar range and costs more in tooling and machine — yet even that equipment class remains lighter than what high-pressure molding demands.
The savings also show up in speed. Heat, drape, vacuum, cool — nothing in that loop needs a long stabilization run, so a tool cut this week forms parts next week. When a buyer is still comparing design options, that speed is worth as much as the tool price itself.
Where Do Thermoforming Savings Show Up First?
Prototyping and early production are where the gap is widest. Tools are quick to cut and revise, so design iterations cost days instead of weeks, and a change late in development is a machining edit rather than a tool rebuild.
Large parts are a quiet cost win. With sheet processed from 0.5 to 15 mm and a maximum forming length of about 2,500 mm, a single formed housing can replace an assembly of several parts, fasteners, and joining labor. Every eliminated joint also removes tolerance stack-up, leak paths, and bill-of-material lines — savings that never appear in a per-piece price comparison but dominate a project budget.
Consolidation only pays if the geometry suits it. If a part truly needs molded-in detail on two surfaces, joining two formed halves adds cost back, and the honest comparison is formed-plus-joined against whatever alternative actually meets the function.
ZetarVac processes sheet from 0.5 to 15 mm on more than 20 vacuum forming and thermoforming machines, with a maximum forming length of about 2,500 mm. For a project owner, that means a large equipment enclosure or machine cover can be formed, trimmed, and supplied as a single part — and the joint count, fastener count, and assembly tolerance issues of a multi-piece build simply disappear from the scope.
Does Cheap Tooling Guarantee Cheap Parts at Volume?
No. Tooling is a one-off cost, so its share of unit price shrinks as volume grows, while sheet material and cycle time take over. Past a certain volume, the advantage narrows unless the part geometry keeps the cycle short.
For a heavy-gauge1 part, the unit-cost anatomy at volume usually reads: sheet material first, forming cycle second, trimming and finishing third, amortized tooling last. Heating dominates the cycle, so wall thickness, draft, and heater zoning decide how many parts a machine delivers per shift. Thin, well-drafted parts cycle fast; thick, deep parts do not.
| Cost driver | Prototype stage | Production stage | What you control |
|---|---|---|---|
| Tooling | Dominant, but low in absolute terms | Amortized toward zero | Draft angles, simple parting, cavity count |
| Sheet material | Minor spend | Largest share of unit cost | Gauge, grade, sheet yield per part |
| Cycle time | Negligible | Second-largest share | Wall draft, heater zones, cooling fixtures |
| Trimming and finishing | Small | Can rival forming cost | Trim lines on tool, hole strategy |
"A low tooling price means the thermoformed part will be cheap to produce."False
Tooling is a one-off that gets amortized; at production volumes the unit price is driven by sheet material and cycle time. A part with a long forming cycle or poor sheet yield can cost more per piece than a tool that cost twice as much.
"Thermoforming is most cost-effective at low to medium volumes."True
The process avoids high-pressure tooling and long stabilization runs, so savings are real from the first batch and tool amortization stays relevant. As volumes climb and cycle time dominates, the economics need to be re-checked part by part.
At the procurement stage, ask for the split: tool, material, forming cycle, trimming, finishing. Itemized numbers show which lever actually moves your unit cost, and those levers are worked through in detail in Cost Control in Thermoforming.
How Do Material and Sheet Choices Move the Price?
Material choice is the lever customers underestimate most. ABS, HDPE, and PP are the workhorses of cost-sensitive formed parts; PC and PMMA buy clarity and impact performance; PA6, POM, and glass-filled grades serve special structural applications. Every step up the grade ladder adds sheet cost and often narrows the processing window.
Validation belongs in the material decision. ASTM D638 governs the tensile properties of plastics and is the standard tensile test run on thermoformed sheet, so incoming material can be verified against the grade datasheet before a production run starts. Where a formed panel sits near a heat source, the heat deflection temperature2 from ISO 75-2 data tells you whether it holds shape under load — do not assume room-temperature behavior persists.
Two more checks belong in every material review. Ask what regrind content the sheet carries3, because reprocessed material lowers price and raises bubble and splay risk in deep draws. And for clear formed covers, ISO 13468 specifies how the total luminous transmittance of transparent plastics is measured, which turns clarity from a visual judgment into a number.
Compliance can also block a downgrade. UL 94 classifies the flammability of plastic materials, and many formed equipment enclosures must meet a specified UL 94 rating4 before they can be approved for electrical equipment use. A grade premium is almost always cheaper than a failed approval.

Material is one of the few cost levers a customer can pull directly. ZetarVac forms ABS for automotive interiors, equipment housings, cases, and guards; HDPE for industrial trays, liners, and storage boxes; PP for trays and equipment liners; PC and PMMA for clear guards and covers; and PC/ABS or ASA where impact and weathering combine. Matching the grade to the real exposure — indoor, outdoor, clear, structural — usually recovers more margin than squeezing the forming cycle.
What Adds Cost After the Sheet Is Formed?
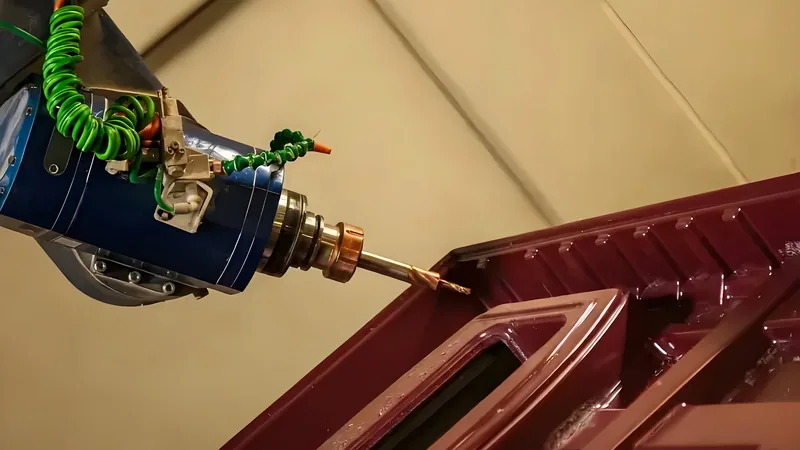
Trimming and detail work. The forming step shapes one surface, but a precise outline, cut-outs, and mounting holes all happen afterward — typically on a 5-axis CNC trimming centre so the trimmed outline follows the forming tool.
Trim cost scales with cut length, feature count, and the tolerance demanded on trimmed edges. Forming holes in the tool is cheap but limits geometry; machining them afterward is flexible but adds handling. Bonding, inserts, and decorating each carry their own operation cost. Surface defects from poor heating — bubbles and splay marks — multiply through every later step, because rework or rejection now includes the finishing work already invested; those failure modes are covered in Bubbles and Splay Marks in Heavy-Gauge Thermoforming.
"Once the first article passes inspection, production parts will stay within tolerance."False
Between first article and full production, sheet gauge variation, regrind content, and heater drift all move the process. A process signed off on one sheet lot can drift into thin corners or warped flanges several hundred parts later unless sheet input and heater zones are re-checked.
"Stable thermoforming output depends on controlling the incoming sheet."True
Formed parts inherit the sheet — its gauge, its lot, its thermal history. Verification at sheet intake plus periodic first-off checks on the machine keeps production inside the window the first article validated.
Is Thermoforming Always the Cheapest Option?
No. When a part needs tight tolerance on the non-molded surface, near-uniform wall in two directions, or very high volumes with short cycles, other forming processes can win. Thermoforming is cheapest when one formed surface carries the function and the second surface only needs to be reasonable.
Geometry decides a lot. Deep, tight-radius draws push the draw ratio5 up, and wall thinning follows: the corners stretch first and end up thinnest, which is where rejection risk concentrates. Undercuts, sharp interior corners, and critical details on the free surface all push cost back into tooling, machining, or redesign. The parts that form cheaply have generous draft, generous radii, and their functional features on the mold side.
"The quoted price for a thermoformed part covers everything through final assembly."False
Forming, trimming, and finishing are usually quoted as separate operations, and assembly, packaging, and logistics may not appear in the number at all. Comparing quotes that bundle different scopes is how projects end up with a cheap part and an expensive invoice.
"A fair thermoforming quote itemizes tool, material, forming, trimming, and finishing."True
Separate line items make the scope explicit and let suppliers be compared on the same work content. They also show which operation to target when unit cost has to come down later.
Scope clarity protects the schedule as well as the price. When finishing operations are named and priced, the capacity behind them can be checked against the delivery window before the order is placed instead of after.
Volume flexibility is part of the cost picture. ZetarVac supports prototyping, small batch, and large batch production, with a reference monthly capacity of about 100,000–200,000 pieces. For the buyer, that means the tooling and process economics described here can be tested with a small batch first and scaled up without changing the process route.
FAQ About Thermoforming Cost
Why is vacuum forming cheaper than other plastic forming processes?
Because it shapes the part at low pressure with single-surface tooling. Vacuum forming pulls the softened sheet against the mold at roughly atmospheric pressure, so tools can be cut from inexpensive materials, machines are simpler, and no long stabilization runs are needed. The saving is built into the physics, not into a discount.
How much cheaper is a thermoforming tool?
For a comparable part size, forming tools frequently run an order of magnitude below high-pressure tooling, but the exact ratio depends on part size, material, texture, and cavity count. The reliable way to find out is to have tool price and piece price quoted as separate line items.
Does thermoforming stay cheap at high volumes?
Partly. Tooling amortizes away, but sheet material and cycle time do not, so the per-piece gap narrows as volume grows. Re-examine the itemized cost split once annual volume is known rather than assuming the prototype-stage picture still holds.
What sizes and thicknesses can heavy-gauge thermoforming cover?
Sheet from 0.5 to 15 mm can be processed, with a maximum forming length of about 2,500 mm, and formed parts are trimmed on a 5-axis CNC centre. That range covers equipment housings, trays, and structural covers as single formed parts.
Which materials keep a formed part cheap?
ABS, HDPE, and PP are the usual cost-effective choices for industrial parts, trays, and housings. Before downgrading a grade, check what the part has to pass — heat exposure, flammability rating, clarity — because a failed requirement costs far more than the grade premium ever saved.
To keep digging, explore the vacuum forming hub for the process fundamentals behind these cost mechanics, or review how a heavy-gauge vacuum forming manufacturer in China structures tooling, materials, and capacity for exactly these decisions.
-
Heavy gauge: Heavy gauge (thick-gauge) thermoforming processes sheet roughly 0.5 mm and thicker, typically in cut-sheet form, as opposed to thin-gauge roll-fed work. ↩
-
HDT: Heat Deflection Temperature is the temperature at which a standard plastic bar deflects a specified amount under flexural load, defined in ISO 75-2 and ASTM D648. ↩
-
Regrind: reprocessed skeletal trim and scrap mixed back into sheet material; its content affects melt behavior and surface quality. ↩
-
UL 94: the flammability classification standard for plastic materials, grading burning behavior from HB up to V-0 and 5VA. ↩
-
Draw ratio: the ratio of formed part surface area to original sheet area; higher values mean more wall thinning in deep draws. ↩

