

Plastic housings are the visible and structural shell of a machine: they carry mounts, shed impacts, protect electronics, and set the perceived quality of the product. Heavy gauge thermoforming has earned a central place in this application because it combines large forming envelopes, moderate tooling cost, and fast design iteration. This guide explains where the process wins, which parameters decide quality, and how a buyer should judge a formed housing before committing to production volume.
- Heavy gauge thermoforming converts 0.5–15 mm sheet into rigid, large housings with tooling cost far below comparable molding routes.
- The process window — sheet temperature, vacuum timing, and cooling discipline — governs dimensional stability more than thickness alone.
- ABS, PC, PC/ABS, and ASA dominate housing work, each mapping to different stiffness, heat, and weathering requirements.
- Five-axis trimming plus standards such as UL 94 and ASTM D790 define how a formed housing is validated.
- First-article approval does not guarantee volume stability; tolerances must be assigned per surface, not applied blanket-tight.
Why Does Heavy Gauge Thermoforming Suit Plastic Housings?
Heavy gauge thermoforming suits housings because it forms large, rigid shells from thick sheet with low-pressure tooling, so a new enclosure reaches first parts in weeks at a fraction of the tooling investment of other molding routes. Large forming envelopes and fast iteration match how housing designs actually evolve during development.
Three factors drive the fit. First, scale: sheet up to 15 mm thick and forming lengths around 2,500 mm allow single-piece enclosures that would otherwise be assembled from several parts, eliminating joints, fasteners, and potential sealing gaps. Second, tooling economics: a vacuum forming tool is a low-pressure shape, typically cast or machined aluminium, so revising a housing after a design review costs days rather than weeks. Third, wall strategy: because the sheet drapes over the mold, a designer can thicken visible faces while accepting thinner return flanges in a single forming operation.
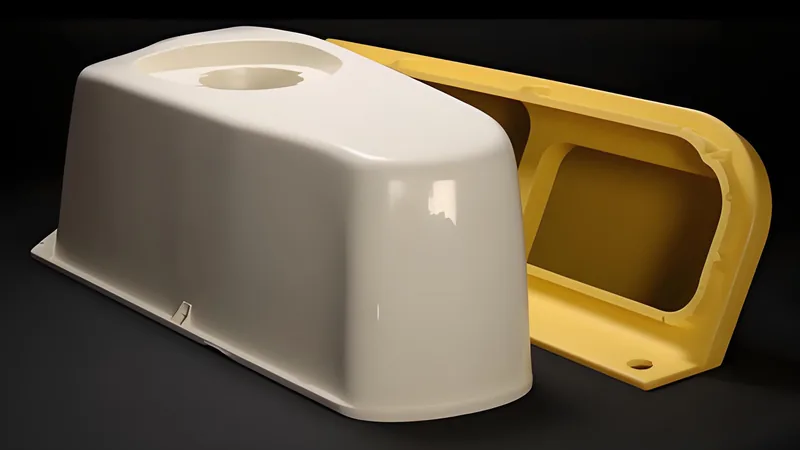
Materials reinforce the argument. Enclosure-grade sheet such as ABS, PC/ABS, and PC is supplied in housing thicknesses and textures specifically for thermoforming lines, and flame-rated grades are widely available for electrical equipment covers. When one tool can trial three candidate grades at prototype scale, material selection becomes an engineering decision supported by formed samples rather than a procurement guess.
ZetarVac operates 20+ vacuum forming and thermoforming machines processing sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm, so most industrial and medical housings can be formed as a single shell and finished on a five-axis CNC trimming centre without secondary handwork.
The practical consequence for a buyer is schedule control. Because the same forming route covers prototype batches and volume production, a housing program can move from design review to pilot units to mass production without changing process, supplier base, or validation logic.
"A vacuum formed housing will hold machined-panel tolerances on every surface."False
Formed surfaces follow the sheet as it drapes and cools, and differential shrinkage pushes free areas well beyond machined tolerances. Writing blanket-tight numbers across the whole shell leads to rework, price creep, and rejected first articles.
"Formed housings need tolerances assigned per surface and per feature."True
Correct practice puts tight tolerances only on trimmed edges, holes, and mounting interfaces that mate to other parts. Free formed walls receive wider process tolerances, which protects first-pass yield without adding cost.
What Process Window Decides Quality in Heavy Gauge Work?
Sheet temperature, vacuum timing, and cooling discipline decide quality. A heavy gauge housing is only as stable as its thermal history: under-heated sheet forms with high springback, over-heated sheet sags and picks up heater marks, and uncontrolled cooling locks in warp.
For common housing materials, the sheet surface is typically heated into roughly the 130–180 °C range before forming, with the exact setpoint depending on grade, gauge, and heater zoning; PC and its blends sit near the upper end, ABS near the middle. Thick sheet needs a longer soak because heat must penetrate the full section, not just the skin. The second classic error is late vacuum: vacuum must be applied within seconds of the sheet reaching its forming window, or the sheet cools and detail is lost. Capable shops verify temperature with a probe or infrared reading on the sheet itself, not the heater bank, and record the value for every setup.
Heat capability is judged with data, not guesswork: ISO 75-2 specifies the determination of the deflection temperature of plastics under flexural load, and that value tells you whether a formed housing will hold its shape near heat-generating electronics instead of slowly deflecting in service.1
Which Materials Work Best for Thermoformed Housings?
ABS remains the default for indoor housings, while PC/ABS and PC take over where impact performance and heat resistance matter, such as electrical and medical equipment. ASA and other weatherable grades carry outdoor duty without painting, and HDPE and PP cover industrial trays, liners, and chemically exposed covers. The table below summarizes the common mapping.
| Material | Typical housing role | Selection logic |
|---|---|---|
| ABS | Indoor equipment housings, cases, guards | Balanced stiffness, cost, and formability |
| PC | Clear guards, protection covers, medical housings | High impact strength and heat resistance |
| PC/ABS | Automotive interiors, electrical equipment housings | Impact performance with easier forming |
| ASA | Outdoor equipment housings, exterior automotive parts | Weatherable surface without painting |
| HDPE | Industrial trays, equipment liners, storage boxes | Chemical resistance and low material cost |
| PP/GF | Structural industrial and automotive parts | Stiffness from glass fiber reinforcement |
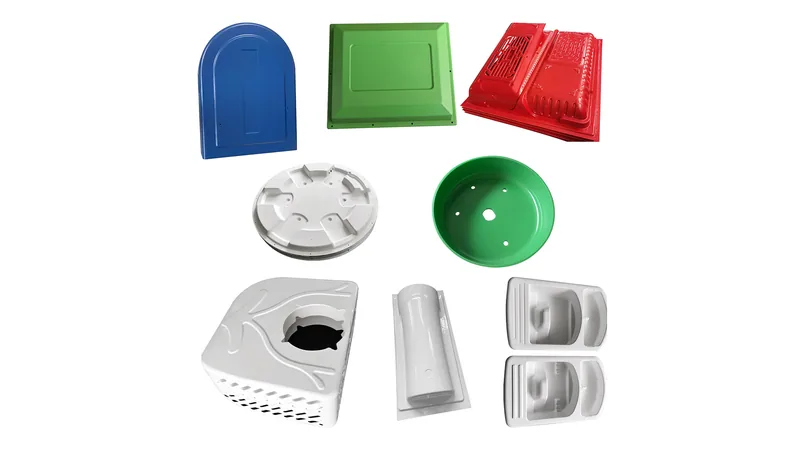
For electrical equipment, compliance follows the polymer, not only the part: UL 94 classifies the flammability of plastic materials, and many formed enclosures must therefore use a flame-rated sheet grade so the finished housing can support the end-product safety requirements.2
The ZetarVac material library covers PVC, ABS, HDPE, LDPE, PP, PC, PMMA, PA6/PA66, POM, TPE, TPU, TPV, PC/ABS, ASA, and PP/GF, so a housing program can start in ABS for prototyping and move to PC/ABS or ASA for production without changing the forming route or trimming concept.
Grade selection also interacts with the process window. Higher-temperature materials such as PC demand tighter heater control and longer soaks, while ABS forgives setup drift. This is why an experienced thermoforming shop asks for the operating environment — continuous temperature, impact exposure, UV, chemical contact — before recommending a grade, rather than defaulting to the cheapest sheet on the shelf.
"Once the first article passes inspection, the production run will stay within specification."False
A first article reflects one sheet, one setup, and one operator on one day. Without a documented process window and incoming sheet controls, normal variation in heating and cooling will drift parts out of tolerance during volume production.
"Stable volume output requires a defined process window, not just an approved part."True
Serial production holds tolerance when sheet temperature, vacuum timing, and cooling are specified and recorded for every setup. With those parameters fixed and audited, first-article performance becomes repeatable rather than lucky.
How Are Formed Housings Trimmed and Validated?
Trimming and validation are where a formed shell becomes an installable housing. At ZetarVac, formed parts are finished on a five-axis CNC trimming centre, and because the trimmed outline follows the forming tool datum, cutouts and drilled features stay consistent from the first part to the last.
Structural acceptance usually starts with stiffness: ASTM D790 covers the determination of flexural properties of plastics, and it is the standard test behind the panel-stiffness values a housing designer relies on when choosing sheet gauge and rib strategy.3 Where a housing claims ingress protection, IEC 60529 defines the degrees of protection provided by enclosures — the IP code — and that rating must be earned through gasket design and flange geometry, not assumed from a material datasheet.4
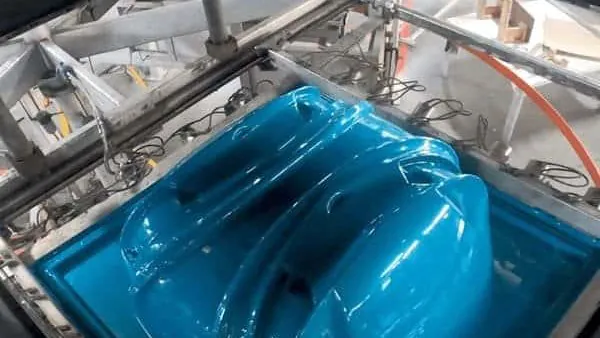
A practical validation plan separates feature classes: mounting hole positions and connector cutouts are checked against tight per-feature tolerances, free formed walls are checked against process tolerances, and cosmetic surfaces are checked against an agreed appearance standard. Reviewing a supplier’s DFM checklist for heavy gauge thermoformed parts and molds before tooling starts is the cheapest moment to catch datum and tolerance conflicts.
"Thicker sheet always produces a stronger housing."False
Bending stiffness scales with the cube of thickness, but heavy gauge also means longer heat cycles, deeper corner thinning, and harder vacuum distribution. A poorly designed 8 mm shell can distort more in service than a well-designed 5 mm version with ribs and correct flange geometry.
"Gauge, geometry, and material must be optimized together for housing stiffness."True
Ribbed flanges, generous radii, and the right grade often beat raw thickness. The correct engineering move is to set stiffness targets first, then choose the minimum gauge and geometry that meet them in the selected material.
What Failure Modes Should You Watch on Vacuum Formed Housings?
The dominant defects are webbing between closely spaced features, bubbles or blisters from trapped moisture, corner thinning in deep draws, and post-forming warp. Each traces to a specific process variable, which makes them diagnosable rather than mysterious.
Webbing appears when excess sheet bridges between bosses or ribs that sit too close together; it is fixed in the tool or the design, not at the trim station. Bubbles in ABS and PC sheet come from absorbed moisture expanding under heat, which is why hygroscopic sheet must be dried before forming. Corner thinning concentrates where the draw ratio is highest, so critical features should be moved away from deep corners or the sheet should be pre-stretched. Warp follows uneven cooling, and it is controlled with symmetric fixturing and disciplined cycle timing.

Most of these mechanisms are prevented during design review rather than caught at inspection. The DFM checklist for heavy gauge thermoformed parts and molds covers draft, radii, and boss spacing before tooling is cut, and the guide to bubbles and splay marks in heavy gauge thermoforming explains the moisture and heating mechanisms in detail.
With 45+ production lines across the plant and a reference monthly capacity of about 100,000–200,000 pieces, ZetarVac supports prototyping, small batches, and large batch production on the same forming route, so a housing validated at pilot scale does not need a new process when volume grows.
FAQ
What sheet thickness counts as heavy gauge thermoforming?
Heavy gauge generally describes sheet above roughly 1.5–3 mm, thick enough that the formed part is rigid without reinforcement. At ZetarVac the forming window runs from 0.5 to 15 mm, which spans thin protective covers through thick structural shells, with the practical gauge chosen from stiffness and draw requirements.
Can a vacuum formed housing meet flame and ingress requirements?
Yes, when the sheet grade and the geometry are chosen for it. Flame performance comes from UL 94 rated grades, while ingress protection depends on gasketed flanges and overlapping joints designed into the part. Both should be agreed before tooling so the housing geometry supports the target rating.
How tight can tolerances be on a formed housing?
Tolerances should be assigned per feature class. Trimmed edges, holes, and mounting interfaces hold tighter limits because they are machined against the tool datum, while free formed walls need wider process tolerances. Blanket-tight specifications across the whole shell usually raise cost without improving fit.
How large can a thermoformed housing be?
At ZetarVac the maximum forming length is about 2,500 mm with sheet from 0.5 to 15 mm, which covers full-size machine enclosures and covers as single shells. Large parts should be reviewed early for draw depth, undercuts, and trim access so the geometry stays formable.
Does heavy gauge thermoforming work for medical equipment housings?
Yes. A typical example is a large, curved PC housing for diagnostic equipment with custom cutouts, mounting holes, and reinforcement formed in one piece. PC brings the impact and cleaning-agent resistance medical environments require, and five-axis trimming keeps the interface features accurate to the internal frame.
If you are mapping a housing program and want to understand how the process window, material grades, and trimming route fit together, explore the ZetarVac vacuum forming overview or review how a dedicated vacuum forming manufacturer structures DFM and validation before you shortlist suppliers.
-
ISO 75-2: Standard for determining the deflection temperature of plastics under flexural load in a heated environment, an indicator of heat capability in service. ↩
-
UL 94: Standard for the flammability of plastic materials for parts in devices and appliances, classifying burning and self-extinguishing behavior. ↩
-
ASTM D790: Standard test methods for flexural properties of unreinforced and reinforced plastics and electrical insulating materials, used to characterize the bending stiffness of sheet and formed panels. ↩
-
IEC 60529: International standard defining degrees of protection provided by enclosures against ingress of solids and water, known as the IP code. ↩



