
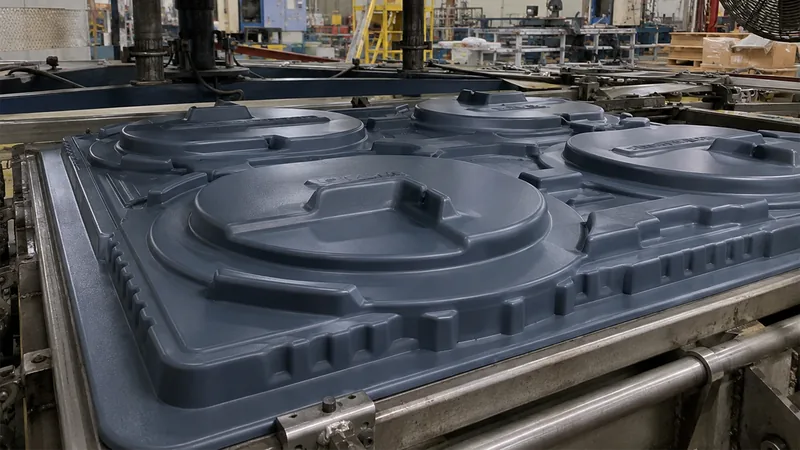
Heavy-gauge thermoforming turns plastic sheet between 0.5 and 15 mm into structural housings, trays, covers and industrial components — and vacuum forming is only one of the ways to drive that heated sheet against a mold. This guide separates the four main thermoforming types, gives the process windows and failure modes that matter in production, and lists the tests that decide whether a formed part passes.
- Thermoforming splits into four main types: vacuum forming, pressure forming, twin-sheet forming and plug-assist forming.
- Vacuum forming is the default for heavy-gauge structural parts; pressure forming adds positive air pressure for sharper detail and texture on cosmetic surfaces.
- Heavy-gauge work is defined by cut sheet from 0.5 to 15 mm and forming lengths up to about 2,500 mm, producing long-service parts rather than disposable packaging.
- Draw ratio, oven zone balance and cooling discipline control corner thinning — the primary failure driver in vacuum forming.
- Validation typically runs through tensile (ISO 527-2), flexural (ASTM D790) and heat deflection (ISO 75-2) testing on the formed sheet.
- Formed enclosures add flammability (UL 94) and ingress protection (IEC 60529) requirements on top of dimensional checks.
What Are the Main Types of Thermoforming?
The main types are vacuum forming, pressure forming, twin-sheet forming and mechanical plug-assist forming. The classification comes from how the heated sheet is driven against the mold: by vacuum alone, by positive air pressure, by two sheets formed back to back, or by a plug that pre-stretches the sheet before vacuum completes the draw.
Every variant shares the same skeleton: clamp a thermoplastic sheet, heat it into its forming window, drive it against a single-sided mold, cool, then trim. What changes is the driving force, and that choice cascades into surface finish, wall-thickness distribution, tooling cost and cycle time. For heavy-gauge parts — enclosures, machine covers, trays, structural components — vacuum forming and pressure forming dominate, while twin-sheet and plug-assist appear when geometry demands them.
ZetarVac runs more than 20 vacuum forming and thermoforming machines processing sheet from 0.5 to 15 mm with forming lengths up to about 2,500 mm — the full heavy-gauge range these process types cover.
Plug-assist forming1 deserves a note here even though it is less visible to buyers. A matched plug, usually wood, syntactic foam or aluminum and kept below sheet temperature, pushes the sheet partway into the cavity before vacuum pulls it home. The plug pre-distributes material so deep corners keep wall thickness instead of draining it — a common fix when a deep-draw part webs or thins out under vacuum alone.
Vacuum Forming: The Baseline Heavy-Gauge Process
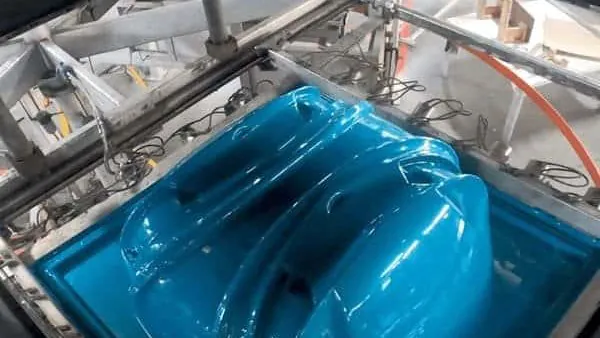
Vacuum forming pulls the softened sheet against the mold by evacuating the space between sheet and tool. Industrial systems typically pull 25–29 inHg (roughly 85–98 kPa), which means the available forming force never exceeds about one atmosphere. That ceiling is why vacuum forming favors open geometries and moderate draw depths, and why the process window is defined by sheet temperature, vacuum ramp time and cooling rate rather than by brute force.
Heating is where most heavy-gauge problems start. The sheet must reach a forming temperature near its softening range — roughly 130–180 °C for ABS depending on grade and equipment, higher for PC — and both surfaces need even heat. Overheated sheet blisters or sags uncontrolled; underheated sheet forms with excessive corner thinning and lost detail. Infrared ovens are zone-controlled so edges and center can be balanced, and a competent molder locks the window with a first-article study before committing to a run.
The characteristic failure modes are webbing, where folds bridge inside corners; chill marks, where cold tool or cold sheet freezes the surface mid-draw; and non-uniform wall thickness concentrated at the deepest draws. Webbing is managed with sheet tension, plug pre-stretch or mold redesign, chill marks by raising mold temperature and rebalancing oven zones. All three trace back to draw ratio2 — the ratio of formed surface area to original sheet area — and it is the first number a molder calculates when quoting a deep part.
Mold design choices compound these effects: cavity count, draft angles, vent sizing and the male-versus-female decision all shift where material thins. Our guide to thermoforming mold cavities walks through those trade-offs in detail.

For process theory beyond the shop floor, the SPE Thermoforming Division publishes peer-reviewed technical papers covering sheet heating, draw-ratio behaviour and pressure assistance across all forming variants.
Pressure Forming: Paying for Surface Detail
Pressure forming seals the sheet edge against a pressure box and adds positive air pressure — commonly 3–5 bar on well-equipped lines — on top of vacuum. That multiplier on forming force pushes plastic into sharp corners, crisp vents and molded-in texture, producing near-injection-grade surface quality on the tool-contact face.
Where plain vacuum forming leaves one side glossy against the tool and the other side matte, pressure forming transfers texture and fine detail to the formed surface. Equipment housings, medical device covers and retail display parts are the classic beneficiaries: the cosmetic face reads as molded-in texture rather than applied finish. The costs are real — tooling needs a pressure box, sealing surfaces and a stiffer clamp frame, cycle times run marginally longer, and the process window is narrower, so cosmetic scrap risk rises without a molder who runs the process daily. Surface appearance choices interact with this decision too, and our guide to different colors in thermoforming covers that side of it.
"Pressure forming is just expensive vacuum forming, so the two quotes are interchangeable."False
The added air pressure changes what the tool must survive: the mold needs a pressure box, sealing surfaces and a stiffer frame. Buying a vacuum-forming quote for a pressure-forming part ends with soft corners, lost texture and failed cosmetic inspection.
"Pressure forming only pays for itself on visible, cosmetic surfaces."True
If the part is a hidden structural tray or an internal liner, the extra tooling cost and tighter process window buy nothing. Reserve pressure forming for faces where texture, sharp radii or fine detail are specification items, and run plain vacuum forming everywhere else.
How Do Thin-Gauge and Heavy-Gauge Thermoforming Differ?
The dividing line is sheet gauge and part duty. Thin-gauge thermoforming runs roll-fed material in thin gauges into high-cavity disposable packaging; heavy-gauge thermoforming loads cut sheet — from 0.5 to 15 mm on ZetarVac’s floor — one blank at a time, and the output is structural: enclosures, machine covers, trays and load-bearing components. Between those poles sits a medium band where the two approaches overlap.
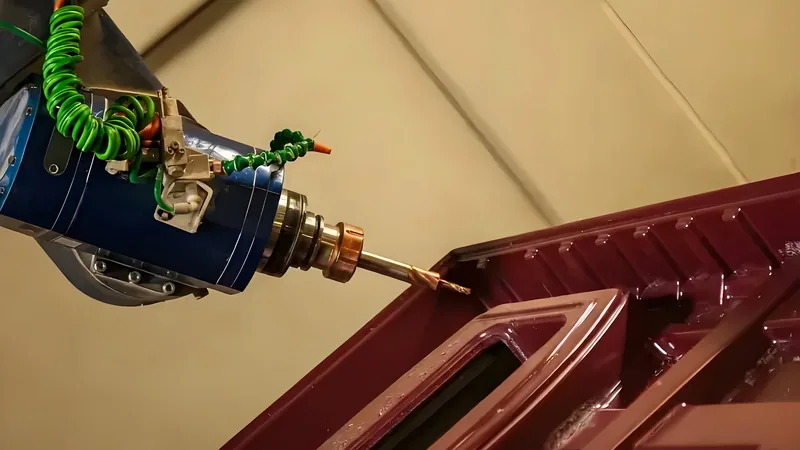
Heavy-gauge work changes the engineering conversation. Sheet sag, forming length and trimming dominate: a 2,500 mm enclosure cover needs oven zoning across its full length and a trimming method that holds outline accuracy without hand finishing. This is why heavy-gauge shops invest in 5-axis CNC trimming — the trimmed outline follows the forming tool’s datum, so cutouts and mounting holes land where the mold put the material, run after run. Wall thickness is a distribution, not a single number: a panel formed from 6 mm sheet might finish near 3.5 mm in deep corners and 5.5 mm on flat faces, and the drawing has to tolerate that spread.

Formed parts at ZetarVac are trimmed on a 5-axis CNC centre whose outline follows the forming tool, so cutouts and mounting features repeat part to part without secondary fixturing drift.
Sheet thickness range, in other words, is the entry ticket — process control across production lots is what keeps the parts conforming.
"Once the first article passes, heavy-gauge vacuum forming holds that accuracy for the whole run."False
First-article approval validates the setup, not the process. Sheet lot changes, oven element ageing and cooling-water drift all move wall thickness and outline between lot 1 and lot 10, so a heavy-gauge run needs periodic in-process checks rather than a single sign-off.
"Consistent heavy-gauge output is a process-control problem, not a tooling problem."True
A sound mold is a prerequisite, but dimensional stability across a run is governed by sheet lot consistency, oven zone calibration and cooling discipline. Ask a heavy-gauge supplier how they monitor those variables mid-run before you judge their quoted tolerance.
Which Thermoforming Type Fits Your Part?
Match the forming type to three variables: surface requirement, geometry depth and structural load. Vacuum forming suits open structural geometries, pressure forming suits cosmetic faces, twin-sheet forming suits hollow rigid panels, and plug-assist forming suits deep draws where wall distribution is critical.
| Forming type | Driving force | Typical sheet | Best suited for | Main watch-outs |
|---|---|---|---|---|
| Vacuum forming | Vacuum alone (≈1 atm) | 0.5–15 mm | Enclosures, trays, machine covers, liners | Corner thinning on deep draws, webbing |
| Pressure forming | Vacuum + 3–5 bar air | 0.5–10 mm | Cosmetic housings, display covers, textured panels | Tooling cost, narrower process window |
| Twin-sheet forming | Vacuum on two sheets | 2–10 mm per sheet | Hollow structural panels, double-wall parts | Sheet registration, weld quality |
| Plug-assist forming | Mechanical plug + vacuum | 1–15 mm | Deep draws needing even wall distribution | Plug temperature and material matching |
Quantities matter less in thermoforming than in most plastics processes because molds are single-sided and comparatively inexpensive, so prototypes, small batches and large runs are all viable. ZetarVac supports prototyping through large-batch production with a reference monthly capacity of roughly 100,000–200,000 pieces, letting the forming-type decision follow part requirements instead of volume thresholds. For a part-by-part view, our guide to products suitable for thermoforming maps common applications to materials.
Material selection maps directly onto these forming types: ABS and PC/ABS serve housings and guards, PC serves clear protective covers, PMMA delivers transparent display parts, and PP or HDPE carry industrial trays and liners.
What Tests and Standards Govern Formed Parts?
Formed parts are validated with the same mechanical tests used across plastics engineering: tensile per ISO 527-2, flexural per ASTM D790 and heat deflection per ISO 75-2 — run on the formed sheet, because thermoforming orients and thins the material.
ISO 527-2 specifies the tensile test method used to measure strength and elongation of thermoformed sheet, and it matters because forming stretches and orients the polymer, so raw-resin datasheets overstate what the formed wall actually delivers. ISO 75-2 defines the heat deflection temperature of plastics under flexural load3, the property that decides whether an enclosure near a heat source holds its shape in service. For stiffness-critical panels, ASTM D790 flexural testing on formed sheet predicts how a housing wall resists bending under load.
Equipment housings and covers add regulatory layers. UL 94 classifies the flammability of plastic materials, and many electrical enclosures specify a minimum flame rating for the housing material. IEC 60529 defines the ingress-protection (IP) code4 that rates how well a formed cover seals against dust and water, which drives gasket design and flange geometry rather than forming parameters alone. For outdoor equipment, ASA and UV-stabilized grades enter the material conversation alongside the forming-type decision.
"Thicker starting sheet always produces a stronger formed part."False
Forming stretches the sheet, and deep draws thin corners far more than flat faces — a 6 mm blank can end up near 3 mm in a sharp corner. Strength follows the thinned wall and the draw ratio, so a shallower draw in thinner sheet can outperform a badly designed deep draw in thick stock.
"Corner thinning decides part strength more than starting gauge does."True
Wall-thickness distribution is set by draw ratio, mold geometry and plug design. A well-engineered deep draw keeps critical corners inside the minimum-wall callout, and tensile testing on the formed sheet confirms it — which is why minimum-wall tolerance belongs on the drawing, not just nominal thickness.
FAQ
Is vacuum forming the same as thermoforming?
No. Thermoforming is the family of processes; vacuum forming is one member of it. Pressure forming, twin-sheet forming and plug-assist forming are also thermoforming, each driven by a different forming force.
Which thermoforming type is cheapest for low volumes?
Vacuum forming, because it needs only a single-sided mold and no pressure box. Prototyping, small batch and large batch production are all supported, and single-sided tooling keeps early volumes affordable.
What sheet thickness counts as heavy gauge?
Heavy-gauge thermoforming generally works with cut sheet processed between 0.5 and 15 mm and forming lengths up to about 2,500 mm, producing structural parts rather than disposable packaging.
Can pressure forming reproduce injection-molded surface quality?
Close, on the tool-contact face. Pressure forming transfers mold texture and sharp detail at several bar of air pressure, which reads as molded-in finish; the non-tool side stays untextured, and very fine features still favor other processes.
What materials work across these forming types?
ABS, PC, PC/ABS, HDPE, PP, PMMA, ASA, PA6/PA66, POM, TPE, TPU, TPV and PP/GF all form on heavy-gauge equipment; the choice follows the part’s duty — housings, clear covers, trays or structural components.
To keep digging, explore the ZetarVac vacuum forming guide for deeper process and material detail, or see how a China vacuum forming manufacturer structures heavy-gauge projects from sheet selection through 5-axis trimming.
-
Plug assist: A forming aid — typically heated wood, syntactic foam or aluminum — that pre-stretches the sheet into the cavity before vacuum completes the draw, improving wall-thickness distribution. ↩
-
Draw ratio: The ratio of formed surface area to original flat sheet area; higher draw ratios concentrate thinning at corners and deep features. ↩
-
HDT: Heat deflection temperature, measured per ISO 75-2 as the temperature at which a standard specimen deflects a set amount under a specified flexural load. ↩
-
IP code: The ingress-protection rating defined by IEC 60529, classifying how well an enclosure seals against dust and water. ↩

