

Heating decides whether heavy-gauge thermoforming succeeds or scraps parts. Before a sheet can be drawn over a mould, it must reach a uniform forming temperature through its full thickness, not just at the surface. The heating method, and how tightly it is controlled, determines wall-thickness distribution, surface finish, cycle time and whether a part stays flat after trimming. This article walks through the three heating methods used in industrial practice, where each one fits, and how to control and inspect the heating stage in thick-sheet vacuum forming.
- Infrared radiant heating is the default method for heavy-gauge thermoforming: fast, non-contact and dividable into independent heating zones.
- Contact heating on hot plates and convection preheating are secondary methods, used for very thick stock, flat panels or gentle preheat.
- The target is through-heating: the core of the sheet must reach forming temperature, not only the surface.
- Heating time scales strongly with sheet thickness, so a 15 mm sheet needs far more soak than a 0.5 mm sheet on the same machine.
- Zone-by-zone control, sag observation and direct temperature measurement together catch uneven heating before it becomes scrap.
- Every material — PVC, ABS, PC, PMMA, PP and the rest — has its own heating window, so recipes are qualified per material and gauge.
What Are the Methods of Thermoforming Heating?
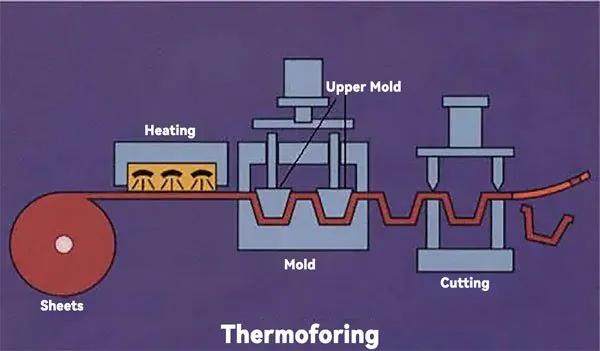
The three methods of thermoforming heating are infrared radiant heating, contact heating and convection heating. Infrared emitters radiate energy directly into the sheet, contact heating conducts heat from a heated plate into the sheet face, and convection warms the sheet with circulating hot air. Heavy-gauge vacuum forming machines combine them, most commonly as infrared banks above and below the sheet, sometimes with a convection preheat stage for thick stock.
These methods are building blocks rather than rivals. Machine builders choose heater type, watt density, heater-to-sheet distance and zoning based on the largest and thickest sheet the machine must form. On a heavy-gauge line processing 0.5–15 mm stock, the heating station is usually the largest and most instrumented section of the machine, because every downstream defect traces back to how evenly the sheet entered the forming step. For a wider process overview, see our vacuum forming guide.
Infrared Heating: The Default for Heavy-Gauge Sheet
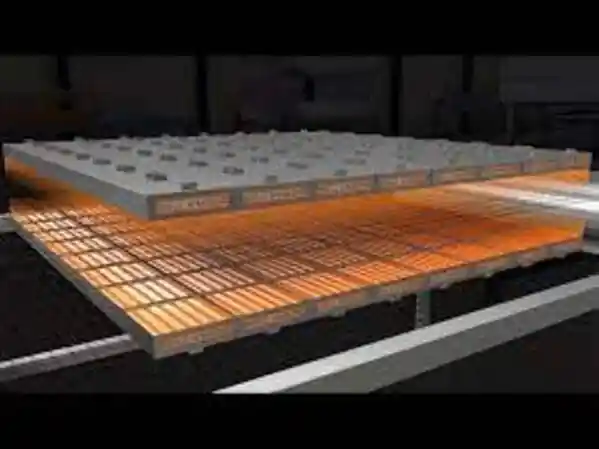
Infrared heating dominates heavy-gauge work for three reasons. It is non-contact, so nothing marks the sheet surface. It transfers energy quickly, which keeps cycle times reasonable on thick stock. And it divides naturally into zones: a modern oven is a grid of independently controlled ceramic or quartz elements, each with its own setpoint, so the operator can put more energy where the mould draws deepest and less where the sheet merely needs to stay hot.
Wavelength matters. Medium- and long-wave emitters put out energy at wavelengths that common thermoforming plastics absorb well, while shorter-wave emitters behave differently and suit clear or thin materials. Sheet colour shifts absorption too: a black ABS sheet soaks up radiant energy noticeably faster than a natural or light-grey one, so the same part in two colours may need two heating recipes rather than one. A heater recipe is therefore part of part qualification, not a background setting.
Zone control is where heating becomes engineering. Typical practice divides the oven into dozens of zones, maps the sag profile of a test sheet, and trims each zone until the sheet softens evenly across its full width and length. The SPE Thermoforming Division publishes practical guidance on heater selection and oven zoning that matches this zone-mapping approach. For the setpoint, ramp and dwell detail behind that practice, our infrared heating and control article walks through the discipline step by step.
ZetarVac processes sheet from 0.5 to 15 mm thick with forming lengths up to about 2,500 mm. A range that wide means one heating recipe can never cover the shop: each material and gauge gets its own through-heating window, qualified before production rather than assumed.
When heater zones drift, the sheet shows it immediately. A hot band over one area produces localized sag, and that over-soft region stretches first in the forming step, ending up as a thin wall or a web in the finished part. Cold zones do the opposite: they leave stiff islands that resist drawing, bridge over deep features or tear during forming.
"One heater temperature setting will treat every sheet thickness the same way."False
A 15 mm sheet needs several times the soak of a 0.5 mm sheet, and thick stock can reach surface temperature while its core is still cold and stiff. Forming from that state produces thin walls, spring-back and warped panels, so one global setpoint cannot serve the full gauge range.
"Heater zones are set per material and gauge, then qualified on a first-article sheet."True
That is standard heavy-gauge practice. Each combination of material, colour and thickness gets a zone map verified against measured sheet temperature and sag before the recipe is released for production runs.
Contact and Convection Heating: Where Each Fits
Contact heating presses the sheet against, or just above, a heated plate and transfers heat by conduction. Because the plate is uniformly heated, it delivers very even surface temperature without radiant overshoot. The trade-offs are speed and geometry: conduction into thick plastic is slow, and the method suits flat or gently curved panels far better than deep draws. It earns its place on thick, flat or finish-critical work where radiant scorch must be ruled out.
Convection heating circulates hot air around the sheet in an enclosed oven. It is gentle, tolerant of awkward colours and textures, and it cannot blister a surface the way an oversized radiant zone can. But air is a poor heat carrier compared with radiation at thermoforming temperatures, so convection alone is slow for heavy-gauge stock. Its most useful role is as a preheat stage ahead of the infrared station: the oven lifts the sheet partway to forming temperature, then the radiant banks finish with precise zone control.
Choosing between them comes down to the part. If the sheet is flat, thick and finish-sensitive, contact or convection-assisted heating reduces risk. If the part is a deep-drawn enclosure or tray with varying section depths, zoned infrared remains the practical default, because only zoning can put energy exactly where the draw needs it.
How Do You Heat Thick Sheet Evenly?
Even through-heating of thick sheet rests on three measures: heating from both sides with top and bottom heater banks, staging the heat so the core has time to soak, and verifying readiness with direct temperature measurement rather than a stopwatch. As a working rule, heating time grows roughly with the square of sheet thickness, so a 15 mm sheet needs far more soak than a 0.5 mm sheet on the same oven, with exact values depending on material, colour and heater power.
Sag is the first visual signal to watch for during heating1. As the sheet softens it drapes downward under gravity, and an even sag profile across the whole width indicates balanced heating. But sag only reflects the surface and the average; it cannot prove the core is hot. That is why heavy-gauge shops add instrumentation. Fixed or handheld IR pyrometers read surface temperature zone by zone2, and a needle thermocouple pressed into a sacrificial corner of the sheet confirms what the core is actually doing.
Materials data helps set the window. The Vicat softening temperature3 gives a useful upper reference: ISO 306 defines it as the temperature at which a flat indenter penetrates the plastic under a specified load, and heating stations treat it as a ceiling to avoid, because past it the sheet loses melt strength and sags uncontrollably. Working setpoints sit in a qualified band between soft-enough-to-form and too-soft-to-handle.
ZetarVac runs 20+ vacuum forming and thermoforming machines with a reference monthly capacity of about 100,000–200,000 pieces across 45+ production lines. Volume like that only works when heating recipes are repeatable, which is why every material-and-gauge combination is qualified with measured temperatures before it enters batch production.
The order of checks matters: screen with sag, verify with measurement, then freeze the recipe. Shops that skip the middle step quietly build warpage into every part at volume, and it only surfaces after trimming and cooling.
"If the sheet sags evenly across its width, the core must be at forming temperature."False
Sag tracks the surface and the average sheet temperature, not the core. On thick stock the core can lag far behind the faces, and forming from that state locks stress into the part that releases as warp after trimming. Only a probe or calibrated pyrometer routine closes that gap.
"Heating readiness is confirmed by measurement, with sag used only as a screening signal."True
Correct. Sag tells the operator when to start looking; a thermocouple or pyrometer check against the qualified recipe tells them when the sheet is actually ready to form.

Which Heating Method Fits Your Material and Part?
The default for most heavy-gauge work is zoned infrared, because it handles thickness, colour and deep draws in one station. Add convection preheat when the sheet is very thick or radiantly sensitive, and keep contact heating for flat, finish-critical panels. The decisive variables are sheet thickness, colour, absorption behaviour and the surface quality the part must carry.
The material adds its own constraints. The table below summarizes how commonly formed materials behave in the heating stage, based on the grades ZetarVac processes regularly.
| Material | Heating behaviour | Watch-out during heating | Typical formed use |
|---|---|---|---|
| PVC | Wide, forgiving softening window | Discolouration if overheated | Trays, packaging, industrial enclosures, liners |
| ABS | Even absorption, stable sag profile | Gloss change near the upper limit | Equipment housings, cases, guards |
| HDPE | Fast, coarse sag response | Shrinkage and sheet droop | Industrial trays, equipment liners, storage boxes |
| PP | Narrow sag window | Cold corners pull thin in the draw | Automotive interior parts, trays, boxes |
| PC | High forming temperature | Sheet must be dried before heating | Clear guards, equipment protection covers |
| PMMA | High clarity, marks easily | Dust or heater marking shows through | Clear covers, luminaires, display parts |
Clear acrylic deserves special care, because every marking picked up in the oven shows in the finished cover; our acrylic thermoforming article covers that material in detail.
Heating Faults and How to Catch Them
Most heavy-gauge forming defects root in the heating stage, which makes it the cheapest place to fix them. The common failure modes:
- Cold core: the surface is at temperature but the centre is stiff. It shows up as thin walls in deep draws, heavy spring-back and warp after trimming. Catch it with core-temperature probes during recipe qualification.
- Overheated surface: blisters, scorch marks, gloss change or streaks above hot zones. Catch it by mapping surface temperature and inspecting the heated sheet before forming.
- Uneven zones: localized sag bands. Formed parts show webs, thin patches or tearing exactly where the sheet was hottest. Catch it with sag profile mapping against the qualified recipe.
- Residual stress: a sheet heated unevenly and formed quickly locks stress into the part, which releases later as warp. Catch it by checking flatness after trimming, not just at the press.
Two laboratory properties anchor the specification side. ASTM D648 is the standard test for heat deflection temperature under flexural load4, and it is the figure buyers use to confirm that a formed panel or enclosure keeps its shape at service temperature — a property that starts with heating the sheet correctly rather than past its limit. For formed electrical housings, UL 94 classifies the flammability of plastic materials, and many formed enclosures must use a resin grade meeting a specified UL 94 class; degrading that resin through overheating can compromise the rating the part was specified to carry.
"A part that looks right at the press will stay dimensionally stable in service."False
Formed parts carry residual stress from uneven through-heating, and that stress relaxes over time or under heat, warping the part weeks after it passed inspection. Heating discipline and post-trim flatness checks protect the shipped part, not a visual check at the machine.
"Flatness is re-checked after trimming and cooling, not only at the forming press."True
Yes. Residual stress from the heating stage shows up as warp once the part cools and is trimmed, so heavy-gauge practice verifies flatness on trimmed parts before release.
When you compare suppliers for heavy-gauge forming work, ask specifically how heating recipes are qualified and re-verified per material; our page on choosing a vacuum forming manufacturer in China lists the capability questions worth putting to any candidate.
FAQ
How long does it take to heat a sheet in heavy-gauge vacuum forming?
There is no single number: heating time depends on sheet thickness, material, colour and heater power. A thin ABS sheet may reach forming temperature in well under a minute under strong two-sided radiant heat, while the thickest 15 mm stock of the same material typically needs several minutes of staged soak. Treat published figures as starting points and qualify the actual recipe with measured temperatures.
Can you overheat thermoforming sheet?
Yes, and the damage is not always visible. Past the upper limit a sheet blisters, scorches or loses gloss; even below visible damage, overheating degrades the polymer and weakens the finished part. Heating setpoints are therefore specified as windows, not single targets, and qualified per material and gauge.
Why does my sheet sag unevenly during heating?
Uneven sag almost always traces to unbalanced heater zones, gauge variation within the sheet, or different colours on a patterned sheet absorbing energy at different rates. Map the sag profile, compare it with the qualified recipe, and trim zone setpoints before touching anything downstream.
Does sheet colour change the heating recipe?
It does. Dark surfaces absorb radiant energy faster than light ones, so a black sheet usually needs lower intensity or shorter exposure than a light-grey sheet of the same material and thickness. Multi-colour or patterned sheets are the hardest case and deserve their own qualification run.
To keep digging into the process after the heating stage, explore our vacuum forming guide, which walks through mould design, forming techniques and trimming in the same engineering detail.
-
Sheet sag: The downward draping of a heated thermoforming sheet under gravity, used as a visual screening indicator of softening and heating balance. ↩
-
IR pyrometer: A non-contact infrared thermometer used to read sheet surface temperature zone by zone in a thermoforming heating station. ↩
-
Vicat softening temperature (ISO 306): ISO 306 defines the temperature at which a flat-ended indenter penetrates a plastic specimen under a specified load, marking where the material begins to soften. ↩
-
HDT (ASTM D648): Heat deflection temperature, the temperature at which a standard test bar deflects a specified amount under flexural load, used to judge stiffness of formed panels at service temperature. ↩


