Most buyers arrive at thermoforming with a part sketch and one question: will this process work for my application? The answer depends on part size, wall thickness, annual volume, and the environment the part must survive. This article maps the applications where vacuum formed parts are the default choice, explains the material logic behind each family, and lists the acceptance checks a buyer should expect before approving first articles.
- Vacuum formed parts dominate five application families: equipment housings, medical and diagnostic enclosures, trays and packaging, automotive components, and agricultural or display parts.
- Heavy gauge thermoforming processes sheet from 0.5 mm to 15 mm and forms parts up to about 2,500 mm long in a single piece.
- ABS, PC, HDPE, PVC, and PP cover most applications; ASA and PMMA extend the process to outdoor weathering and optical clarity.
- Acceptance rests on standard tests: tensile per ASTM D638 or ISO 527-2, flexural and heat checks per ASTM D790 and ISO 75-2, flammability per UL 94.
- 5-axis CNC trimming is what converts a formed shell into a finished part with accurate cut-outs and mounting holes.
What Are the Most Common Applications for Vacuum Formed Parts?
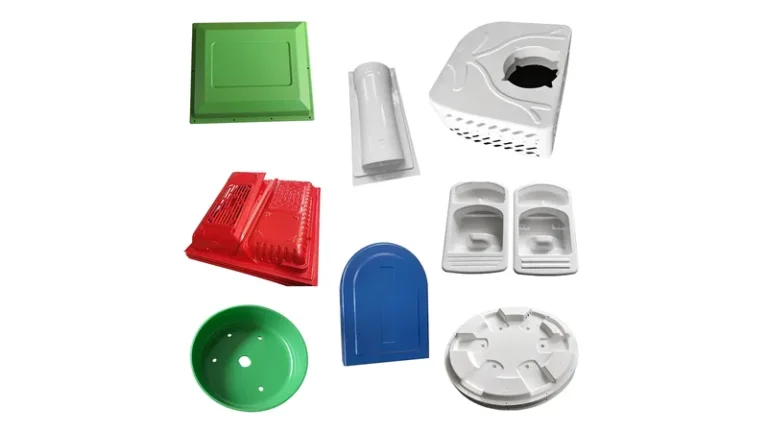
Vacuum formed parts are most common in five families: equipment housings and machine covers, medical and diagnostic equipment enclosures, heavy gauge trays and material-handling packaging, automotive interior and exterior components, and agricultural or retail display parts. The process wins these jobs because it converts 0.5–15 mm sheet into large, thin-walled, three-dimensional shapes at tooling cost well below comparable molding routes.
Each family shares three engineering characteristics. The parts are big: machine guards, equipment covers, and liners routinely exceed 500 mm in one dimension, which makes machining them from solid stock impractical. The walls are thin relative to the footprint — typically 1–8 mm of formed sheet — so high packing pressure is not required. And volumes are moderate: anywhere from a few dozen prototypes to tens of thousands of units per year.
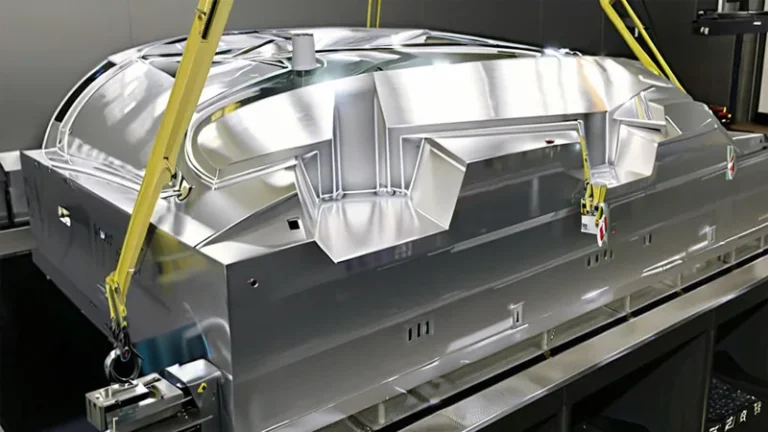
That volume window matters more than any single property. Vacuum forming tooling is usually a single-sided mold, which keeps upfront cost low and makes design revisions cheap. When a buyer needs 200 enclosures this year and expects the geometry to change twice, forming is often the only route that stays economical. For the workflow behind these parts, see the vacuum forming process overview.
It is just as useful to know where forming is the wrong answer. Small, dense, tight-tolerance parts produced in the tens of thousands per year, or parts that need uniform wall thickness in every direction, generally justify a matched-mold process instead. Formed parts carry inherent wall variation from the draw, and pretending otherwise at the quotation stage is how projects end up renegotiating tolerances after first articles arrive.
Equipment Housings and Machine Enclosures
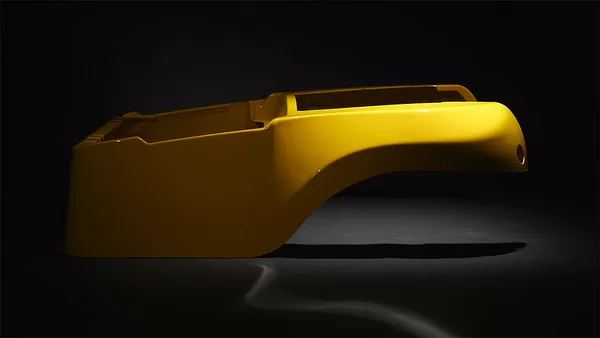
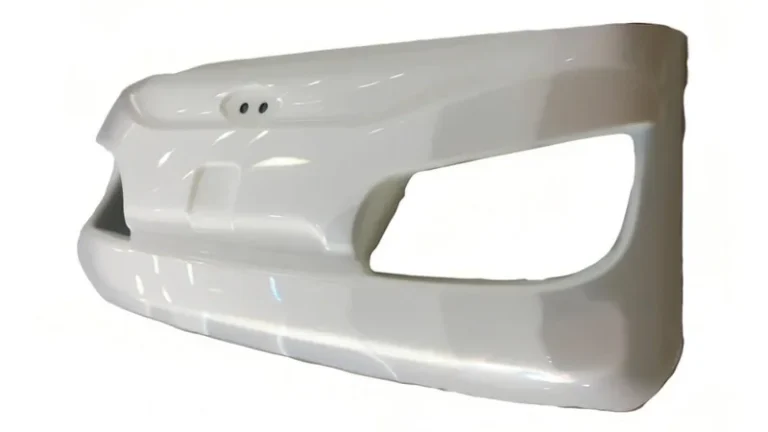
Equipment housings are the flagship application for heavy gauge1 forming. A typical machine cover is a shell with a flat mounting flange, cut-outs for displays and connectors, and a wall gauge between 3 and 8 mm. ABS is the workhorse because it forms cleanly, carries sheet texture through to the finished surface, and is available in flame-rated grades. Where impact or service temperature rises, PC and PC/ABS take over; where the enclosure lives outdoors, ASA resists UV far better than most alternatives.
Design details decide whether the housing trims cleanly. Draft angles of roughly 2–5 degrees on vertical walls, generous radii at the flange, and a shrinkage allowance matched to the material keep the shell predictable after cooling. Where finer surface detail or sharper texture definition is needed, pressure forming adds air pressure on top of the vacuum. A drawing that ignores draft and radii asks the toolmaker to fight physics, and the excess usually shows up as warped flanges or out-of-tolerance mounting holes.
Electrical enclosures carry additional obligations. UL 94 classifies the flammability of plastic materials, and many formed equipment housings must specify a grade such as V-0 or HB before the finished machine can pass its own certification2. Ingress protection is handled separately: IEC 60529 defines the IP code that grades how well an enclosure excludes dust and water, so an outdoor formed cover is gasketed and tested against a stated IP target3. Medical and diagnostic equipment enclosures follow the same pattern but add impact resistance, which usually pushes the material choice toward PC.
"Vacuum formed housings are inherently flimsy compared with molded ones."False
A formed shell of 4–8 mm ABS or PC carries ample stiffness for a guard or cover, and flanges, ribs, and bonded internal frames raise rigidity further. The genuine risk is not weak material but wall thinning on deep draws, which is controlled through heating strategy and plug assistance.
"Forming is the economical route for large enclosures at low-to-mid volumes."True
Tooling for a 1,500 mm housing is a single-sided mold costing a fraction of a paired mold set. From prototyping through batches of a few thousand units, per-part economics usually favor forming, especially while the design is still evolving.
One limitation deserves honesty before the conversation moves to materials. Deep draws thin the sheet unevenly, so the engineer should ask for a wall thickness prediction on the deepest corners rather than a single gauge number on the drawing. Shops that quote one uniform gauge for a deep shell are promising something the process cannot deliver.
ZetarVac forms sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm, and trims formed parts on a 5-axis CNC centre. For a housing project, that means a single shell can span most machine covers without splitting into joined sections, and the trimmed outline follows the forming tool rather than a secondary fixture.
Trays, Packaging, and Material Handling
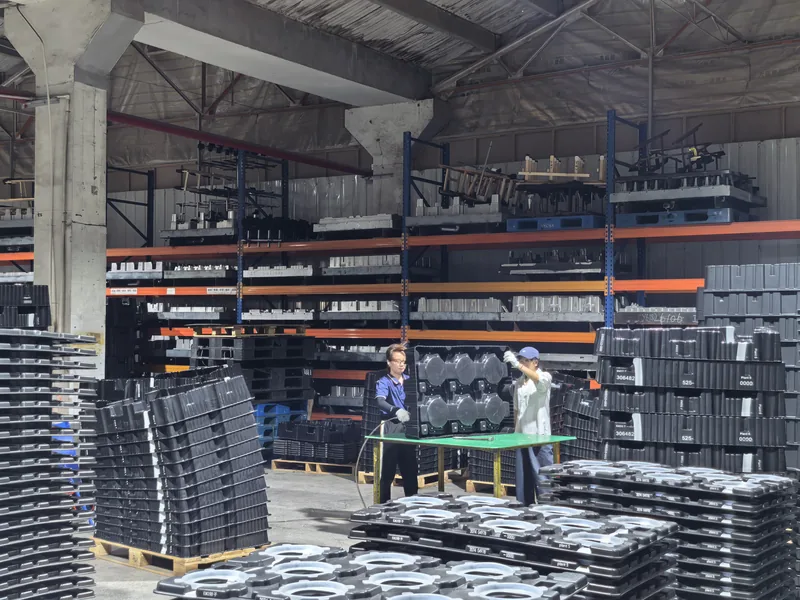
Trays are the volume leader in vacuum forming. Heavy gauge trays cover dunnage, in-process handling, shipping packaging, and equipment liners, with gauges typically between 1 and 6 mm and multi-cavity layouts that locate parts precisely for assembly lines. PVC serves general packaging and industrial liners; HDPE brings chemical resistance to equipment liners and storage boxes; PP handles trays that see elevated wash temperatures.
Food-adjacent packaging adds a compliance layer. EU 10/2011 regulates plastic materials and articles intended to come into contact with food, so any thermoformed tray or packaging part that touches food must be made from a compliant material and documented accordingly. Industrial packaging avoids that clause but keeps its own verification: stacking load, drop behavior, and edge stiffness on the tray flanges.
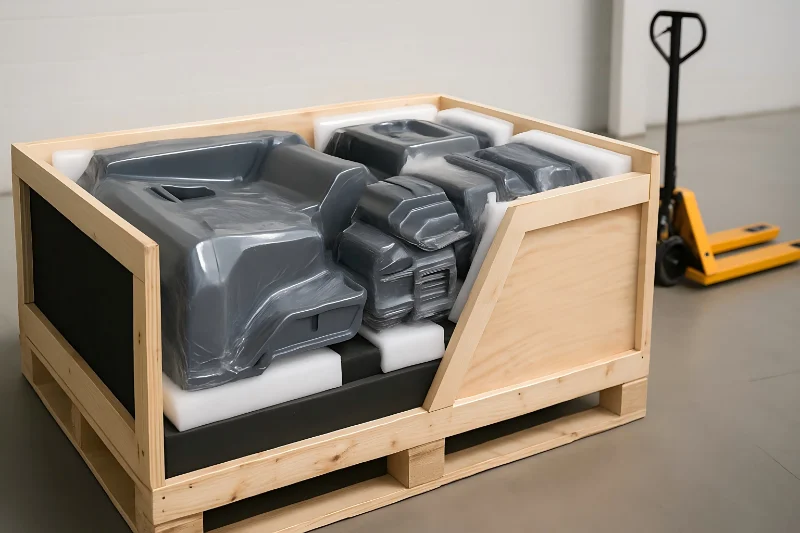
ZetarVac runs more than 20 vacuum forming and thermoforming machines across 45+ production lines, with reference monthly capacity of roughly 100,000–200,000 pieces. For a packaging program that mixes prototype trays with seasonal volume peaks, that machine spread keeps both stages inside one process qualification.
Automotive, Agricultural, and Display Components
Automotive applications use forming where surfaces are large and volumes are moderate: interior trim covers and carriers in ABS and PC/ABS, soft parts in TPV, structural brackets in PP/GF, and exterior trim in ASA. Heat resistance is screened early through heat deflection temperature4, because cabin and under-hood zones routinely cycle well above room temperature. Grained sheet supplies the surface finish directly, which removes a secondary texturing operation from the cost stack.
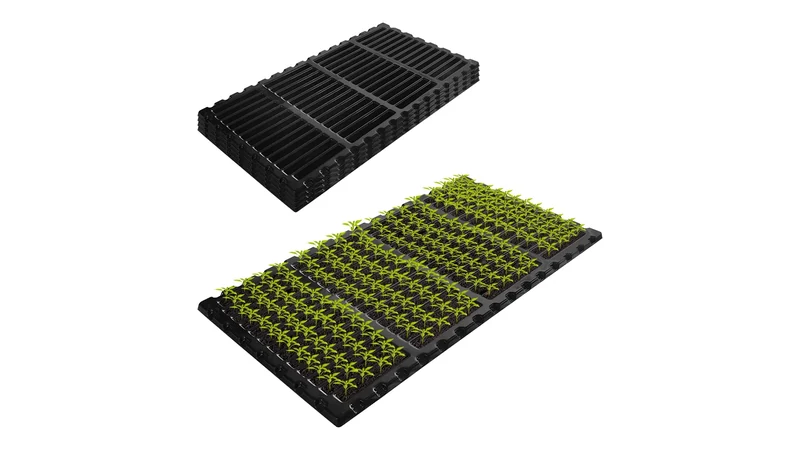
Agriculture is quieter but demanding. A multi-cavity ABS seedling tray must survive seed contact, irrigation water, UV exposure, and thousands of handling cycles, with cell geometry tuned to the crop and the seeding machine. Machine liners and storage boxes in HDPE take the abrasion and chemical splash that field equipment generates season after season.
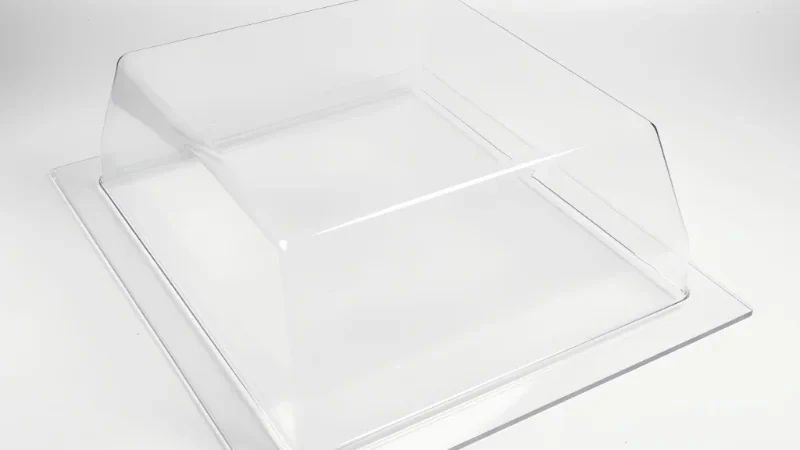
Retail display leans on PMMA. A clear cover over a display unit needs optical clarity, custom curvature, and stable edges after trimming — a combination forming delivers without the joint lines and distortion risk of glued flat panels. The same logic extends to luminaires and protective covers where the part is meant to be seen through, not just seen.
Which Material and Process Choices Fit Each Application?
Start from the environment, not the datasheet. Outdoor parts point to ASA or PMMA; impact-prone guards point to PC or PC/ABS; food or chemical contact points to HDPE, PP, or compliant PVC; structural load paths justify PP/GF; and transparent covers point to PMMA. The material then sets the forming window, the trim method, and the test plan — which is why material selection is the first engineering decision, not the last.
| Application family | Typical materials | Why forming fits | Key watch-outs |
|---|---|---|---|
| Equipment housings | ABS, PC/ABS, ASA | Large single shells, low tooling cost, flame-rated grades | Wall thinning on deep draws; flammability rating |
| Medical enclosures | PC, ABS | Impact resistance, large curved surfaces, custom cut-outs | Stress whitening at trimmed edges |
| Trays and packaging | PVC, HDPE, PP | Multi-cavity geometry, 1–6 mm gauge, chemical resistance | Food contact requires compliant material |
| Automotive parts | PP, PP/GF, TPV, PC/ABS | Heat deflection, grained sheet finish, moderate volumes | Sag control during heating; thermal expansion |
| Agricultural and display | ABS, HDPE, PMMA | UV-stable or transparent options, large flat areas | Outdoor weathering; scratch resistance on clear parts |
Process execution separates a good part from a rejected one. Every polymer has its own forming window: PC heats high and sags quickly, PP has a narrow window and strong memory, PMMA needs careful thermal control to stay optically clean. Pushing one heating profile across all of them produces thin corners, webbing, or bubbles in vacuum formed products. Surface character comes mainly from the sheet itself, and the options are compared in this guide to finishes for vacuum formed parts.
"Any plastic sheet can be vacuum formed with one universal recipe."False
Each polymer has its own heating window, sag behavior, and shrinkage memory, so a profile tuned for ABS will distort PP or haze PMMA. Shops that ignore this produce thin corners, bubbles, and warped flanges that fail dimensional checks.
"Material selection should start from the application environment."True
UV exposure, impact, temperature, chemical contact, and flammability requirements eliminate most grades before cost is even discussed. Specifying ASA for an outdoor cover or PC for a machine guard up front prevents an expensive requalification cycle later.
How Are Formed Parts Tested and Accepted?
Formed parts are accepted on the same plastic test standards as any other molding process, applied to both the incoming sheet and the finished part. Tensile properties are verified per ASTM D638 or ISO 527-2, stiffness and heat resistance per ASTM D790 and ISO 75-2 or ASTM D648, flammability per UL 94, and enclosure protection per IEC 60529 or NEMA 250.
ASTM D638 measures the tensile properties of plastics, and it is the standard tensile test run on thermoformed sheet and on coupons cut from the formed regions where thinning is expected5. Wall thickness mapping matters more than any single lab number: a shell that gauges 4 mm on the flange may thin to 1.5 mm over a deep corner, and that map decides whether the part survives impact or vibration in service. Trim accuracy is checked against the drawing on a fixture, and clear parts are judged on transmittance and visible distortion under light.
ZetarVac supports prototyping, small batch, and large batch production on the same machine base, so a first-article approval built on these tests carries into volume runs. That continuity matters when a medical or industrial enclosure cannot be requalified every time the batch size changes.
FAQ
What sheet thickness counts as heavy gauge thermoforming?
Heavy gauge generally means sheet roughly 1.5 mm and thicker, where the formed part is structural rather than a thin packaging skin. ZetarVac processes sheet from 0.5 to 15 mm, which spans thin-wall packaging parts through PA6, POM, and PP/GF industrial structural components.
How large can a single vacuum formed part be?
ZetarVac forms parts up to about 2,500 mm in length. At that scale the process is usually chosen precisely because joining smaller pieces would add seams, misalignment, and assembly cost to a housing or cover.
Can formed parts include cut-outs, holes, and mounting features?
Yes. Forming creates the three-dimensional shell; 5-axis CNC trimming then cuts the outline, display windows, connector openings, and mounting holes directly against the geometry the tool produced. Reinforcement ribs and bosses can be added as bonded or fastened secondary features where local stiffness is needed.
Which material should I choose for an outdoor enclosure?
Start with ASA or a UV-stable PMMA for the shell, and PC if impact resistance matters more than long-term weathering. Gasketing and an IP target from IEC 60529 should be on the drawing from day one, not added after a field failure.
Does vacuum forming work for food-contact trays?
Yes, provided the selected material complies with EU 10/2011 for food contact and the compliance documentation travels with the material lot. HDPE and PP are the usual starting points for washable or reusable food-adjacent trays, with PVC reserved for compliant single-use packaging.
To keep digging into the process itself, explore the vacuum forming hub, or review how a China-based vacuum forming manufacturer takes applications like these from prototype through batch production.
-
Heavy gauge: Heavy gauge thermoforming refers to forming plastic sheet roughly 1.5 mm and thicker into structural parts, as opposed to thin-gauge packaging film. ↩
-
UL 94: UL 94 is the standard for flammability of plastic materials, grading specimens from HB up to V-0 and 5VA by burning and afterflame behavior. ↩
-
IP code: The IP code defined in IEC 60529 classifies the degrees of protection an enclosure provides against dust, objects, and water ingress. ↩
-
HDT: Heat deflection temperature is the temperature at which a plastic specimen deflects a specified amount under a defined flexural load, per ISO 75-2 or ASTM D648. ↩
-
ASTM D638: ASTM D638 is the standard tensile test for plastics, measuring tensile strength, elongation, and modulus on standardized specimens. ↩