
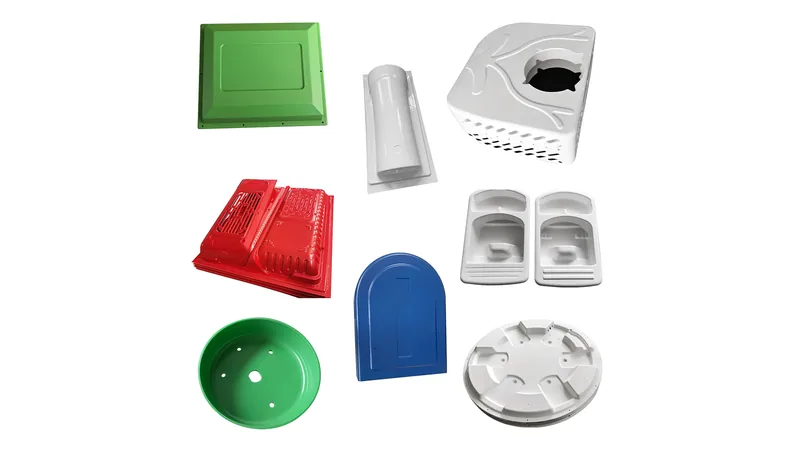
Sustainability requests usually reach the engineering desk as a blunt instruction: use less material, use less energy, and make the part recyclable at end of life. For large plastic parts — equipment housings, machine covers, logistics trays, agricultural panels — vacuum forming is one of the few forming routes where all three can be addressed without rebuilding the business case around tooling cost. The environmental argument for thermoforming is not marketing gloss. It rests on measurable quantities: sheet yield, forming temperature, regrind loops, and validated wall thickness. This article walks through where the advantages are real, where they depend on design discipline, and which checks a buyer should run before accepting a “greener” claim from any supplier.
- A thermoformed part consumes only the sheet area it actually draws; the remaining trim stays clean, single-polymer, and reusable as regrind.
- Forming happens below the melting point of the resin, so energy per kilogram of finished part is lower than in processes that fully melt and inject material.
- Down-gauging — running a thinner sheet and adding ribs — cuts resin use, but only when stiffness is re-validated with standard tensile and flexural tests.
- Single-polymer choices such as HDPE, PP, and ABS simplify recycling; multi-layer sheets, paint, and bonded liners can block it.
- Food-contact recycled content is controlled by EU Regulation 10/2011, not by supplier preference.
- Honest trade-offs exist: deep draws thin the sheet unevenly, and appearance surfaces limit how much regrind can be blended in.
What Makes Thermoforming a Lower-Waste Process?
The core advantage is that vacuum forming shapes a heated sheet against a single mold using vacuum or air pressure, without melting the resin into a liquid. Because the material is only softened, the energy input per kilogram is lower, and every offcut remains a clean piece of one polymer that can be reground and fed back into production.
The forming window is the heart of the argument. Sheet is heated to a softened state — commonly in the 120–180 °C range for ABS or HDPE, depending on grade, gauge, and heater power — and then drawn onto the mold by vacuum. No screw plasticizes the resin, no runner is discarded, and no high-pressure injection wastes energy on packing. The energy budget is dominated by infrared heaters and the vacuum pump, which scale with sheet area rather than part volume. On a life-cycle basis that difference shows up directly in kilowatt-hours per kilogram of finished part, before logistics and end-of-life effects are even counted.
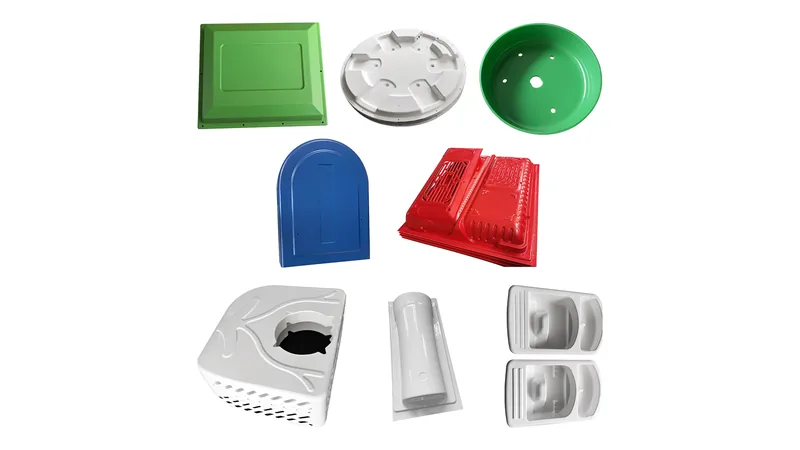
Scrap generation is equally visible. A formed part produces two categories of offcut: the trim frame around the pocket and the web between multiple cavities. Both are the same polymer as the part, never fully melted, and both leave the trim station in predictable shapes that are easy to collect and reprocess1.
Does Vacuum Forming Really Use Less Energy Than Injection Molding?
For large, thin-walled parts, usually yes. Thermoforming heats only the sheet to a forming temperature well below full melt, while injection molding plasticizes the entire shot at high pressure and discards runners. The honest comparison still depends on cycle time, trim ratio, and part thickness, so the saving is largest on big parts with moderate draw depth.
The per-part arithmetic explains why. A machine cover formed from 4 mm ABS sheet needs one heater pass of a few minutes and modest clamping force; the same geometry injection molded would require a machine with far higher tonnage, a steel mold with cooling channels, and a longer cycle to pack and freeze a thick-walled part. For heavy-gauge parts above roughly half a meter, the forming route typically wins on both tooling energy and machine energy. Below that size, or at very high volumes with thin walls, the balance can shift — which is why the claim should be checked against a specific part, not asserted in general.
ZetarVac processes sheet from 0.5 to 15 mm on more than 20 vacuum forming and thermoforming machines, with formed lengths up to about 2,500 mm and 5-axis CNC trimming of formed parts. For a sustainability program that range matters: one line can carry a part from thin packaging sheet to heavy structural covers, and CNC trimming keeps the final outline accurate so the part — not the scrap bin — defines the delivered geometry.
The SPE Thermoforming Division publishes process guidance on sheet heating and energy practice, and it is a useful independent reference when a supplier’s energy claim needs a sanity check.
Where Does the Material Actually Go: Sheet Yield, Trim, and Regrind
Start with the yield calculation, because it decides everything downstream. If a tray draws 70 percent of the sheet area into the part, the remaining 30 percent is trim. That trim ratio is not waste in the accounting sense; it is unpaid material waiting to be reclassified. How much of it you can actually reuse depends on the draw ratio2 — deeper parts thin the sheet more, and heavily stretched zones may not tolerate regrind blended in, because recycled resin has slightly lower melt strength and can tear at extreme elongation.
"Thermoforming throws away most of the sheet it starts with."False
Trim looks like waste only when no recovery system exists. The offcut is clean, single-polymer, and un-degraded, so it can be regranulated and blended back into new sheet for many part families. Shops without a regrind loop lose that value; shops with one rarely do.
"Trim becomes a closed regrind loop for the right part families."True
Industrial trays, liners, and covers in HDPE, PP, or ABS can run controlled regrind percentages after granulation and screening. Appearance-critical and food-contact surfaces stay on virgin sheet, which is why the loop needs a written material policy rather than an informal habit.
A regrind policy has three engineering controls: the blend percentage, usually kept in a conservative band for non-appearance parts; the screening step that removes contamination and over-fine granulate; and a traceability record linking each batch to its blend ratio. Without those controls, recycled content is a slogan. With them, it is a reproducible material specification that an auditor can follow.
ZetarVac runs 45+ production lines across the plant, with reference monthly capacity of about 100,000–200,000 pieces and support for prototyping, small batch, and large batch production. For material-efficiency work this matters directly: down-gauging and regrind validation are iterative trials, and a supplier that can run short prototype batches lets you test a thinner sheet or a regrind blend before committing volume.
Can Recycled Content Go Into a Formed Part?
Yes for most industrial and non-food parts, within limits. Regrind from the same polymer — post-industrial trim — is the easiest route because the material history is fully known. Post-consumer resin3 is possible for robust industrial parts but introduces variability in melt flow and color, so it belongs in non-critical geometries until supplier qualification proves otherwise.
Food contact changes the answer completely. EU Regulation 10/2011 governs plastic materials and articles intended to come into contact with food, and it defines the compliance path that decides whether any recycled content may enter a thermoformed food tray; recycled material must clear that regulation, not just a supplier’s internal test. In practice, most food-contact thermoformed packaging runs virgin sheet, with environmental gains pursued through down-gauging and lightweighting instead.
There is also a durability argument that buyers sometimes miss. A PC guard or PMMA display cover that lasts ten years in service displaces more material than a short-lived part replaced twice — the most sustainable kilogram is the one you never have to mold again. Heat resistance matters here as well: parts near motors or lamps should be checked against the heat deflection temperature4 of the chosen grade before a lighter, thinner version is approved.
Which Design Choices Cut Material Without Cutting Performance?
Ribbing, corner radii, and flange design do more for material efficiency than any procurement negotiation. A flat panel and a ribbed panel of the same resin can show similar stiffness at noticeably different gauges, because formed ribs add height exactly where the section needs it. The saving is only real when the new design is re-tested, and the standard check is defined: ISO 527-2 specifies the tensile test method for plastics and is the test that confirms a down-gauged thermoformed sheet still carries its design loads.
"A thinner sheet always means a weaker finished part."False
Thickness is only one stiffness variable. Rib height, radius, and flange width routinely restore rigidity at lower total weight, and formed ribs come nearly free from the mold geometry. The claim fails mainly when nobody re-tests stiffness after the gauge change.
"Down-gauging is safe only with re-validated mechanical data."True
A tensile check on the new gauge, plus a flexural stiffness comparison against the original part, tells you whether the ribbed design carries load. Run that sequence and thinner sheet becomes an engineering decision with evidence behind it, not a gamble.
Material choice sets the ceiling for everything above. The table below compares the common heavy-gauge sheet materials on regrind and recycling behavior:
| Material | Regrind compatibility | Typical formed applications | Environmental note |
|---|---|---|---|
| HDPE | Excellent in closed loops | Industrial trays, equipment liners, storage boxes | Widely recyclable; single polymer simplifies recovery |
| PP | Excellent | Automotive interiors, trays, packaging, boxes | Low density reduces shipping mass per part |
| ABS | Good for non-appearance parts | Equipment housings, cases, guards | Strong and dimensionally stable; regrind kept off visible surfaces |
| PC | Limited | Clear guards, protection covers | High durability extends service life; clarity needs virgin sheet |
| PMMA | Limited | Clear covers, display parts | Long service life offsets a higher material footprint |
When packaging is the target, the same logic applies at thinner gauges, and the thermoformed packaging overview covers the material and design options in detail.
What Trade-Offs Should You Verify Before Claiming the Green Win?
Deep draws thin the sheet unevenly. A part formed over a tall, narrow core can end up with corner walls at half the original gauge, which means the nominal sheet thickness overstates the strength of exactly the zones that matter. Ask for wall-thickness measurements at the corners and the floor, not just at the flange.
Appearance surfaces limit regrind. Any part with a visible texture, gloss requirement, or clear geometry will usually stay on virgin sheet, because regrind introduces color drift and optical defects. That is not a failure of the sustainability case; it simply means the recycled content claim belongs on the structural and non-visible part families where it is honest.
Finally, ask how the environmental claim will be measured. A full life-cycle assessment5 is the only method that captures heating energy, trim recovery, transport weight, and end-of-life together, and it is worth commissioning when a large program depends on the number. For everyday sourcing decisions, a structured comparison of sheet yield, regrind percentage, and validated gauge is usually enough to separate real savings from claims that will not survive an audit.
A representative agricultural case shows the lightweighting path end to end: an ABS seedling tray produced by heavy-gauge thermoforming, with a multi-cavity layout and custom cell geometry. Because cavity count, cell size, and tray dimensions are all tool-driven, the tray can be redesigned to cut resin per cell while keeping the stiffness that seedling handling and machine transfer require.
FAQ
Is vacuum forming more sustainable than injection molding for large parts?
Generally yes for large, thin-walled parts, because the process heats only the sheet to forming temperature and produces no runners. Injection molding regains ground on small, thick, high-volume components. Compare on a per-part basis using sheet yield and cycle energy.
Can thermoformed products be recycled at end of life?
Single-polymer parts in HDPE, PP, or ABS are straightforward candidates for mechanical recycling, especially industrial trays, covers, and liners. Multi-material assemblies with bonded foam, paint, or mixed polymers are harder and often end up in energy recovery instead.
How much recycled content can a formed part contain?
Non-appearance industrial parts can often run a meaningful regrind blend once the percentage is qualified. Food-contact and clear parts generally stay on virgin material, and food applications must satisfy EU 10/2011 before any recycled content is permitted.
Does heavy-gauge thermoforming support lightweight packaging and trays?
Yes. Gauge, cavity geometry, and flange design are all adjustable in the tool, so tray weight can be reduced step by step and verified with stiffness testing. The thermoforming packaging application guide walks through these options by market.
Which material should I choose for a recyclable enclosure or tray?
Start with HDPE or PP when recyclability leads the requirement list, ABS when stiffness and surface quality lead, and PC or PMMA when clarity and durability do. To compare how these materials behave on a real forming line, the China vacuum forming manufacturer overview explains the material-to-process mapping in practice.
To keep digging into the process behind these decisions, explore the vacuum forming capability overview or review how heavy-gauge projects are structured from sheet selection through trimming — both walk through the engineering details in more depth.
-
Regrind: production trim and scrap reprocessed into granules that can be blended back into new sheet at a controlled percentage. ↩
-
Draw ratio: the ratio of formed part surface area to the original sheet area that forms it; higher draw ratios stretch the sheet thinner. ↩
-
PCR: post-consumer recycled resin recovered from used products, with more variable properties than post-industrial regrind. ↩
-
HDT: heat deflection temperature, the temperature at which a plastic specimen deflects a set amount under a defined flexural load. ↩
-
LCA: life cycle assessment, a standardized method for quantifying the environmental impact of a product across its whole life. ↩



