

Production time in heavy-gauge thermoforming is decided long before the sheet reaches the heater. Tool design choices, material selection, and the order in which engineering tasks run determine most of the calendar. This guide breaks down where the days actually go in vacuum forming thick sheet, which levers shorten each phase, and how to compress a schedule without trading away part quality.
- Total thermoforming lead time splits into tooling, sheet preparation, forming cycles, and trimming; attacking only the press cycle leaves most of the schedule untouched.
- Heating and cooling dominate cycle time and scale with sheet thickness, so material and gauge choices are schedule decisions, not only performance decisions.
- The fastest stable cycle forms at the lowest sheet temperature that still fills the tool detail, not at maximum heater power.
- Tool building, trimming programs, and sheet logistics can run in parallel; sequential task planning is the largest avoidable delay in a forming program.
- First-article approval is not proof of cycle stability; verify output over a continuous run before committing a delivery date.
- Agree the validation plan — stiffness, heat deflection, flammability — before production starts so testing never becomes a tail-end surprise.
What Actually Determines Thermoforming Production Time?
Total production time is the sum of four phases: tool design and build, sheet preparation, forming cycles, and trimming with finishing. Within the forming cycle itself, heating and cooling account for most of the minutes. Sheet thickness, material, and heating uniformity decide hours per hundred parts; everything else moves the total by seconds.
For heavy-gauge work, sheet in the 3–10 mm range commonly cycles in roughly 2–8 minutes depending on material, draw depth, and mold construction. The relationship between thickness and cycle time is not linear: heating time rises close to the square of thickness because heat must conduct to the core of the sheet before the surface reaches a formable state, and the same conduction physics works against you during cooling. Doubling the gauge does not double the cycle; it can triple it.
Heating uniformity matters as much as raw heater power. Heater panel zoning must match the sheet area actually drawn; a sheet whose edges run 10–20 °C hotter than the center will sag unevenly, flag, or thin preferentially at the corners. Industry references such as the SPE Thermoforming Division document how sheet temperature distribution drives both cycle consistency and wall-thickness control, which is why serious cycle-reduction work starts with a temperature survey, not with the press.
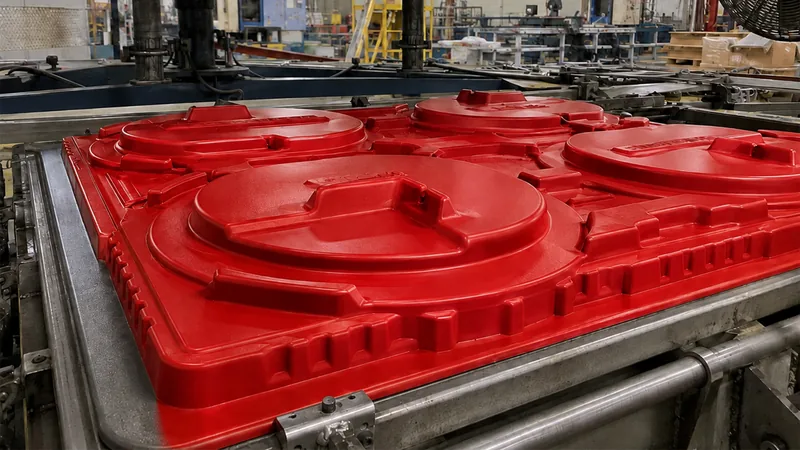
A practical check before any speed-up attempt: measure sheet surface temperature at several points at the end of heating, across consecutive cycles. If the spread between points exceeds roughly 10 °C, or the readings drift from cycle to cycle, shortening the cycle will only shorten it into scrap. For a fuller breakdown of the variables involved, see the guide to thermoforming cycle time factors.
Hygroscopic materials add a preparation phase that is easy to forget: ABS, PC, and PA sheet should be dried before forming, because absorbed moisture releases vapor at forming temperature and leaves bubbles or silver streaks that no later step can remove. Drying capacity, not the press, becomes the pacing resource when a program starts without dried production-gauge sheet.
ZetarVac runs more than 20 vacuum forming machines, processing sheet from 0.5 to 15 mm thick with forming lengths up to about 2,500 mm. For a buyer, that means trials can run on one line while another holds stable production, instead of a single machine becoming the schedule bottleneck.
Which Engineering Tasks Can Run in Parallel?
Almost everything except forming itself. Tool building, trimming-program preparation, and sheet specification can all start before the first formed part exists. Treating these tasks as a strict sequence is the single largest avoidable delay in a heavy-gauge vacuum forming program.
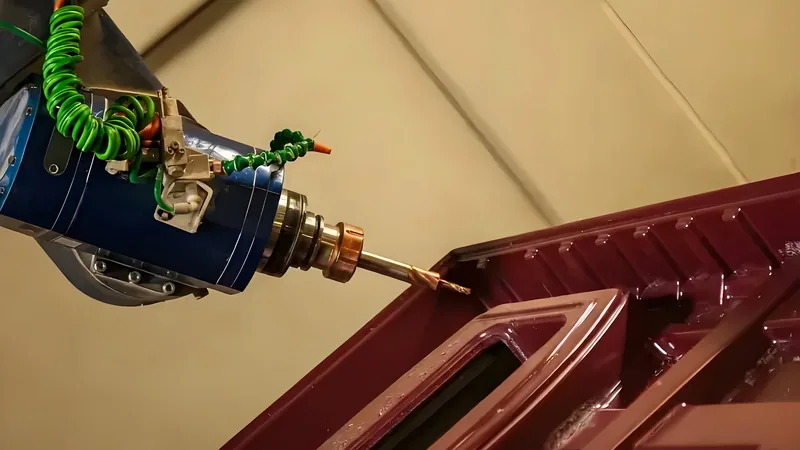
Mold manufacturing is the long pole. A machined aluminum tool for a mid-complexity part typically takes weeks, so the design-freeze decision — draft angles, corner radii, shrinkage allowance, cooling channel layout — deserves more schedule attention than the press rate. Once the forming-tool CAD is frozen, the 5-axis trimming program can be generated from the same geometry, because the trimmed outline follows the forming tool; NC programming has no reason to wait for formed parts.
Sheet logistics form the second parallel track. Material, gauge, color, and texture should be locked before tooling finishes so that production-gauge sheet is on site when the mold is. Changing sheet thickness after the tool is built forces a heating-profile restart and often mold rework. Logistics exposure after shipping is its own topic; the guide to heavy-gauge thermoforming lead time and logistics risk covers that side in detail.
"Running the sheet hotter forms the part faster and shortens the cycle."False
Overheated sheet sags under its own weight, thins unpredictably over deep draws, and takes longer to cool because more heat must be removed. The realistic fastest cycle sits at the lowest temperature that still fills the tool detail.
"The fastest stable cycle forms at the lowest sheet temperature that fills the tool."True
Forming near the lower end of the material window reduces sag and thinning, and leaves less heat to extract during cooling. Cycle reduction comes from finding that lower limit through controlled trials, not from more heater power.
How Much Can Mold Design and Cooling Save?
A well-cooled tool is worth more than a faster press. Moving heat out of the part through the mold is usually the rate-limiting step in heavy-gauge forming, and mold design controls exactly that.
Cooling channels placed close behind the forming surface, with turbulent water flow, keep the mold surface temperature stable between cycles. Male tools cool the part’s inner surface while the outer surface stays free; female tools do the opposite, so the tool type affects both wall distribution and where heat escapes. Deep draws also raise the draw ratio1, which concentrates thinning at corners — and thin corners both reject parts and lengthen the cooling needed before safe demolding.
Material choice compounds the effect. High-heat materials need a higher sheet temperature to form and release more heat into the mold per cycle; their heat deflection temperature2 also decides how long the part must stay on the tool before it can be handled without distortion. Where fine texture or sharp detail is required, pressure forming adds modest air pressure above the vacuum and can form detail faster than vacuum alone, at the cost of higher tooling requirements. Selecting adequate rather than excessive heat resistance is therefore a cycle-time decision as much as a performance decision.
| Phase | What drives the time | Practical lever |
|---|---|---|
| Tool design and build | Part complexity, cooling design | Freeze design early; start 5-axis programming from tool CAD |
| Sheet preparation | Material availability, drying, gauge | Lock material and gauge before tooling finishes |
| Forming and cooling | Sheet thickness, material, draw depth | Form at the lowest workable temperature; cool the tool properly |
| Trimming and finishing | Geometry complexity | Generate 5-axis programs in parallel with forming trials |
| Validation | Required standards and test volume | Agree the test plan when the tool is ordered |
Does Machine Capacity Shorten a Program, or Just a Cycle?
More machines never make one cycle faster, but they decide how much schedule risk a program carries. Parallel lines let trials, tool changes, and production runs coexist instead of queuing behind each other.
A plant running dozens of forming lines can hold a pilot press for trials while production continues elsewhere, absorb a sheet-batch change without losing a delivery slot, and run a second tool when volumes justify it.

Reference monthly capacity in the six-figure range only converts into shorter lead times when that kind of redundancy sits behind it. Capacity without trial discipline simply fills the plant with work in progress.
ZetarVac operates 45+ production lines across the plant with a reference monthly output of about 100,000–200,000 pieces. For a schedule-sensitive program, that spread means a forming trial does not have to interrupt the machine running your parts, which is where calendar time is actually saved.
Trial discipline matters as much as installed capacity. A shortened cycle should be proven with recorded cycle times, sheet temperatures, and reject rates before it is promised to a delivery schedule, and common failure signatures are catalogued in the guide to thermoforming problems.
"Once the first article passes inspection, the run will hold the same cycle."False
First-article approval happens on a stabilized, attended setup. Sheet batch variation, heater aging, and ambient conditions shift the process window over a run, and a cycle that was fast on part one can drift into reject territory by part two hundred.
"Cycle stability must be demonstrated over a continuous run, not one part."True
A meaningful confirmation records cycle time, sheet temperature, and reject rate across dozens of consecutive cycles after the setup settles. Only then is a shortened cycle safe to lock into the delivery schedule.
How Do You Compress Validation Without Weakening It?
Validation belongs inside the schedule, not after it. The test plan should be agreed when the tool is ordered, so stiffness, heat, and flammability checks run on the first production-intent parts instead of delaying shipment weeks later.
For structural formed panels and enclosures, flexural stiffness is the usual acceptance property: ASTM D790 defines the standard flexural test used to verify the stiffness of formed panels and enclosures3, and specimens can be cut from early formed parts while forming continues on the same machine. For parts facing elevated service temperatures, deflection-temperature testing confirms that the formed part keeps its shape under load, which matters for enclosures mounted near motors or heat sources.
Flammability requirements for equipment enclosures follow UL 944, and test specimens should be formed from the production sheet rather than cut from unformed stock, because forming changes orientation and residual stress and therefore the measured behavior. Planning these tests in parallel with the run — using parts cut from the same production window — keeps validation from becoming the tail that wags the schedule.
FAQ
Can vacuum forming handle thick structural parts at production speed?
Yes. Heavy-gauge thermoforming routinely forms sheet from 3 mm up to 15 mm into housings, trays, and structural covers, with cycle times of a few minutes per part. The trade-off is that thick sheet amplifies every heating and cooling inefficiency, which is why the levers in this article matter more as gauge increases.
Does a deeper draw always mean a longer cycle?
Usually, but not proportionally. Deeper draws raise the draw ratio, increase thinning risk, and often need slower forming speeds to control wall distribution, but a well-zoned heater and a correctly placed plug assist can keep the added time small.
What is the fastest route to first formed parts?
A prototype tool on a production-intent machine. Prototyping, small-batch, and large-batch runs are all supported, so the practical shortcut is a single-cavity aluminum prototype tool that proves the process window before the production tool is cut.
Which material choices most affect production time?
Heat content and formability. Materials that form at lower temperatures cycle faster and demold sooner, while high-heat materials trade cycle time for temperature and impact performance. Locking the material early matters because it drives the heating profile, the mold cooling design, and the validation plan together.
Where can I learn more about this process?
To see how the whole process fits together — materials, tooling, and the steps from sheet to finished part — explore the ZetarVac vacuum forming guide, or review the forming capabilities on the China vacuum forming manufacturer overview.
-
Draw ratio: The ratio of formed part area to starting sheet area; higher draw ratios concentrate wall thinning at deep corners. ↩
-
HDT: Heat deflection temperature, the temperature at which a plastic bar deflects a set amount under flexural load, measured per ISO 75-2. ↩
-
ASTM D790: Standard test method for flexural properties of unreinforced and reinforced plastics, used to verify the bending stiffness of formed panels and enclosures. ↩
-
UL 94: Standard for the flammability of plastic materials, classifying how a plastic extinguishes after ignition; commonly required for equipment enclosures. ↩


