
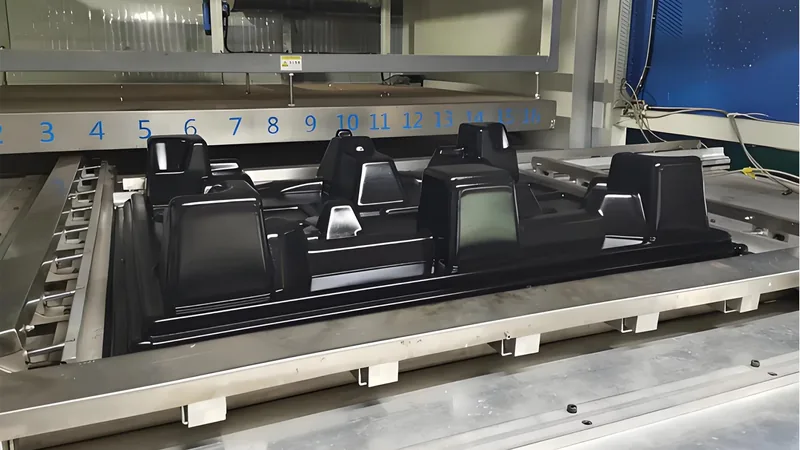
Polypropylene (PP) offers chemical resistance, toughness and low material cost, which is why it appears everywhere from industrial trays to equipment covers. It is also one of the less forgiving sheet materials in heavy-gauge thermoforming: a narrow heating window, high shrinkage and a fast sag once forming temperature is reached. Making good PP parts is less about special equipment and more about disciplined control of heat, vacuum and cooling. This guide walks through the process from sheet selection to trimming and inspection.
- PP thermoforming works in a narrower temperature window than ABS or PVC, so heater setup and sag control matter more than machine size.
- Sheet selection drives the result: homopolymer for stiffness, impact copolymer for toughness, UV stabilization for outdoor parts.
- PP shrinks more than most sheet materials, conventionally around 1–2.5%, so tooling must be compensated and cooling kept uniform.
- Fast vacuum evacuation and plug assistance hold wall thickness on deeper draws.
- Trim PP parts only after they have fully settled; 5-axis CNC trimming keeps the outline consistent with the formed geometry.
What Does It Take to Form Polypropylene Successfully?
Polypropylene forms well on standard heavy-gauge vacuum forming equipment. The difficulty is control rather than capability: PP works in a narrower sheet-temperature band, conventionally around 150–175 °C at the sheet surface as a starting range, and it needs faster response from the heaters, the vacuum system and the cooling stage.
PP differs from styrenic sheet in three ways that shape the whole process. It carries more heat per kilogram, so the oven needs more energy and slightly longer times for the same thickness. Its melt strength is low, so the sheet sags quickly and keeps thinning under its own weight if it hangs too long. And it shrinks as it cools, more than most sheet materials, which affects both tooling and part stability.
On the forming side, the softened sheet is drawn over the mold by vacuum, and deeper parts get help from a plug assist1 that pushes material into the cavity before the vacuum pulls it tight. Fine texture or sharper detail can justify pressure forming, which adds air pressure on top of the vacuum, but well-designed vacuum forming with plug assistance covers most industrial parts.
Material data should stay traceable: ISO 527-2 defines the tensile test method used to validate both incoming sheet and formed parts, so tensile values quoted for a PP thermoformed component should be reported against this method. For broader process background, the SPE Thermoforming Division publishes practical references on heating, forming and tooling practice.
Choosing the Right PP Sheet for the Job
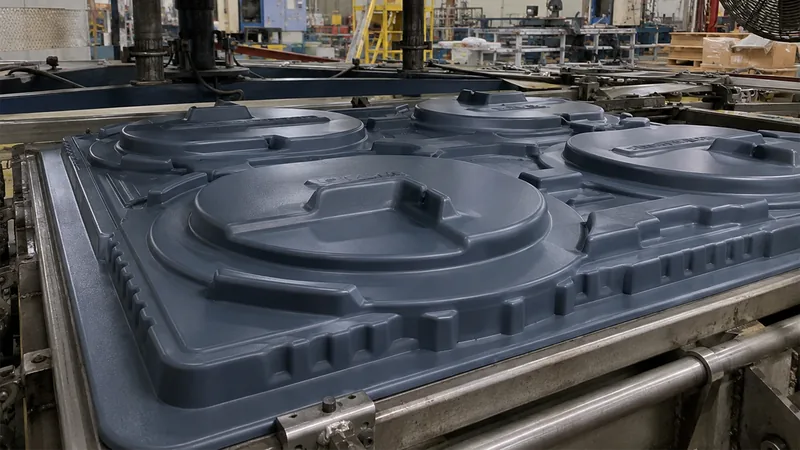
Sheet choice decides most of the downstream behavior before the oven is switched on. Homopolymer PP is the stiffest and usually the cheapest option and suits flat or shallow parts: panels, guards and trays with modest draw. Impact copolymer trades some stiffness for much better low-temperature drop resistance, which matters for industrial trays and housings that get handled daily.
Thickness drives cycle time and rigidity. Most heavy-gauge PP work falls between roughly 1 and 8 mm, and the trade-offs are familiar: thicker sheet heats and cools slower but produces stiffer, more stable parts. A detailed breakdown of the full 0.5–15 mm processing window is covered in our thermoforming thickness guide.
Grade details matter as much as base resin. Melt flow index2 deserves a glance: thermoforming wants high melt strength, so very high-flow grades form poorly even when their datasheets look attractive. Outdoor covers and agricultural trays need UV stabilization, and color choice affects how much solar heat a part absorbs.
Standards give the selection a neutral footing. ISO 75-2 specifies how the heat deflection temperature of a plastic is measured under flexural load, and it is the reference behind the HDT figures3 you compare when a PP part must survive a warm environment. Regulation (EU) 10/2011 governs plastic materials and articles intended to come into contact with food, and it is the baseline a PP thermoformed packaging tray must meet before entering a food supply chain.
| PP sheet grade | Typical thermoformed parts | Selection notes |
|---|---|---|
| Homopolymer | Flat panels, guards, rigid trays | Highest stiffness, lowest cost; weaker impact resistance when cold |
| Impact copolymer | Industrial trays, equipment housings | Better drop and low-temperature toughness; slightly softer surface |
| UV-stabilized | Outdoor covers, agricultural trays | Additives slow weathering; color still affects heat gain |
| Higher-HDT grades | Parts near warm equipment | Better heat resistance; forming window tends to narrow |
| Food-contact grade | Packaging trays and boxes | Sheet must be produced against EU 10/2011 requirements |
"A thicker PP sheet always delivers a stiffer, better part."False
Stiffness scales roughly with the cube of thickness, but deep draws thin the sheet non-uniformly, so a thick blank can still produce a weak corner wall. Overspecifying thickness also adds cycle time and cost without fixing what is usually a geometry problem.
"Rigidity should be verified on the trimmed formed part, not on flat sheet data."True
Forming redistributes wall thickness, so the meaningful check is flexural stiffness on a real sample. When a part needs more stiffness, a rib, a return flange or a small geometry change often beats adding a full millimetre of sheet.
Both decisions — grade and thickness — are easier to make against real part geometry than against a datasheet alone, and the forming envelope sets boundaries early.
ZetarVac processes thermoforming sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm, which covers the large PP panels, liners and housings where grade and thickness decisions carry the most cost.
What Heater and Mold Settings Work for PP?
As a conventional starting window, heat PP sheet from both sides to roughly 150–175 °C at the sheet surface, keep mold temperature in the 40–70 °C range, and apply vacuum as soon as the sheet reaches its sag target rather than after. Exact values depend on grade, thickness and machine, so treat these as a window to validate, not fixed numbers.
Heating uniformity is the first quality gate. PP punishes uneven heating faster than ABS: a hot zone produces a thin patch, a cold zone leaves a thick, unstretched corner. Zone-by-zone oven control matters, and heating time scales with thickness, so a 6 mm industrial panel needs a different recipe than a 2 mm tray. Watch the sag rather than the clock, and move the sheet when it drops smoothly and evenly.
Vacuum application should be fast, because the gap between ready-to-form and too-thin-in-the-middle is short. A quickly evacuating vacuum system plus well-placed mold holes and vents holds wall distribution on the draw. Mold temperature controls surface finish and stress: cold molds freeze parts quickly but can lock in the stress that later becomes warpage, while molds in the 40–70 °C range give the material time to relax at a modest cycle cost.
"PP can be formed with the same oven recipe as ABS or PVC sheet."False
PP needs more heat input, sags sooner and thins more aggressively, so a recipe tuned for styrenic or vinyl sheet either underheats the blank or lets the center hang too long. The typical result is uneven wall distribution and dimensions that drift between parts.
"Every PP grade and thickness combination needs its own validated heater profile."True
Supplier data gets you into the window, but the profile is proven on the machine: record heater zones, sag time and vacuum delay, then freeze them into the setup sheet. This is what makes batch two match batch one.
Repeatability across machines is the next step after a single recipe works.
ZetarVac runs more than 20 vacuum forming and thermoforming machines, so a PP recipe validated once can be documented and repeated across the forming shop instead of living in a single operator’s notebook.
Why Do PP Parts Warp After Forming?
PP warps because it shrinks more than most thermoforming sheet materials and because uneven cooling locks different shrink rates into different zones of the part. Conventional mold shrinkage4 for PP sits around 1–2.5%, and the exact value varies with thickness, geometry and thermal history.
Two mechanisms dominate. Bulk shrinkage pulls every dimension down as the part cools from forming temperature to room temperature, so uncompensated tooling produces parts that come out small. Differential shrinkage is worse: zones that cool at different rates — a thick flange beside a thin wall, one face against a colder mold — shrink unequally, and the part bows toward the side that solidified last.
Mitigation is mostly symmetry and patience. Uniform mold temperature on both sides, even airflow during cooling and enough cooling time in the mold before demolding do more for flatness than any after-correction. Tooling should be cut with measured shrinkage built in, and draft planned early; our draft angle guide covers how draft interacts with shrinkage and ejection.
For long, flat panels, geometry helps as well: ribs, returns and formed-in flanges resist bowing far better than a plain flat sheet. Where a genuinely flat surface is required, plan for trimming and fixturing after the part has fully settled, since cutting too early captures dimensions that will no longer be true an hour later.
Cooling, Trimming and Secondary Operations
PP releases heat slowly for a plastic — its low thermal conductivity means cooling, not heating, often sets the real cycle time. Fans or mist cooling speed the formed part down, but it should not be demolded while still hot enough to distort under its own weight. A practical rule: demold when the part is dimensionally stable, then rest it on a flat fixture before any cutting.
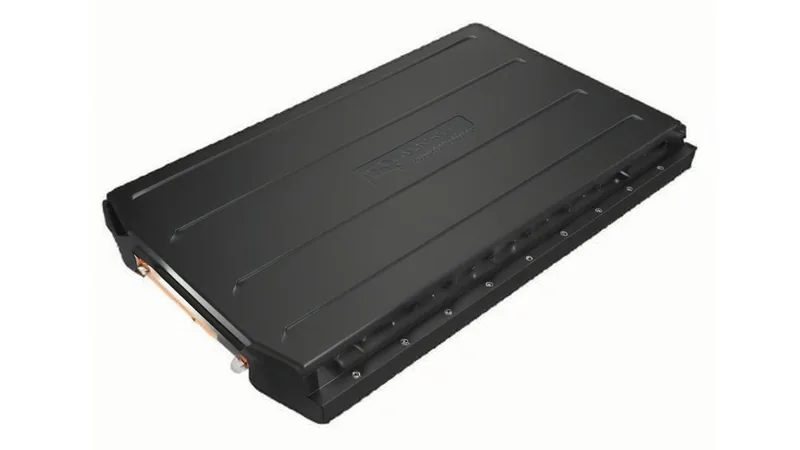
Trimming deserves the same engineering attention as forming. PP continues to settle for minutes after demolding, so trimming too early produces an outline that no longer matches the finished part. A 5-axis CNC trimming centre cuts the outline along the same geometry as the forming tool, keeping the trim line consistent from part to part; the options are compared in our CNC trimming and secondary operations guide.
ZetarVac’s 5-axis CNC trimming centre trims formed parts against the forming-tool geometry, which is especially useful for PP, where late dimensional change makes fixed jigs less dependable.
Which PP Thermoforming Defects Should You Watch For?
Most PP forming defects trace back to three roots: wrong sheet temperature, uneven heating or rushed cooling. The table maps the common failure modes to their usual causes and the first corrective action worth trying.
| Defect | Usual cause | First corrective action |
|---|---|---|
| Excessive sag or tearing | Sheet overheated or hung too long | Reduce zone power, form at first even sag |
| Thin corners and walls | Deep draw without plug assist; slow vacuum | Reshape plug, enlarge or reposition vacuum holes |
| Bubbles or blisters | Surface moisture or overheated surface | Check sheet storage, lower peak sheet temperature |
| Webbing between features | Sheet too hot or features too close | Reduce temperature, open spacing or radii |
| Warpage | Uneven cooling, uncompensated shrinkage | Balance mold temperature, extend cooling dwell |
| Sticking in the mold | Mold too hot or insufficient draft | Lower mold temperature, verify draft and finish |
"If the first article passes inspection, the production run is proven."False
A first article validates only that sheet lot, heater state and machine setup. PP shifts with sheet lot variation and oven drift, so a run can pass at piece one and drift out of tolerance by piece five hundred if nobody is measuring.
"Stable production needs interval checks, not just a good first article."True
Dimensional checks at defined points — first piece, mid-run, last piece — catch drift while it is still correctable. Logging heater zones, cycle time and sheet lot numbers makes the record usable when something does move.
Process discipline separates a one-off good part from a dependable supply. Sheet lot records, fixed heater profiles, logged vacuum delay and scheduled dimensional checks turn PP’s quirks into a controlled process. Buyers evaluating suppliers get more signal from asking how these parameters are recorded than from any sample.
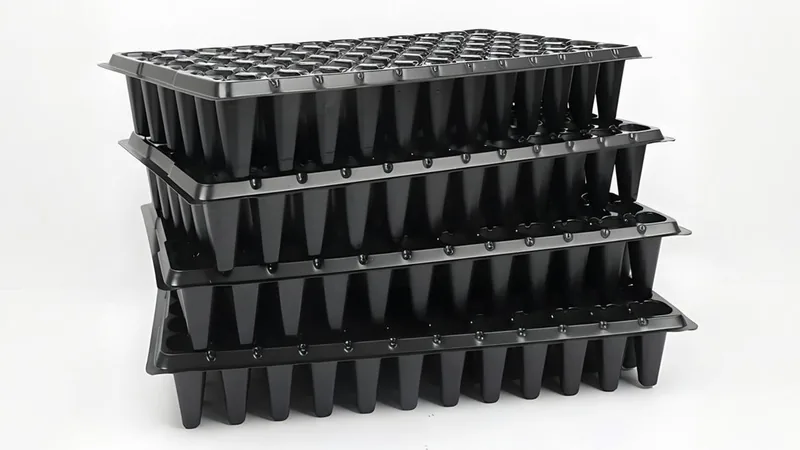
FAQ: Making PP Thermoformed Sheets
What sheet thickness can heavy-gauge PP thermoforming handle?
Heavy-gauge processing commonly covers 0.5–15 mm at well-equipped forming shops. Thicker sheet means longer heating and cooling, so the practical limit is usually cycle time and heating capacity rather than formability itself.
Does PP sheet need drying before thermoforming?
Usually not. PP absorbs very little moisture compared with many engineering sheet materials. If pallets were stored in a cold, damp space, surface condensation can cause bubbles, and simply letting the sheet reach room temperature before forming normally solves it.
How much shrinkage should PP tooling allow for?
Plan around 1–2.5% as a conventional starting range for PP, then confirm on trial forms when tolerances are tight. Thickness, geometry and cooling all shift the final value.
Can thermoformed PP parts be used outdoors?
Yes, with UV-stabilized grades. Unstabilized PP embrittles over seasons of sunlight exposure, so outdoor service should be declared at the design stage along with color and expected service life.
Is vacuum forming PP suitable for food-contact trays?
Yes, when the sheet itself is produced against food-contact requirements. Regulation (EU) 10/2011 governs plastic materials and articles intended to come into contact with food, so compliance sits primarily with the sheet grade; forming then has to avoid contamination from tooling and handling.
If you want to go deeper on the process before comparing suppliers, explore our vacuum forming guide, or see how we approach heavy-gauge PP projects from prototype through volume production as a vacuum forming manufacturer.
-
Plug assist: A shaped tool that mechanically pushes the heated sheet into the mold cavity before vacuum is applied, improving wall distribution on deep draws. ↩
-
MFI: Melt flow index, a measure of how easily molten plastic flows; thermoforming favors lower-flow, higher-strength sheet grades. ↩
-
HDT: Heat deflection temperature, measured per ISO 75-2 as the temperature at which a standard bar deflects a specified amount under flexural load. ↩
-
Mold shrinkage: The percentage dimensional change of a formed part as it cools from processing temperature to room temperature. ↩




