

Heavy gauge thermoforming turns thick plastic sheet — typically 0.5 to 15 mm in an industrial shop — into structural housings, trays, guards and covers without the tooling cost of high-pressure molding. For a manufacturer deciding whether to build the capability in-house or to source formed parts, the question is rarely whether the process works. It is whether the economics, part sizes and material options line up with the product program. This article answers that from the engineering side: where vacuum forming pays back, what tolerances it holds, which standards govern formed enclosures, and how to qualify a supplier before committing volume.
- Heavy gauge thermoforming is the economical route for large, thick-walled parts in volumes from prototypes to hundreds of thousands of pieces per year.
- Sheet from 0.5 to 15 mm and forming lengths up to about 2,500 mm cover most equipment housings, machine shrouds, trays and structural panels in one piece.
- Tooling is the main cost lever: forming tools cost a fraction of high-pressure tooling and can be revised between runs.
- Standards such as UL 94, IEC 60529 and ASTM D638 let formed parts be qualified for real electrical and industrial duty.
- Failure modes — bubbles, splay, uneven wall distribution — are predictable and screenable during first article approval.
What Counts as Heavy Gauge Thermoforming?
Heavy gauge (or thick-gauge) thermoforming is vacuum or pressure forming of sheet thicker than about 1.5 mm: the sheet is heated, draped over a mold and formed under vacuum instead of being injected under pressure. The forming window, heating pattern and cooling times all scale with sheet thickness. In practice, heavy gauge covers structural parts — enclosures, trays, shrouds — while thin-gauge work covers disposable packaging.
The distinction matters for an investment decision because equipment, tooling and quality controls differ by gauge class. A heavy gauge vacuum forming line heats sheet that must carry its own weight, forms deep draws over minutes rather than seconds, and depends on controlled top-and-bottom heating and slower cooling. Pressure forming adds air pressure on the sheet face to sharpen texture and detail when a formed part has to mimic a molded surface.
Industry references such as the SPE Thermoforming Division document these process variables in detail. On the shop floor the sequence is simple: load sheet, heat both faces to forming temperature, seal the clamp frame, apply vacuum, cool below heat deflection temperature, release, trim. The engineering lives in the middle — sheet temperature uniformity, vacuum rate, plug assist geometry on deep draws, and cooling gradients that decide whether the part stays flat or warps.

Where Heavy Gauge Thermoforming Pays Back for Manufacturers
The investment case rests on three part families that recur across industries.
Equipment housings and machine covers. Formed ABS, PC or ASA housings protect diagnostic machines, industrial controllers and outdoor equipment. A housing up to about 2,500 mm long forms in one piece, which removes the assembly joints and sealing paths that multi-piece fabrication creates.
Heavy-duty trays and dunnage. Multi-cavity trays in HDPE, PP or ABS carry parts through washing, assembly and shipping. Cavity count, cell geometry and tray size are customizable, so the tray matches the component rather than the reverse.
Guards, liners and structural panels. PC guards, equipment liners and reinforced panels absorb impact and trim to complex outlines.
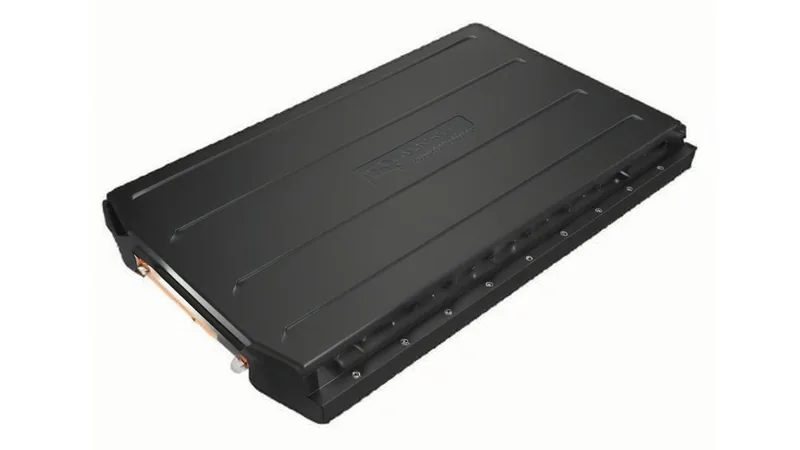
The economics favor thermoforming when parts are large, walls are thick and volumes run from prototypes to hundreds of thousands of pieces per year. Forming tools cost a fraction of high-pressure tooling, and lead time is measured in weeks, so a manufacturer can qualify a design before committing to hard tooling. Revisions are practical because forming tools can be modified between runs — a real advantage while a product program is still moving.
ZetarVac runs 20+ vacuum forming and thermoforming machines processing sheet from 0.5 to 15 mm, with maximum forming length of about 2,500 mm. For a buyer, that means a single formed part can replace a multi-piece fabricated assembly even at machine-envelope sizes.
A useful way to frame the decision is by what the process controls well and what it does not. Thermoforming controls the mold-side surface precisely but lets the free surface follow sheet sag; it handles large envelopes easily but distributes wall thickness unevenly on deep draws. Buyers who understand those two boundaries write better specifications — and avoid both over-tight tolerances and false economies.
"A passed first article proves the production run will stay stable."False
First article approval validates the tool, the setup and the measurement plan at one point in time. Sheet-lot variation, heater ageing and ambient shifts move wall distribution and warp over a run, which is why release criteria must include in-process checks, not just the first piece.
"Stable forming depends on monitoring wall distribution, not just outline."True
Wall thickness is the main hidden variable in thermoforming: hot zones stretch more and finish thinner. Tracking minimum wall at defined part locations catches drift long before it becomes scrap or a field failure.
What Tolerances and Sizes Can Vacuum Forming Hold?
Formed parts routinely hold about ±1% on major dimensions and roughly ±0.5 mm on trimmed edges for mid-size parts, with tighter control where the mold forms the surface. Wall thickness is where thermoforming differs most: distribution varies with draw depth, so a 3 mm sheet may finish between roughly 2.4 and 3.0 mm across a deep draw. Exact values depend on material, draw ratio and tool design.
Three geometric facts set the tolerance picture. Only the mold-side surface is controlled; the free surface follows sag and cooling. Deep draws thin the sheet — a working rule of thumb allows roughly 10–25% thinning across a deep draw, worst at sharp inside corners and plug-assist contact zones. Trimming then defines the final outline, so the trim method decides edge tolerance and repeatability.
That is where five-axis trimming earns its place. When the trimmed outline follows the forming tool, hole patterns, cut-outs and seams register to the formed geometry instead of a separate fixture — which is how large housings keep mounting holes aligned across a full production run.
Sheet capability defines part size. Processing 0.5–15 mm sheet with forming lengths around 2,500 mm covers most machine shrouds, medical housings, agricultural trays and logistics containers in one formed piece. Material interacts with size: PC and PC/ABS hold stiffness in thinner walls at elevated temperature, while HDPE and PP tolerate impact and washdown in tray duty.
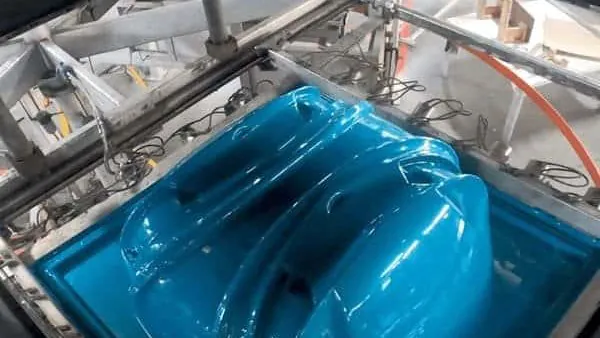
Use this table as a first-pass material screen for common formed parts:
| Material | Typical formed parts | Selection driver |
|---|---|---|
| ABS | Housings, cases, guards, automotive interiors | Balanced cost, impact strength and paintability |
| PC / PC/ABS | Clear guards, protection covers, equipment housings | Stiffness and elevated-temperature performance |
| HDPE / PP | Industrial trays, equipment liners, boxes | Chemical and washdown resistance |
| ASA | Outdoor equipment housings, exterior parts | UV and weathering stability |
| PP/GF | Structural automotive and industrial parts | Stiffness at reduced weight |
| PMMA | Clear covers, luminaires, display parts | Optical clarity and weathering |
Five-axis CNC trimming of formed parts means the trimmed outline follows the forming tool directly. Cut-outs, mounting holes and seams stay registered to the formed geometry without secondary fixtures, which shortens first-article iteration on complex housings.
Which Standards Govern Formed Enclosures and Covers?
Formed housings and covers qualify under the same standards as molded ones. UL 94 governs flammability of plastic materials and is required for many electrical enclosures,1 while IEC 60529 defines the IP code that rates how well an enclosure excludes dust and water.2
ASTM D638 defines the standard tensile test run on thermoformed sheet, so material data and first-article validation speak the same language whether a part is formed or molded.3 ISO 75-2 specifies the heat deflection temperature test — the property that decides whether a housing over a drive or power supply keeps its shape at operating temperature.4 For guards and liners that take impact, ISO 6603-2 defines instrumented puncture testing of rigid plastics, which maps directly onto dropped-tool and debris scenarios.5
The practical point: a formed enclosure can carry a compliance story, not just a shape. Ask which flammability rating the application needs, whether an IP rating will be claimed on the finished machine, and confirm the selected compound — a flame-retardant ABS or PC grade, for example — supports it. Ratings attach to the compound and the tested assembly, so sheet grade selection comes before process decisions.
How Should You Qualify a Thermoforming Supplier?
Qualify a thermoforming supplier on process control, not machinery lists. The checks that predict production stability are sheet heating uniformity, wall-thickness reporting on formed parts, trim repeatability and a documented first-article release process.
Start with design-for-process review. A capable supplier flags draw ratio limits, corner radii, draft angles and undercuts before tooling is cut; the DFM checklist for heavy gauge thermoformed parts and molds covers the specific geometry rules. Treat a supplier who accepts every geometry without comment as a warning sign — deep draws, sharp inside corners and tight male detail are exactly where formed parts thin and warp.
Verify defect control next. Bubbles and splay marks trace back to sheet moisture and heating practice, and the failure mode is well documented; a serious shop will show how it screens for it rather than insisting it never happens. Ask how wall thickness is measured on formed parts, where minimum-wall points sit on your geometry, and what release limits apply.
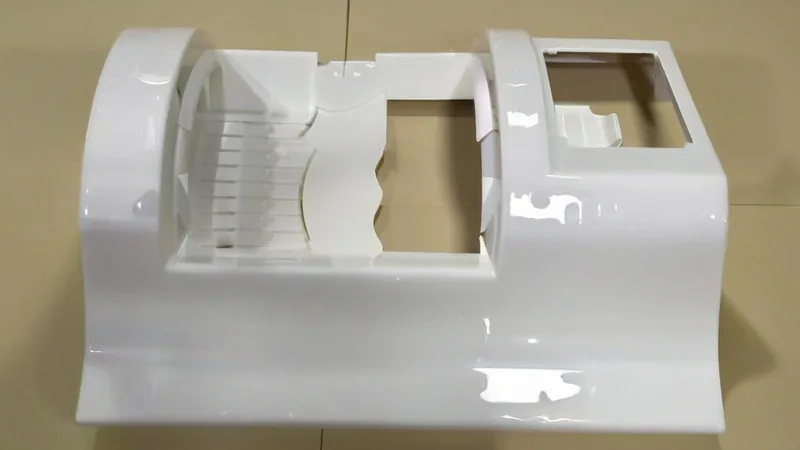
Capacity matters for the investment decision. A plant running 45+ production lines with reference monthly output of 100,000–200,000 pieces can absorb program growth without a supplier change, and supports prototyping through large batch on one tooling philosophy.
ZetarVac supports prototyping, small batch and large batch production on the same forming capability, with reference monthly capacity of about 100,000–200,000 pieces. A program can move from pilot tooling to volume without changing process or supplier.
One more distinction separates buyers who get stable supply from those who firefight: how the supplier treats tooling as a living asset rather than a one-off purchase. Forming tools get revised, maintained and sometimes re-cavitated, and the plan for that work belongs in the quotation discussion rather than in a change order a year later.
"Heavy gauge thermoforming only makes sense for low-volume programs."False
That view confuses the process with the volume band of its cheapest tooling. With multi-cavity tools and plant capacity above 100,000 pieces per month, formed trays and housings run at serious volumes; the real constraints are part geometry and wall uniformity, not a volume ceiling.
"Volume readiness shows in tooling strategy, not machine count."True
A supplier who designs forming tools for maintenance, revision and multi-cavity scaling can grow a program; one who treats each tool as a one-off cannot. Ask how a tool is revised and how cavities are added before you commit volume.
FAQ: Heavy Gauge Thermoforming Investment
What sheet thickness counts as heavy gauge?
Industrial practice treats roughly 1.5 mm and above as heavy gauge, with capable shops processing 0.5–15 mm. The practical boundary is where the sheet becomes self-supporting after heating and the process shifts from fast thin-wall cycling to controlled forming with longer heat and cool phases.
How large can a vacuum formed part be?
Heavy gauge equipment forms parts up to about 2,500 mm long, which covers machine shrouds, medical equipment housings and large agricultural trays in one piece. Practical size is bounded by sheet width, oven capacity and clamp frame, so confirm the envelope against your part outline early.
How much material does thermoforming waste?
Web and trim scrap typically runs in the 20–40% range on complex parts, but ABS, HDPE, PC and PP trim is commonly reground and blended back where the application allows it. Ask how the supplier handles regrind and whether your purity requirements permit it.
Can formed parts meet IP or flame ratings?
Yes — ratings attach to the material compound and to the tested assembly, not to the forming process itself. Select grades that carry the required UL 94 rating, design the flange and sealing path, and validate the finished enclosure against IEC 60529.
Where should you go deeper before comparing suppliers?
The vacuum forming guide walks through the process, materials and tooling choices in detail, and the China vacuum forming manufacturer page shows how an operating plant organizes forming, trimming and inspection. Both are worthwhile next reads while you build your comparison criteria.
-
UL 94: The flammability classification standard for plastic materials used in electrical equipment. ↩
-
IP code: The ingress protection rating defined by IEC 60529 for enclosures against dust and water. ↩
-
ASTM D638: The standard tensile test for plastics, used to validate thermoformed sheet and formed parts. ↩
-
Heat deflection temperature (HDT): The temperature at which a plastic specimen deflects a defined amount under flexural load, tested per ISO 75-2. ↩
-
Puncture impact (ISO 6603-2): Instrumented test measuring the force and energy required to puncture rigid plastics. ↩


