
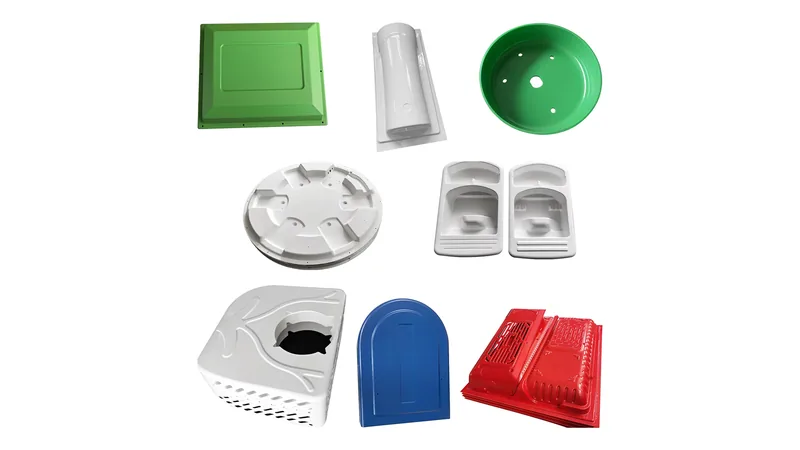
When a part grows too large, too thick or too structural for thin-gauge packaging, it moves into heavy gauge territory: sheet formed from 0.5 mm up to 15 mm, trimmed on 5-axis CNC machines, and shipped as equipment housings, trays, panels and structural covers. This guide walks through the industries that rely on these parts, why each industry specifies them, and what buyers should verify before committing to a forming program.
- Heavy gauge thermoforming covers parts formed from sheet roughly 0.5–15 mm thick: machine enclosures, automotive interior panels, seedling trays and logistics trays.
- The main user industries are industrial equipment, automotive and transportation, medical, agriculture, logistics and retail display.
- Material choice tracks the industry: ABS and PC/ABS dominate housings, ASA and PP serve outdoor automotive duty, PMMA delivers clear display covers, HDPE and PP fill tray programs.
- Enclosure programs must account for standards such as UL 94 and NEMA 250 early, because formed geometry and sealing design decide the rating, not late gasket additions.
- Thickness distribution is a design outcome: corners thin during forming, and stiffness comes from ribs and flange returns rather than heavier nominal sheet.
- A first article approval validates a setup, not future batches; ongoing dimensional checks belong in every mature forming program.
What Counts as Heavy Gauge Thermoforming?
Heavy gauge thermoforming is the forming of plastic sheet into parts where the sheet is thick enough to be structural, typically 0.5–15 mm.1 In practice the term covers vacuum forming and pressure forming, and it describes the part class — shrouds, housings, trays, covers — as much as the process itself.
The workflow stays consistent across industries. Sheet is clamped and heated into its forming window, drawn over or into a mold by vacuum (or by combined vacuum and pressure when surface detail matters), cooled, then trimmed. The difference from thin-gauge work is scale and engineering load: walls are stiffer, cycles run in minutes rather than seconds, and trimming is a machining operation. If you need the terminology split between the two forming variants, our comparison of pressure forming vs vacuum forming for heavy gauge parts breaks down when each variant earns its cost.
Which Industries Commonly Use Heavy Gauge Thermoformed Parts?
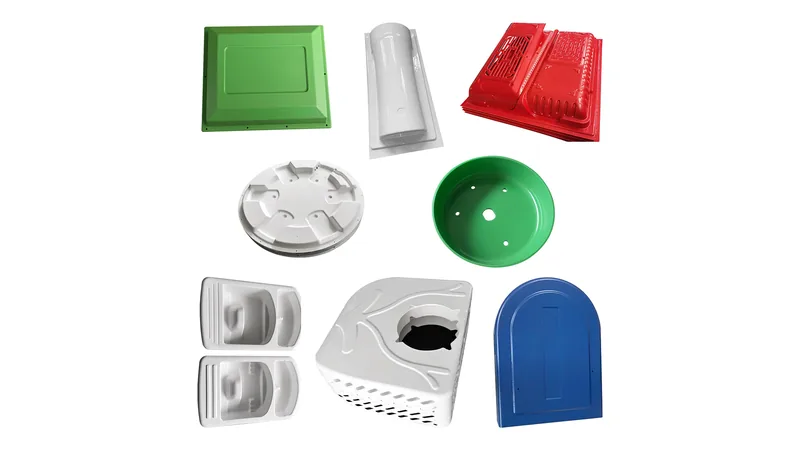
Six industries account for most heavy gauge forming demand: industrial equipment, automotive and transportation, medical, agriculture, logistics, and retail display. Each buys formed parts for the same core reasons — large surfaces at moderate volume, tooling cost far below other large-part routes, and fast design iteration — but each stresses the process differently.
| Industry | Typical formed parts | Common materials | Critical forming concerns |
|---|---|---|---|
| Industrial equipment | Machine shrouds, enclosures, base covers | ABS, PC/ABS, PC | Flatness, cut-out accuracy, flammability rating |
| Automotive | Interior panels, bumper covers, mud flaps | ABS, PP, ASA, PP/GF | Heat sag, grain match, assembly fit |
| Medical | Equipment housings, covers | PC, ABS | Cut-outs, reinforcement, cleanable surfaces |
| Agriculture | Seedling trays, equipment liners | ABS, HDPE, PP | Cavity repeatability, drainage geometry |
| Logistics | Trays, boxes, dunnage | HDPE, PP | Impact strength, stacking stiffness |
| Retail display | Clear covers, display parts | PMMA | Optical clarity, curved geometry |
The table is a starting point. The sections below look at what each industry actually specifies and where forming programs most often fail.
Why Do Industrial Equipment Makers Specify Thermoformed Enclosures?
Because a formed housing delivers a large, complex, one-sided surface at a fraction of the tooling investment of other large-part routes, and it can be revised quickly when the machine design changes. Machine shrouds, control cabinet covers and guards are classic heavy gauge work: sizes often exceed what other processes produce economically, and volumes rarely justify hard tooling.
Enclosure programs carry the heaviest standards load of any formed-part category. UL 94 grades the flammability of plastic materials, and many formed enclosures must meet a specified rating before they can be fitted to electrical equipment.2 UL 746C governs polymeric materials in electrical equipment more broadly, and it is the reference most enclosure engineers work from when they select a housing resin. For washdown or outdoor installations, IEC 60529 defines the IP code and NEMA 250 defines the equivalent enclosure types, and both constrain how flanges, seal faces and drainage have to be formed rather than added later.3
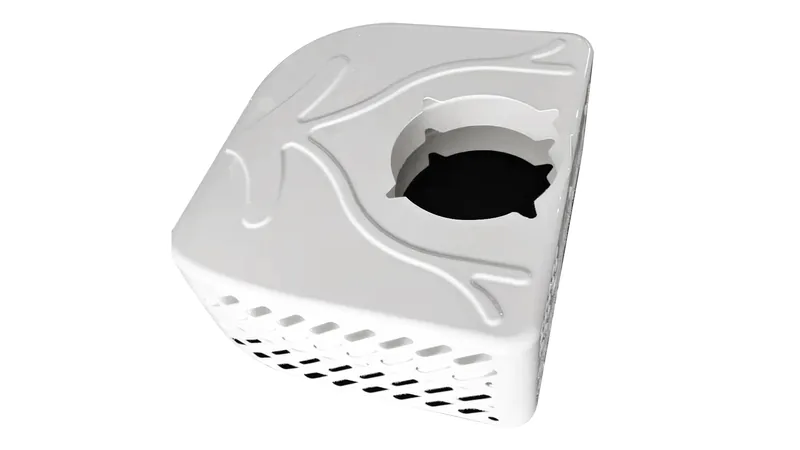
ZetarVac processes sheet from 0.5 to 15 mm with a maximum forming length of about 2,500 mm and runs 20+ vacuum forming machines alongside 45+ production lines. For equipment builders this means a full shroud or enclosure set can be formed in one piece instead of assembled from panels, which removes seal joints and speeds machine assembly.
Geometry decisions drive enclosure cost more than resin price. Every cut-out, mounting hole and reinforcement added to the formed face must be machined on the 5-axis trimming centre, so consolidating fastener locations onto formed flanges usually beats designing in extra brackets. The claim pair below is the most common enclosure mistake in incoming designs.
"Gasketing is enough to turn any formed cover into a NEMA Type 4 enclosure."False
A Type 4 rating demands sealing against hose-directed water, which depends on flange width, fastener spacing and the formed seal face — not on a gasket squeezed against a flat edge. Covers designed without this in mind leak at corners and fastener lines after the first washdown cycle.
"NEMA Type 4 performance has to be designed into the formed geometry and verified by testing."True
That means formed flange returns, ribbing around the seal face and fastener patterns laid out to keep clamp pressure even, decided during tooling design rather than after the first leak report. Verification then confirms the rating before the enclosure reaches the machine.
How Do Automotive and Transportation Programs Use Formed Parts?
Interior panels, bumper covers, mud flaps and underbody guards are the formed parts automotive buyers order most, typically in ABS, PP, ASA and glass-filled PP. Forming earns these programs because panel sizes are large, surfaces are functional rather than class-A, and annual volumes sit where forming tooling pays back quickly.
Heat is the defining failure mode in this industry. Interior panels sit near glass and inside parked vehicles, so resin selection starts with the heat deflection temperature of the material, and the forming window has to leave enough margin that the part does not warp in service.4 ASA and PP take outdoor duty; PP/GF carries structural loads where stiffness per weight matters.
Because these programs ship in volume, the gap between an approved sample and a stable batch is where most supplier disputes start; our guide to first article inspection for heavy gauge thermoformed parts explains what an approval actually locks down.
"Once the first article is approved, every later batch will match it automatically."False
A first article validates one setup: one tool temperature, one sheet lot, one cycle window. Sheet lots change, heater elements age and tool surfaces wear, so dimensional drift between batches is normal unless it is actively checked.
"Batch consistency requires in-process checks that go beyond the first article."True
Periodic thickness mapping, trim inspection and material lot documentation catch drift while parts are still in tolerance. Mature programs audit these checks during supplier selection, not after the first assembly-line stoppage.
What Do Agriculture, Logistics and Display Programs Need?
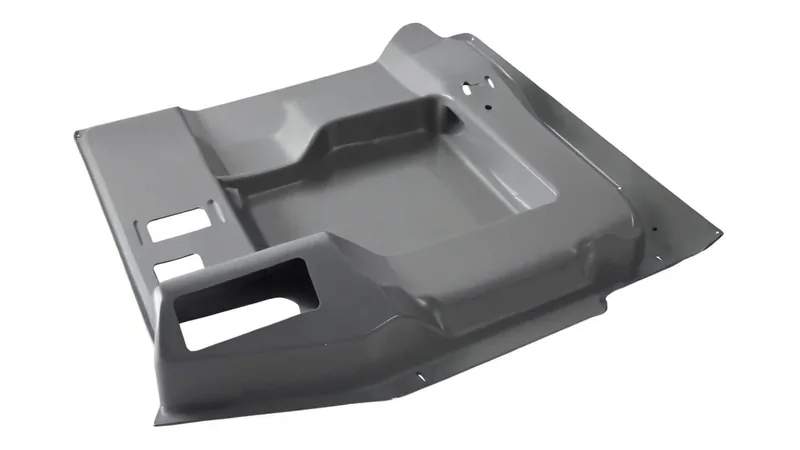
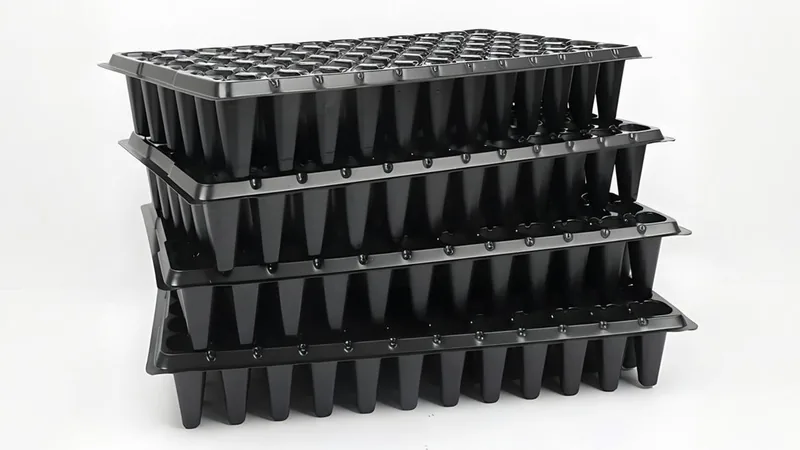
Agriculture buys trays and liners, logistics buys trays and boxes, and retail display buys clear covers — three industries with one shared requirement: repeatable geometry at volume. A formed seedling tray may run thousands of cavities per geometry and be re-used season after season, so cavity-to-cavity repeatability and drainage geometry matter more than surface finish. Logistics trays stack, so flange and rib layout has to hold stiffness under load, and HDPE or PP delivers the impact behavior.
Display work inverts the priorities. PMMA formed covers need high optical clarity, so sheet heating, mold surface temperature and forming speed are controlled to avoid marked or hazy zones — and curved geometry is exactly what makes forming the economical route for these parts.
ZetarVac’s reference monthly capacity is about 100,000–200,000 pieces, with prototyping, small batch and large batch production all supported. For tray and liner programs that scale seasonally, that range lets a pilot cavity layout move into volume production without changing the forming route or tooling approach.
How Should Material Selection Track the Application?
Match the resin to the industry’s dominant stress, not to a datasheet average. ABS and PC/ABS cover most housing and interior work because they form predictably and machine cleanly; PC earns medical and guard applications through impact resistance and clarity; ASA holds color outdoors; HDPE and PP absorb impact in tray duty; PMMA is reserved for clarity; and specialty resins such as PA6, POM, TPE, TPU and TPV fill sealing, precision and soft-touch roles.
Material validation runs through standard test methods rather than supplier claims. ASTM D638 is the tensile test most programs run on both incoming sheet and formed parts, because forming changes orientation and local thickness enough that flat-sheet data alone understates the real variation. On display and cover work, ISO 13468 defines total luminous transmittance, which is how clarity requirements are specified for formed PMMA parts. Our DFM checklist for heavy gauge thermoformed parts and molds5 covers how to translate these choices into draw ratios and corner radii before tooling is cut.
"Thicker sheet is the reliable way to make a formed part stiffer."False
Stiffness scales steeply with thickness for flat sections, but corners and deep draws thin during forming, so adding nominal thickness often adds weight and cycle time without stiffening the zones that actually flex. The result is a heavier part with the same failure points.
"Rib and flange geometry delivers stiffness far more efficiently than nominal thickness."True
Formed ribs, return flanges and edge stiffeners raise section depth exactly where loads concentrate, at little weight cost. This is why experienced designers review the thickness map after forming instead of simply specifying heavier sheet.
When you review a supplier’s sample, ask for the formed thickness map rather than the nominal sheet specification. It shows where corners thinned and whether the stiffening geometry actually landed where the load path needs it.
The material library at ZetarVac spans ABS, PC, PC/ABS, ASA, HDPE, LDPE, PP, PP/GF, PMMA, PA6/PA66, POM, TPE, TPU and TPV for formed parts. Choosing from resins a plant already forms shortens development, because draw behavior, heating profiles and trim behavior are already characterized for those materials.
FAQ: Heavy Gauge Thermoformed Parts by Industry
What sheet thickness range counts as heavy gauge in vacuum forming?
Most programs treat roughly 0.5 mm and above as heavy gauge, with 0.5–15 mm covering the vast majority of industrial housings, trays and panels. Below that range, work moves into thin-gauge packaging with different equipment and economics.
Which industry uses the most heavy gauge thermoformed parts?
Industrial equipment is the largest single user by part size: machine shrouds, enclosures and covers consume most large-format forming capacity. Automotive and logistics follow, driven by interior panels and tray programs respectively.
Can thermoformed parts meet enclosure protection ratings?
Yes, when the geometry is designed for it. Flange design, seal faces and fastener layout determine whether a formed cover reaches a given IP code or NEMA type, and the rating is confirmed by test after forming, not assumed from the material.
How many parts per year justify forming over other manufacturing routes?
There is no fixed threshold, but forming typically earns its place from prototyping volumes upward and stays economical through large batch production because tooling cost is low and revisions are fast. The break-even depends on part size, trimming complexity and the alternative route being considered.
What should I send a molder to start an industry-specific evaluation?
A 3D model or drawing with the working environment named, the target annual volume, and any rating or material constraints. With that, a molder can propose resin options, sheet thickness and a forming strategy against your geometry.
To keep digging into the process itself, explore our vacuum forming hub for the full process and material overview, or see how a China vacuum forming manufacturer sets up heavy gauge programs from prototype through volume. Walking through both pages gives you a concrete baseline before you start comparing suppliers.
-
Heavy gauge: Heavy gauge describes thermoforming work on sheet roughly 0.5 mm and thicker, where formed parts serve structural or protective roles rather than thin-wall packaging. ↩
-
UL 94: UL 94 is the standard for flammability of plastic materials, grading how a specimen extinguishes after ignition, from HB through V and 5VA/5VB ratings. ↩
-
IP code: The IP code from IEC 60529 classifies the degrees of protection an enclosure provides against ingress of solid objects and water. ↩
-
HDT: Heat deflection temperature, measured under flexural load per ISO 75-2 or ASTM D648, indicates the temperature at which a plastic part begins to deflect under load. ↩
-
DFM: Design for manufacturability, the practice of reviewing a part design against process constraints such as draw ratio, corner radius and draft before tooling is committed. ↩



