Material selection decides whether a vacuum formed part survives its working environment or turns into a warranty claim. The choice looks straightforward on a resin data sheet and behaves very differently on a forming table, because heating, draw depth and cooling push every material well past the conditions its datasheet numbers were measured at. This guide works through the decision the way a forming engineer would: service conditions first, formability second, verification third, cost last.
- Match the resin to the service environment before anything else: continuous temperature, impact, chemical exposure and required ratings eliminate most candidates quickly.
- Heavy gauge thermoforming between 0.5 and 15 mm sheet amplifies material behaviour — heating time, sag, corner thinning and warpage all scale with thickness.
- Verify the property that actually fails the part: deflection temperature for hot service, impact for guards, flammability for electrical enclosures.
- Standards such as ISO 75-2 and UL 94 turn material claims into comparable numbers; request them at your finished thickness, not just the grade name.
- Compare cost per accepted part, not cost per kilogram of sheet; yield, trim ratio and cycle time move the real number.
- Prototype in the exact grade, gauge and sheet-lot condition you intend to run in production.
What Should the Material Decision Actually Settle?
The decision settles three questions: whether the part survives its working environment, whether the sheet forms reliably at your draw depth and gauge, and whether the finished cost per part stays inside budget. Appearance, secondary operations and supplier logistics are filters on top of those three, never substitutes.
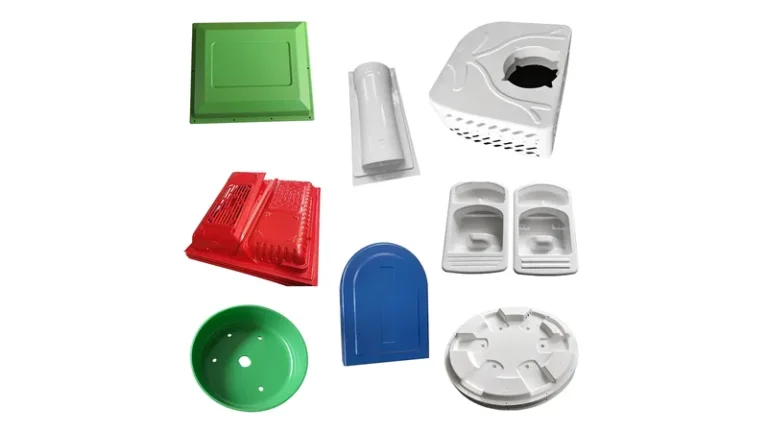
Work the shortlist in that order. A resin that fails the service environment is disqualified no matter how beautifully it forms, and a resin that cannot hold a deep draw is disqualified no matter how cheap the sheet is. Most projects start with eight to twelve candidate grades and end with two or three that deserve a forming trial. The table below is a working shortlist for heavy gauge thermoforming across the markets formed parts serve most often.
| Material | Typical formed parts | Key strengths | Watch-outs |
|---|---|---|---|
| ABS | Equipment housings, cases, guards, automotive interior parts | Tough, forms over a wide window, good surface finish | Limited UV resistance; dry sheet before heating |
| PC/ABS | Automotive interiors, equipment housings, guards | Balanced impact and rigidity, paintable | Needs thorough drying to avoid blisters |
| PC | Clear guards, equipment protection covers, automotive parts | Very high impact, optical clarity | High forming temperature; stress whitening on tight radii |
| HDPE | Industrial trays, equipment liners, storage boxes | Chemical resistance, low cost, tough | High shrinkage; warpage needs tool compensation |
| PP | Trays, packaging, boxes, equipment liners | Chemical and fatigue resistance, lightweight | Strong memory; sag and warpage control decide the outcome |
| PVC | Trays, packaging, industrial enclosures, liners | Cost-effective, forms cleanly, self-extinguishing grades available | Upper service temperature limit; confirm grade approvals |
| PMMA | Clear covers, luminaires, display parts | Optical clarity and weatherability | More brittle than PC; radii matter |
| ASA | Outdoor equipment housings, automotive exterior parts | UV and weather stability | Fewer low-cost supply options than ABS |
The shortlist still assumes you can hit the forming window. Each resin has a sheet-temperature range where it stretches evenly instead of tearing or webbing, and that range shifts with heater output, sheet colour and tool temperature. If the service environment narrows you to one material, confirm early that its forming window fits your equipment — our guide to determining the right temperature for vacuum forming walks through that check.
How Do Service Conditions Narrow the Shortlist?
Service conditions are the fastest filter. Write down the maximum continuous temperature, the worst impact event, every chemical the part touches, whether it lives outdoors, and any flammability or clarity requirement. Two or three of those five answers usually cut the candidate list in half.
Heat is the least forgiving condition. A housing that sits above 70 °C in service needs a resin whose deflection temperature clears that number with margin, not one that merely approaches it on paper. ISO 75-2 defines the heat deflection temperature of a plastic under a specified flexural load, which is the figure that tells you where a formed panel starts losing stiffness rather than where the resin melts.1 As a working rule, keep continuous service temperature well below the measured deflection value of the formed part, because forming introduces orientation and residual stress that shift behaviour away from the raw sheet datasheet.
Impact comes next. Guards, cases and automotive interior parts that take hits point toward PC, PC/ABS or ABS; dunnage and liners that should dent rather than crack point toward HDPE. Outdoor exposure moves the list toward ASA and PMMA, or UV-stabilised grades, because standard ABS and PP chalk and fade within a few seasons. Chemical exposure favours HDPE and PP for trays and liners that see oils, detergents or fertilisers.
Enclosures add a compliance layer on top of mechanics. UL 94 classifies the flammability of plastic materials by how specimens burn and extinguish, and many electrical equipment covers and housings cannot be released until the material meets the required rating at the finished thickness, not merely within the grade family.2 Clarity requirements point to PC or PMMA, and total luminous transmittance is measured per ISO 13468, so ask for the value at your formed gauge rather than quoting a resin brochure.
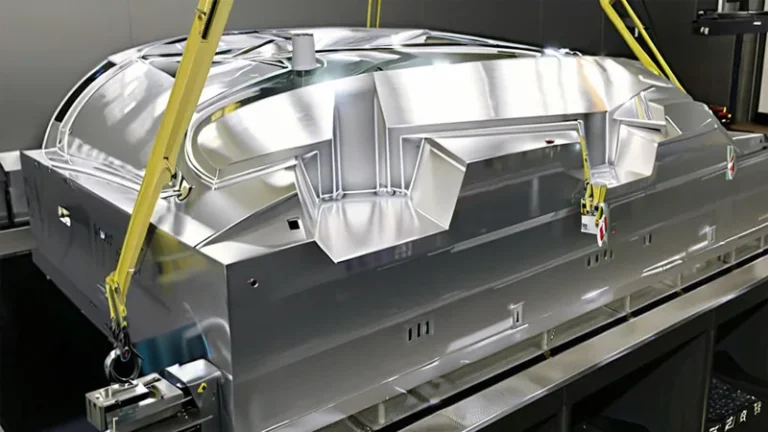
ZetarVac processes sheet from 0.5 to 15 mm and forms parts up to about 2,500 mm long on more than 20 vacuum forming machines. At selection time that range matters: the same geometry drawn in thin sheet and in heavy gauge can demand different resins, because sag, thinning and cooling behaviour all change with thickness.
How Do Gauge and Draw Depth Change Your Options?
Gauge and draw depth decide how much stretching the material must survive. Deep draws thin the corners first, and every resin has a limit past which corners whiten, thin out or tear. Shallow parts forgive almost anything; deep parts eliminate brittle and high-shrinkage resins fast.
A common screen is the draw ratio — formed depth divided by the narrowest side of the formed footprint.3 Many forming shops keep it at or below roughly 1:1 for uncomplicated male-tool parts and plan plug assist, webbing control or pressure forming beyond that. Treat these as conventional ranges, not laws: they shift with resin grade, sheet temperature and tool design, and our guide to determining the right draw depth for vacuum forming shows the fuller method.
Thickness changes the physics as much as the geometry. Above roughly 5 mm, sheet needs longer, more even heating on both sides, sags more under its own weight and demands longer cooling — all of which magnify the differences between resins. Warpage, the most common complaint in heavy gauge thermoforming, is largely a shrinkage-management problem, so a resin with low and predictable mould shrinkage is worth a premium on large flat panels.
Corner behaviour is material-specific. ABS thins gradually and predictably through a deep draw, which is one reason it dominates housings. HDPE and PP carry more memory and spring back after forming, so tools must compensate. PC delivers enormous strength but whitens around tight features when formed too cold — a temperature problem disguised as a material problem.

Which Properties Should You Verify Before Releasing a Sheet?
Data sheet values describe the resin. Formed-part values describe your part, and only the second set should release a material for production.
For structural housings and trays, tensile data is the baseline. ISO 527-2 specifies the tensile test method for plastics and is the standard behind the modulus and strength figures you compare between candidate sheets; ask for values measured at, or corrected to, your forming gauge rather than a different thickness.
Stiffness of large flat panels is a flexural question. ASTM D790 specifies the test method for flexural properties of plastics, and a coupon cut from a real formed panel is a far better predictor of oil-canning and creep under load than the resin brochure alone.
Then test on formed parts, not raw sheet. A coupon cut from a formed wall carries different molecular orientation than the supplied sheet, particularly on deep draws. Verify thickness distribution across the deepest corners, deflection behaviour near heat sources, impact on the formed surface, and dimensional stability after conditioning at room temperature. These four checks catch most mismatches between a shortlisted resin and the actual part.
"A first-article part that passes inspection proves the material choice is safe."False
A first article is formed from a single sheet lot under hand-tuned settings. Sheet lots vary in moisture, regrind content and molecular weight, so a part that passes today can warp in volume production when the next lot forms differently.
"Material sign-off should rest on trials across multiple sheet lots at production settings."True
Forming trials on two or three lots, dried and heated exactly as production will run, expose lot-to-lot drift before it reaches your customer. Lock the approved grade together with its heating profile, vacuum dwell and cooling regime.
What Does the Sheet Really Cost?
Compare cost per accepted, trimmed part — never sheet price per kilogram. Kilogram pricing ignores yield, trim ratio, cycle time and inspection fallout, and those four factors routinely reverse a ranking that looked obvious on a supplier price list.
Sheet consumption per part depends on the trim frame, and heavily drawn parts can waste half the sheet in the frame. Regrind policies change the picture again:4 trim that is reprocessed lowers material cost but shifts melt behaviour, and an inconsistent regrind percentage is a classic cause of lot-to-lot warpage in thermoforming. Cycle time belongs in the same calculation, because a resin that forms and cools faster produces more parts per shift. Add expected scrap from forming and trimming, and the material that looked 15 % cheaper can easily cost more per shipped part.
"The cheapest sheet per kilogram is the cheapest material for the project."False
Price per kilogram says nothing about yield, frame waste, cycle time or post-forming scrap. A resin that cools faster or rejects 4 % fewer parts usually beats a cheaper sheet that runs slower and fails more often at final inspection.
"Rank materials by cost per accepted part at production cycle settings."True
Build the comparison from sheet consumption per part, expected yield, trimming time and inspection fallout. That is the number volume buyers actually pay, and it is the only material ranking that survives contact with a production plan.
For parts where several resins all pass the technical screen, this costing step is usually what settles the debate, because the differences show up in the production plan rather than in the lab.
Prototyping, small batches and large batches are all supported, with reference monthly capacity of roughly 100,000–200,000 pieces across 45+ production lines. For selection, that means a candidate sheet can be qualified under genuine volume conditions instead of a softened laboratory trial.
How Do You Run a Material Trial That Predicts Production?
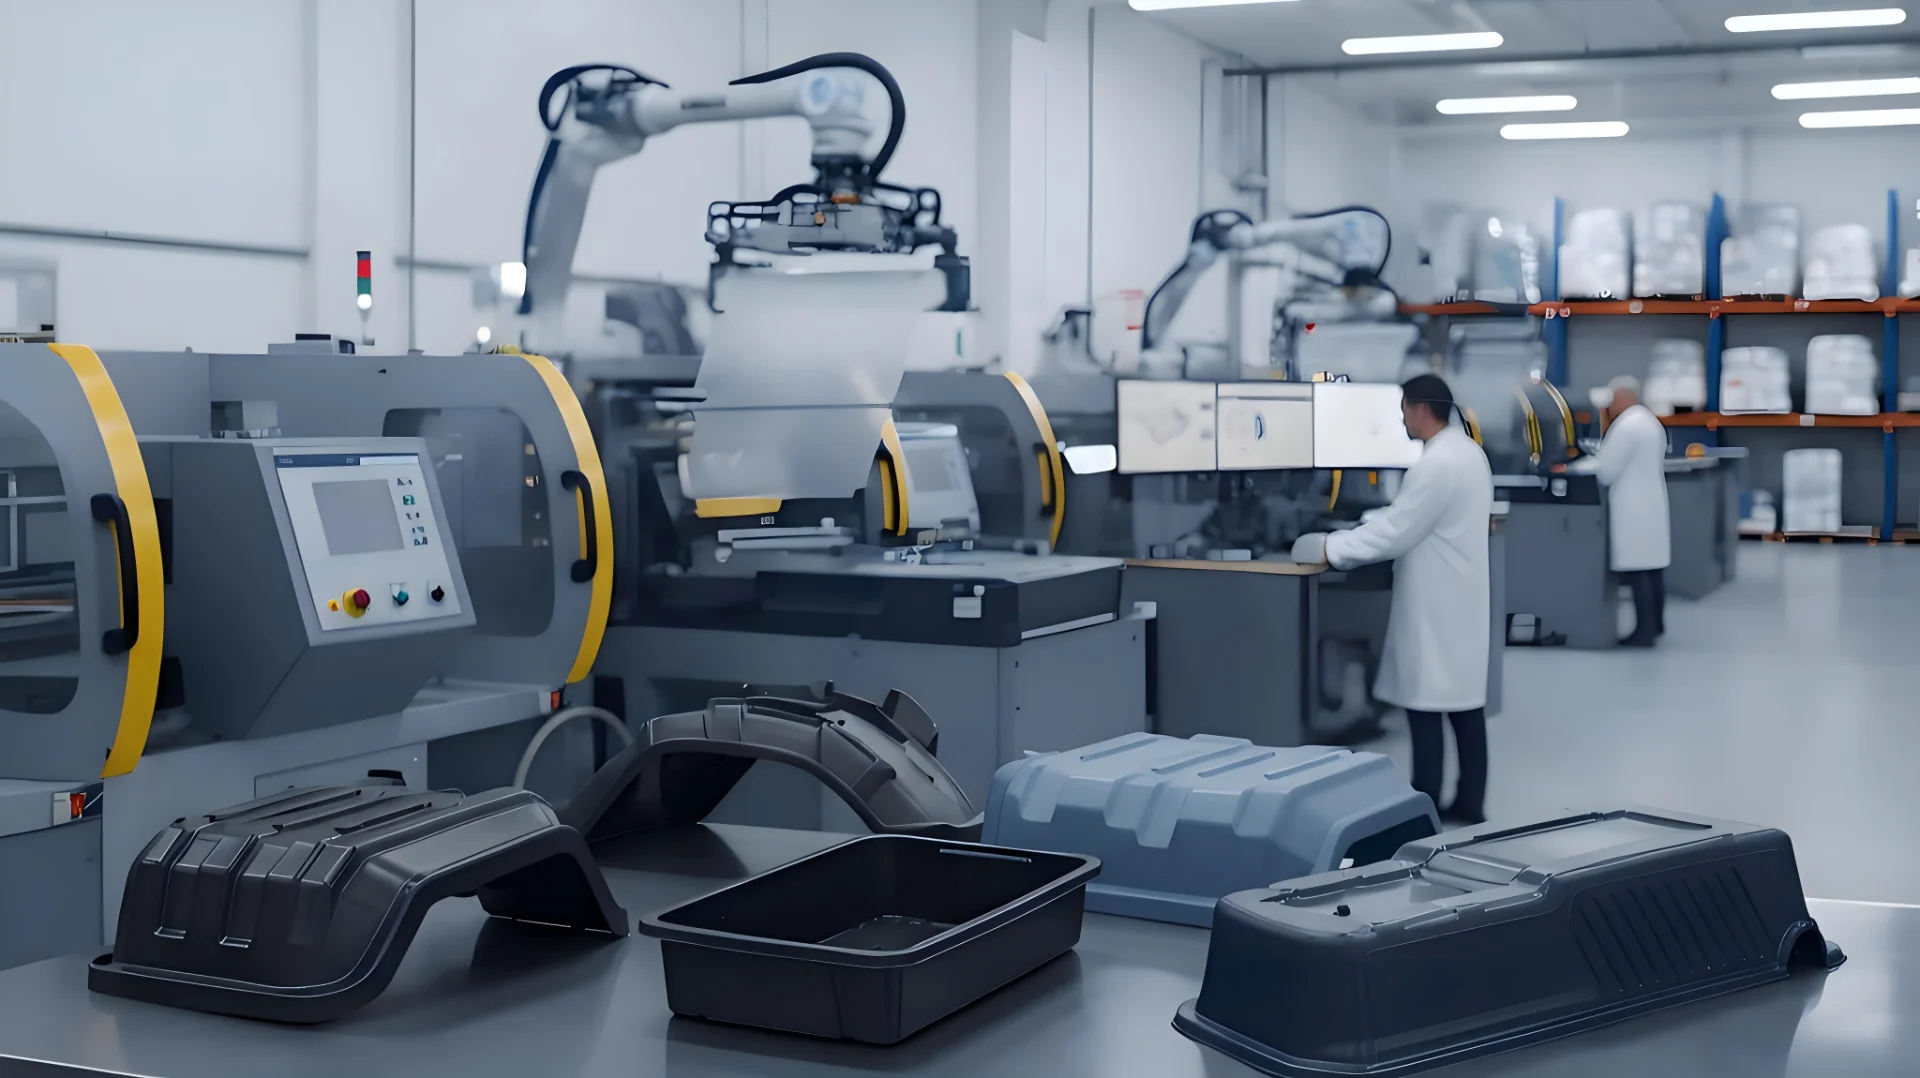
Run the trial at production settings, in the production gauge, with the production drying routine. A candidate sheet formed gently in ideal conditions tells you what the material can do; only production conditions tell you what your part will do.
Record what production will inherit: heater zone settings, sheet surface temperature at the moment of forming, vacuum dwell, cooling time, and post-form shrinkage measured after conditioning. Map wall thickness across the part, not just at one point, and keep the two or three settings that produced in-spec parts as the starting recipe for volume. The SPE Thermoforming Division publishes process papers and case studies worth reading before you design the trial matrix.
Trimming belongs in the trial too. Formed outline accuracy is only provable after trimming, and 5-axis CNC trimming that follows the forming tool will reveal springback and distortion that hand finishing hides. Surface finish decisions also interact with material choice — texture can hide flow lines on one resin and amplify them on another, which our guide to choosing the right finish for a vacuum formed part covers in detail.
"If the sheet forms without tearing, the material is validated."False
Absence of tearing clears only the first hurdle. Wall-thickness distribution, post-form shrinkage, warpage after conditioning and stability at service temperature all remain open, and they are where a poor material match surfaces weeks later.
"Validation means a thickness map, shrinkage check and dimensional report on formed parts."True
Measure thickness across the deepest draw, check post-form shrinkage over a defined conditioning period, and verify critical dimensions after full conditioning. A candidate that passes those checks at production settings is a material you can commit to.
A trial that documents those three outputs also becomes the reference for incoming sheet inspection later, which is how the selection work keeps paying off long after launch.
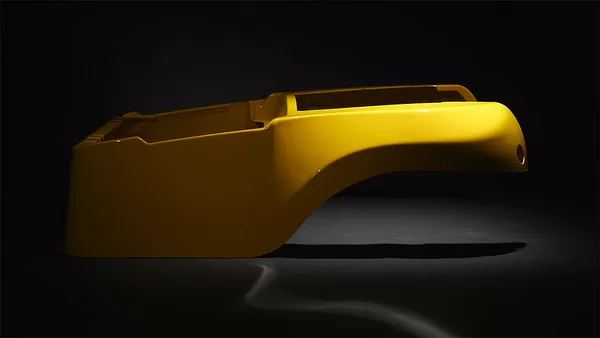
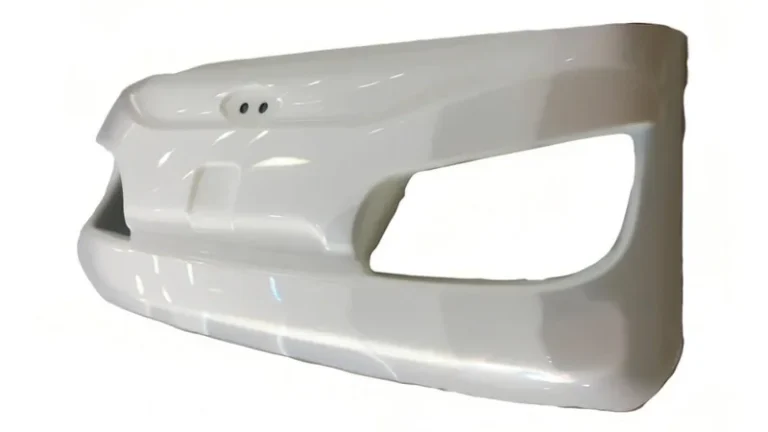
Recent formed programmes show the pattern in practice: an ABS seedling tray with custom cavity geometry for agriculture, a PC medical equipment housing with cut-outs, mounting holes and reinforcement, and a PMMA retail display cover where clarity drove the choice. Three resins, three different selection logics, one forming process.
FAQ
Which plastic is best for vacuum formed equipment housings?
ABS is the default for indoor housings: it forms over a wide window, finishes well and absorbs impact. Move to PC/ABS when impact or paintability matters, and to ASA outdoors. Any housing near a heat source needs its deflection temperature checked before the grade is chosen.
Is thicker sheet always better for heavy gauge parts?
No. Thicker sheet raises stiffness but also lengthens heating and cooling, increases sag and corner thinning, and amplifies the resin’s shrinkage behaviour. Choose the thinnest gauge that meets the stiffness and impact requirement, then confirm it with a flexural check on a formed panel.
Can I switch materials after the forming tool is finished?
Sometimes, but not freely. The tool was cut to compensate for a specific shrinkage rate and trimming behaviour, so a material swap changes dimensions and the trimmed outline. Small moves such as ABS to PC/ABS are usually manageable; crossing resin families needs a tool review first.
PC or acrylic for a clear formed cover?
Choose PC when the cover can be struck and must not crack; choose PMMA when optical clarity and weatherability outrank impact. PMMA forms with excellent transparency but is more brittle, so generous radii and a low-stress forming window matter.
How many sheets does a meaningful material trial need?
Plan on roughly three to five sheets per candidate — one for heater set-up and one to three for measurement at stable settings — ideally drawn from two different sheet lots. Fewer than that and you are qualifying a lot, not a material.
When the shortlist is down to two or three resins, it helps to see how each behaves across the whole process. Explore our vacuum forming overview to understand how sheet selection, tooling and trimming fit together, or learn how we approach material selection as a China-based vacuum forming manufacturer.
-
HDT: Heat deflection temperature — the temperature at which a plastic specimen deflects a specified amount under a defined flexural load, used to compare heat resistance between resins. ↩
-
V-0: A UL 94 flammability rating in which vertical specimens extinguish within ten seconds without igniting the cotton below, commonly required for electrical enclosures. ↩
-
Draw ratio: The ratio of a formed part’s depth to the narrowest side of its formed footprint; a quick screen for how hard the sheet is stretched. ↩
-
Regrind: Sheet trim and rejected parts reprocessed into new sheet; the regrind percentage changes melt behaviour and must stay consistent between lots. ↩